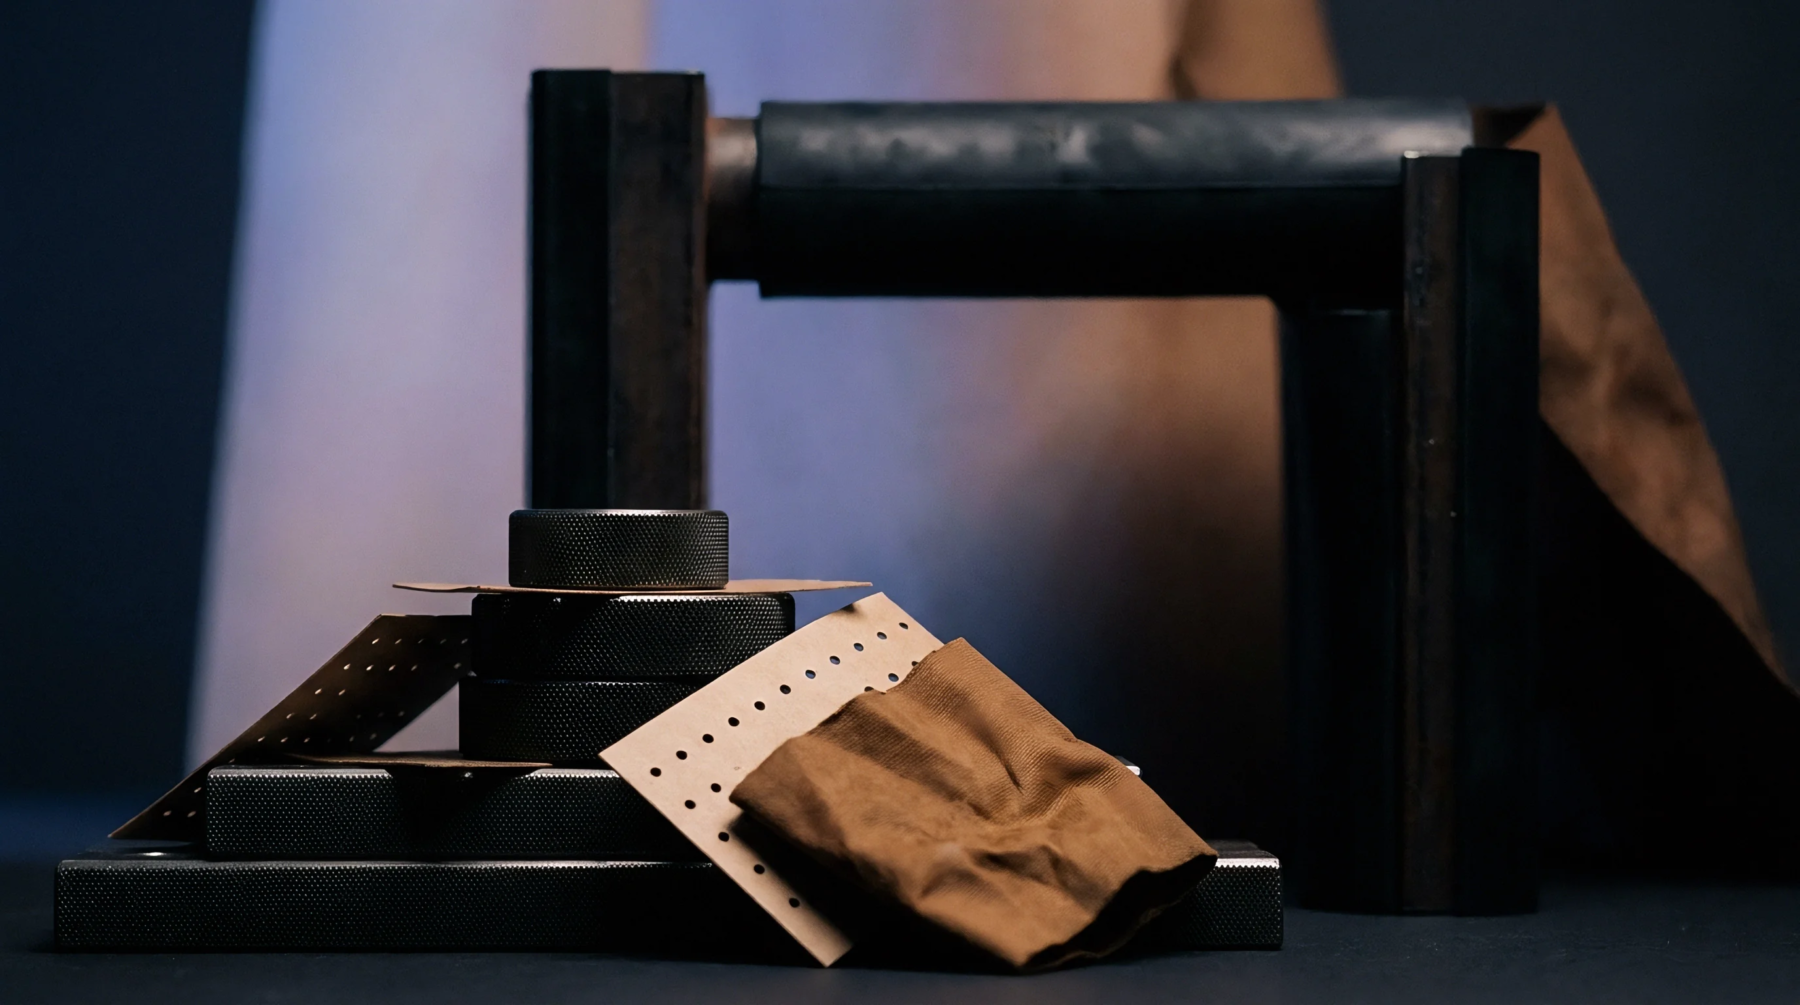
Fiber Compaction
Mechanical force application to substrate samples during moisture equilibrium testing ensures that air gaps within the test piece reach a minimum threshold density before measurement. High pressure sample compression controls the contact area between the sensor face and the internal structure of paper or polymer sheets. This procedure minimizes variance in dielectric response by removing microscopic surface voids.
Engineers utilize this technique to confirm that variations in instrument output result from material properties rather than contact inconsistencies or inconsistent surface topography. Variations in air content within a sheet create false signals in moisture content analysis. Applying a fixed load forces the internal fibers to conform to a uniform geometry.
Force Distribution
Measurement accuracy depends upon the uniformity of the pressure gradient across the sample surface during the test cycle. High pressure sample compression utilizes a hydraulic or pneumatic piston to maintain a constant load during the entire sensing window. The apparatus monitors the reaction force to ensure the material stays within the linear elastic region.
If the material exceeds this limit, the internal structure collapses or experiences permanent deformation. Consistent results depend on the calibration of the load cell against a standard block of known density. A stable environment prevents the sample from shifting under the applied load.
Maintaining a constant state of contact ensures that the dielectric probe captures data from a representative cross section of the substrate rather than superficial surface anomalies.
Operational Boundaries
Production quality systems limit the maximum force applied to prevent the crushing of porous structures like recycled fiber boards. High pressure sample compression relies on specific psi settings calibrated to the structural integrity of the individual grade. The process stops when the sensor determines that the displacement rate has reached a state of near zero velocity.
This equilibrium point defines the target density for the measurement cycle. Automated systems adjust the clamping force if the incoming stock shows thickness variations that exceed the established process tolerance. Achieving a uniform densified state allows for the detection of trace contaminants within the fiber matrix.
Excessive force creates false signals by damaging the internal bonding of the substrate. Proper control of the clamping force defines the reliability of the moisture measurement across the entire manufacturing run.