Laboratory Fiber Yield Measurement across Poly-Coated Packaging Grades for EcoModulation
Laboratory fiber yield determinations on poly-coated board demand dry-mass corrections and ash deductions to prevent punitive eco-modulation packaging surcharges.
Furnish
Extrusion-coated paperboard packs present an immediate mechanical problem at the hydrapulper. The virgin kraft backing disintegrates under shear while the bonded polyethylene film stays intact, trapping usable cellulose within unseparated flakes. Laboratory verification protocols establish the baseline recoverable fiber fraction under controlled disintegration conditions, dictating whether an extended producer responsibility declaration qualifies for fee discounts or triggers punitive fee surcharges.
National extended producer responsibility registries evaluate packaging recyclability through standardized laboratory repulpability determinations. The European Packaging and Packaging Waste Regulation codifies recyclability performance grades based on material efficiency thresholds. Packaging designs yielding below seventy percent recovered dry fiber by mass face statutory disqualification from recycling streams, entering disposal fee tiers that eliminate the margin on high-volume consumer goods.
Fiber recovery testing isolates the water-insoluble polymer barrier from the cellulose matrix. Test standards require disintegrating dry packaging swatches in neutral water, screening the resulting suspension through defined perforations, and determining the dry mass of both the recovered accepted fiber and the rejected plastics. An inaccurate moisture determination or incomplete fiber separation shifts the calculated yield past critical regulatory modulation cutoffs.
Under standard screening conditions, an uncorrected one percent deviation in pulp moisture balance alters calculated fiber yield by over two percentage points against dry furnish weight.
Poly-coated paperboard grades encompass bleached sulfate boards, unbleached kraft liners, and folding boxboards. Each substrate pairs a specific cellulose furnish with an extruded low-density polyethylene layer, occasionally supplemented by aluminum foil or EVOH oxygen barriers. The polymer weight, extrusion lamination temperature, and wet-strength resin chemistry govern the ease with which cellulose detaches from the poly layer during agitation.
Uncoated kraft pulp separates readily, whereas paperboard treated with polyamide-epichlorohydrin wet-strength resins resists water penetration and mechanical defibering. Mills formulating liquid packaging board deliberately engineer wet tensile strength into the cellulose web, preventing carton collapse during milk and beverage storage. That same performance characteristic impedes laboratory repulping, producing large reject fractions on standard screen plates unless prolonged chemical disintegration cycles intervene.
Testing laboratories encounter wide yield discrepancies between single-side poly-coated coffee cup stock and double-sided aseptic carton blanks. Single-coated boards expose an unprotected cellulose face to immediate hydration and swelling. Aseptic constructions encapsulate the fiber between an inner polyethylene skin and an outer poly-aluminum composite, restricting water access exclusively to the cut raw edges during pulping.
The standard laboratory determination balances the dry mass of the recovered fiber against the starting oven-dry weight of the total composite sample. When an overseas converter provides certificates stating fiber yield based solely on the paperboard fraction rather than the finished laminate mass, the resulting declaration fails statutory audit. The importer of record answers for that numerical inflation directly through fee reassessments and administrative fines.
Bench
Laboratory yield evaluations rely on standardized repulpability procedures designed to replicate industrial pulping and cleaning operations. The primary test methods governing European and North American fee determinations comprise the PTS method RH 021/97, the CEPI Harmonised Recyclability Test Method, and the TAPPI UM 213 disintegration protocol. Each method specifies precise mechanical energy inputs, pulp consistency, water temperature, and screening dimensions.
Mechanical Disintegration Parameters across Protocols
Disintegration protocols mandate exact rotational speeds and rotor geometries to apply controlled hydrodynamic shear to the test specimen. The standardized laboratory disintegrator operates at twenty-nine hundred to three thousand revolutions per minute with a propeller rotor inside a cylindrical vessel equipped with four internal baffles. Operating outside these agitation limits either leaves intact paperboard clusters or shatters polymer films into unfilterable micro-fragments.
Pulping consistency dictates the shear stress transferred to fiber-plastic interfaces. The CEPI protocol establishes disintegration at a dry furnish consistency of two and one-half percent using water at forty degrees Celsius for ten minutes, amounting to twenty-five thousand revolutions. PTS Category II testing for barrier-treated liquid packaging grades applies thirty thousand to forty thousand revolutions at four percent consistency to dislodge tenaciously bound virgin fibers from the plastic film.
Specimen preparation demands precision die-cutting into squares measuring twenty-five by twenty-five millimeters or fifty by fifty millimeters. Cut geometry influences the ratio of exposed raw edges to coated surface area. Micro-scale laboratory pulpers artificially overstate defibering rates if specimens are cut into tiny fragments, because exposed fiber perimeter accelerates edge-wicking and water ingress ahead of industrial realities.
| Standard Designation | Furnish Consistency | Bath Temperature | Mechanical Energy | Screen Slot Dimension | Primary Target Output |
|---|---|---|---|---|---|
| CEPI Harmonised Protocol Version 2 | 2.5 percent | 40 degrees Celsius | 25,000 rotor revolutions | 0.15 mm slotted screen | Paper and board for general packaging |
| PTS-RH 021/97 Category II | 4.0 percent | 40 degrees Celsius | 40,000 rotor revolutions | 0.15 mm slotted screen | Liquid packaging and poly-coated barrier board |
| TAPPI UM 213 (Modified Method) | 2.0 percent | 23 degrees Celsius | 15,000 rotor revolutions | 0.15 mm slotted or 1.0 mm round | Containerboard and folding carton repulpability |
| 4evergreen Recyclability Evaluation | 2.5 percent | 40 degrees Celsius | 25,000 rotor revolutions | 0.15 mm slotted screen | Standard and dedicated recycling mill feeds |
Screening Separation Mechanics
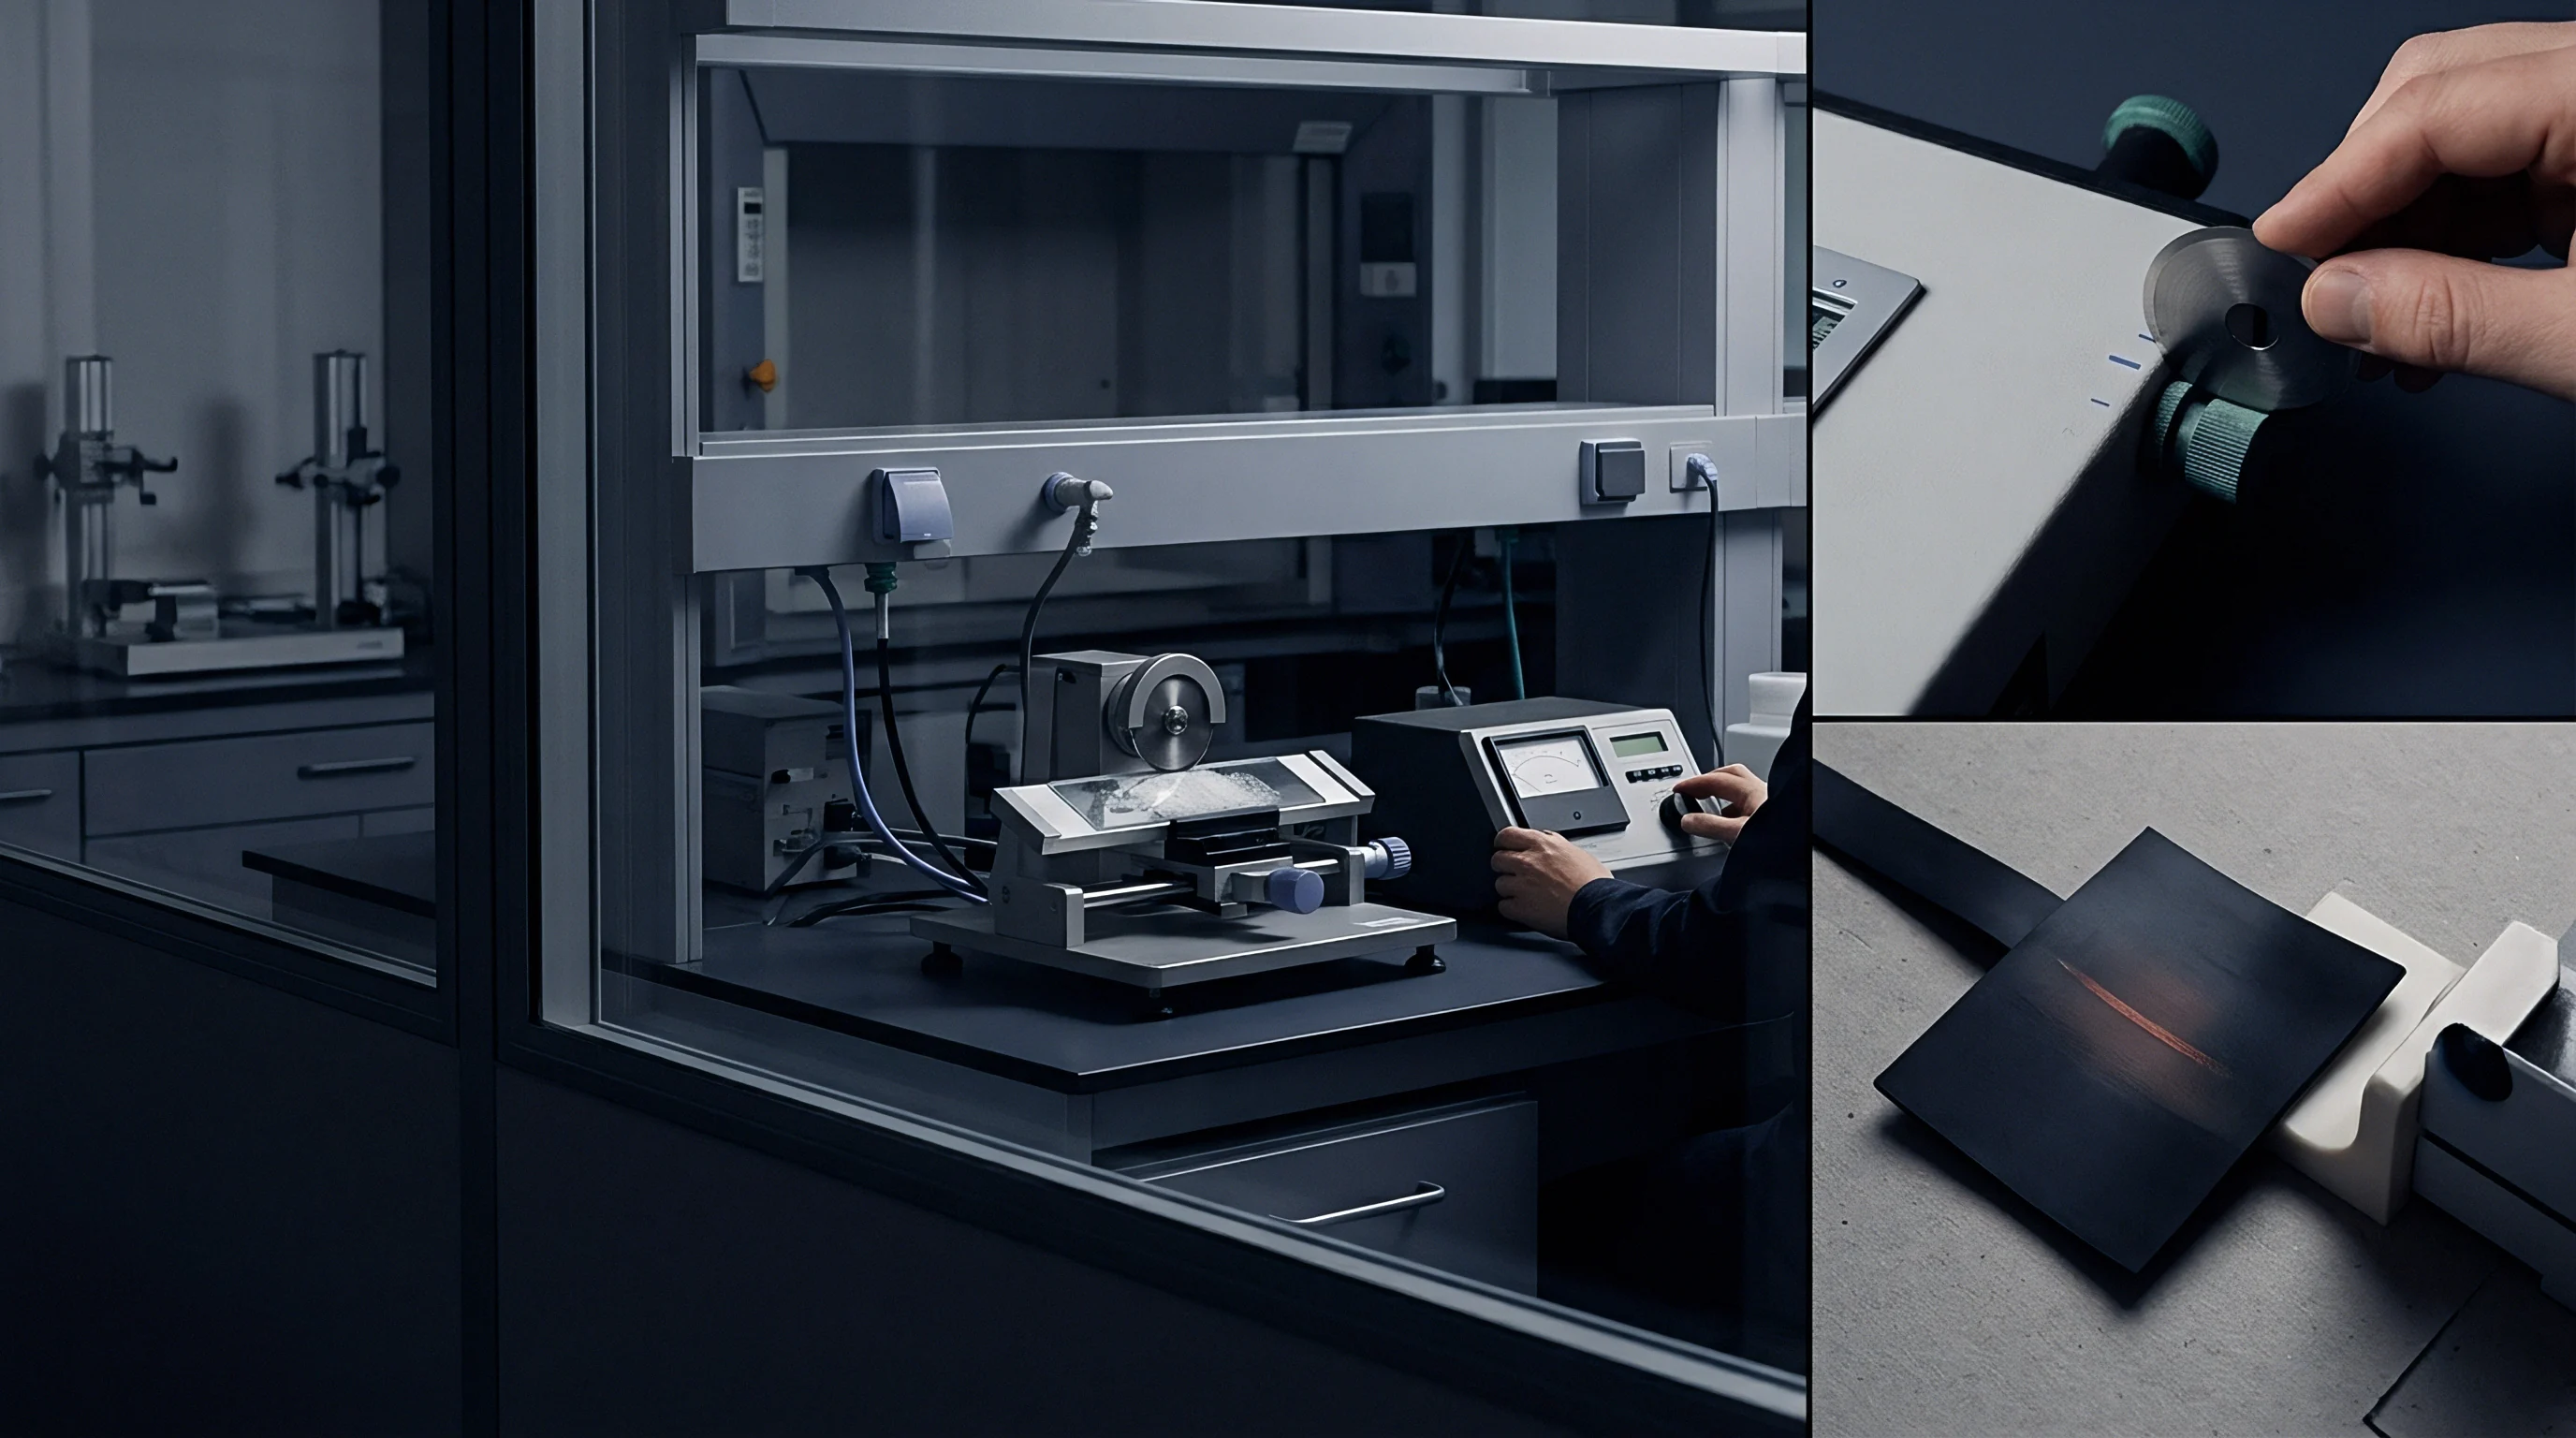
Separating released pulp from polymer reject relies on laboratory fractionation units, typically a Somerville screen or a Haindl classifier. The laboratory technician pumps the repulped slurry onto a flat screening plate containing calibrated parallel slots machined to an aperture of zero point one five millimeters. Water sprays wash the agitated pulp downward through the slots while retaining non-repulpable barrier fragments on the upper surface.
Slot dimensions dictate the boundary between acceptable cellulose fiber and reject debris. Unseparated board flakes, wet-strength fiber bundles, and polyethylene skins remain on top of the plate. Single individual fibers and small, thoroughly hydrated fiber bundles pass through the 0.15-millimeter slots into the accept reservoir.
Blinding of the screen slots by flexible polyethylene films introduces severe measurement error by preventing genuinely dispersed fibers from clearing the reject zone.
Washing duration and water pressure inside the Somerville apparatus must remain stable throughout the fractionation cycle. Standard procedures enforce a twenty-minute screening cycle with a regulated back-pressure water spray applying uniform upward pulsing. This mechanical pulsing dislodges pinned plastic films from the screen plate, ensuring free passage of dispersed fibers into the accept container without shredding the plastic.
Gravimetric Calculations and Yield Derivations
Quantifying fiber yield requires gravimetric mass balances calculated against bone-dry sample weights. Technicians dewater the accepted fiber suspension using a laboratory sheet former or a Buchner funnel lined with fast qualitative filter paper. The recovered pulp pad and the screen rejects are dried in a circulating ventilation oven at one hundred and five degrees Celsius until reaching constant weight.
Calculation equations derive total mass conservation across the fractionation sequence. The starting oven-dry mass of the composite swatch is designated as initial mass. The oven-dry mass of the material retained on the zero point one five millimeter screen forms the reject mass, comprising polymer films, aluminum backing, and non-defibered paper flakes.
The dried cake recovered from the filtered accept fraction forms the accept mass.
Total dry fiber yield expresses the accept mass as a percentage of the total original packaging swatch mass. This figure represents the practical yield entering mill recovery operations. In contrast, paperboard-base fiber yield normalizes the accept mass strictly against the theoretical cellulose content of the board, subtracting known polymer coat weights.
Eco-modulation registries mandate total composite yield rather than normalized base yield for statutory declarations.
Under EN 13430 annex provisions, an accept yield below the designated threshold automatically transfers product qualification from high-value sorting categories to mixed industrial reject streams.
Floc
Yield determinations frequently fail through incomplete fiber release rather than material absence. Polyethylene layers anchor themselves mechanically into the porous surface of the cellulose base during high-pressure melt extrusion. When pulping energy fails to break these mechanical interlocks, cellulose fibers remain glued to the discarded plastic flakes, leaving substantial pulp trapped within the reject stream.
Interfacial Adhesion and Fiber Entrapment
Corona treatment applied to paperboard surfaces before extrusion enhances polymer adhesion by generating oxidized polar sites on cellulose fibers. This chemical bond resists wetting and hydrodynamic shearing during neutral pulping. Laboratory yields drop dramatically when running boards with high corona treatment levels, because the interfacial shear strength exceeds the tensile strength of the individual wet cellulose fibers, causing fiber snapping instead of clean release.
Liquid packaging boards incorporate wet-strength additives, predominantly polyamidoamine-epichlorohydrin resins, to maintain carton rigidity when saturated. These resins form cross-linked, water-insoluble networks across cellulose fibers. During laboratory pulping at neutral pH and forty degrees Celsius, wet-strength resins prevent fibers from swelling, suppressing the hydraulic cleaving action that strips fiber networks cleanly off poly films.
The resulting rejects consist of composite sandwich flakes where paperboard layers remain shielded from water by plastic on one side and a cross-linked wet-strength resin barrier on the other. Laboratory technicians observe these thick, unseparated chips on the Somerville screen. Burning or dissolving the plastic reveals unreleased cellulose fibers that industrial mill pulpers operating without chemical digestion cannot recover.

Macro-Contaminant Formation and Screen Clogging
Poly-coated packaging grades generate specific operational contaminants known as macro-stickies and unpulped barrier flecks. Polyethylene films possess lower density than water, floating on the surface of laboratory flotation cells while simultaneously tackifying under warm disintegration conditions. When pulping temperatures exceed fifty degrees Celsius, low-density polyethylene approaches its softening phase, picking up free cellulose and sticking tenaciously to screen bars.
Pigmented, printed, and adhesive-laminated packaging structures introduce synthetic polymers that fragment into flexible ribbons. These films wrap around disintegrator impellers and obstruct Somerville screen slots. Screen blinding decreases the effective slot opening below zero point one five millimeters, generating artificial reject mass and yielding falsely pessimistic fiber recovery figures on compliant board stock.
Fine mineral fillers and sizing agents contribute to false yield calculations through mass migration. Calcium carbonate, clay, and titanium dioxide detach from the fiber web during mechanical shear, passing through the filter papers during accept dewatering. Unless the testing laboratory performs ash testing at five hundred and twenty-five degrees Celsius on both the starting sample and the final accept pads, lost inorganic fillers register falsely as destroyed or non-recoverable cellulose fiber.

Score
Statutory recycling systems translate laboratory fiber yield into fee structures through mathematical modulation scales. The calculated accept yield forms the gatekeeper metric. If a cup, tray, or carton sample fails the mandatory yield threshold under accredited bench conditions, the producer forfeits baseline packaging fees and faces malus surcharges designed to subsidize sorting and landfill disposal.
Modulation Bands and Regulatory Thresholds
European producer responsibility schemes assign packaging formats to performance tiers based on harmonized laboratory yields. Tiers reward highly repulpable packaging with fee reductions while imposing severe financial surcharges on refractory designs. The regulatory thresholds demand rigorous compliance testing to prove substrate cleanability.
- High recyclability packaging achieves a laboratory fiber yield equal to or exceeding eighty-five percent of total packaging dry mass under standard CEPI or PTS conditions with negligible unpulped flocs.
- Standard recyclability packaging registers laboratory fiber yields between seventy and eighty-four point nine percent, qualifying for ordinary municipal paper mill processing routes without commercial fee penalties.
- Refractory multi-material packaging generates fiber yields between fifty and sixty-nine point nine percent, incurring mandatory eco-modulation fee surcharges due to high reject processing costs at the mill.
- Non-recyclable packaging formats fall below the fifty percent net fiber recovery mark, facing absolute administrative exclusions from paper collection streams and automatic taxation under composite disposal rules.
The mechanical efficiency baseline set by the European Packaging and Packaging Waste Regulation mandates design-for-recycling criteria that establish minimum repulpability scores by 2030. Composite packaging failing to prove an eighty percent industrial fiber recovery rate under standard laboratory verification faces an operational ban across member states. Converters cannot rely on broad self-declarations when customs agents and market surveillance authorities demand certified test documentation.
Worked Yield Case on Double-Sided Liquid Packaging Board
Consider an imported double-sided low-density polyethylene coated aseptic board with a nominal specification of two hundred and eighty grams per square meter baseboard, laminated with twenty grams per square meter outer polyethylene, six grams per square meter aluminum foil, and twenty-four grams per square meter inner polyethylene. Total packaging weight measures three hundred and thirty grams per square meter, yielding an initial theoretical fiber fraction of eighty-four point eight percent.
A compliance officer submits thirty grams of cut board swatches to accredited disintegration following the CEPI Version 2 protocol at forty degrees Celsius and twenty-five thousand revolutions. The initial dry mass of the conditioning sample equals twenty-eight point zero five grams at seven percent raw sample moisture. During pulping, water-insoluble wet-strength resins within the virgin bleached kraft layers limit fiber liberation along the lamination interface.
Somerville fractionation over a zero point one five millimeter slotted plate yields an oven-dry screen reject mass of seven point nine zero grams, comprising fused polymer films, aluminum fragments, and four point two grams of unpulped fiber flakes adhering to the polymer skin. Filtration of the accept slurry yields nineteen point two zero grams of bone-dry recovered fiber cake. Ashing the accept pad at five hundred and twenty-five degrees Celsius reveals zero point four five grams of inorganic mineral pigments.
Calculations show an initial raw accept yield of sixty-eight point four percent against the starting sample dry mass. Deducting the mineral ash fraction produces a net organic cellulose yield of sixty-six point eight percent. Despite the baseboard containing nearly eighty-five percent virgin cellulose on the spec sheet, the packaging lands in the refractory multi-material bracket because twelve point six percent of the total sample mass remained locked in reject flocs, triggering a three hundred euro per tonne statutory fee surcharge.
Under French Citeo fee modulation criteria, falling below the seventy percent fiber recovery threshold converts a standard paper packaging contribution into a double-rate penalization tariff per gross retail unit.
Tariff
Statutory classifications and customs declarations translate laboratory test reports into financial liabilities at the physical port of entry. Customs documentation links material declarations directly to Harmonized System codes and national packaging registers. Discrepancies between certified laboratory repulpability scores and customs packaging descriptions precipitate border holds, retroactive duty reassessments, and environmental fraud audits.

Harmonized Tariff Classifications and Customs Exposure
Packaging buyers declare poly-coated materials under specific tariff subheadings based on material dominance and chemical composition. Poly-coated paperboard containing over ten percent non-cellulosic polymer by mass frequently falls under Chapter 4811 as paper and paperboard coated, impregnated, or covered with plastics. If an overseas supplier describes the item as standard uncoated paperboard under Chapter 4805 to circumvent plastics tracking, customs agents flag the cargo for laboratory chemical verification.
Port-side inspection authorities employ Fourier Transform Infrared Spectroscopy and solvent dissolution to identify barrier polymers and quantify plastic coat weights. When testing exposes an undocumented polyethylene layer, customs auditors invalidate the accompanying commercial invoices and inspect previous shipments within the statutory audit window. Misclassification of plastic composite packaging as pure paperboard incurs back-taxes, calculated anti-dumping duties, and statutory penalties tied to gross container values.
Chain-of-custody documentation under schemes such as FSC or PEFC covers fiber sourcing credentials rather than physical recyclability. An FSC Mix or PEFC Certified claim on a delivery note confirms responsible forestry management across the supply chain, but it provides zero legal defense against national packaging fees or plastic-to-paper ratio violations. Border inspection agencies reject sustainable forestry certificates as substitutes for certified laboratory fiber yield reports.

Who Carries the Cost of Yield Verification Failures?
Packaging supply contracts determine financial liability through indemnification language and delivery incoterms. Importers of record bear the primary statutory obligation toward customs and environmental enforcement bodies. When imported packaging tests below mandated fiber recovery cutoffs, the state levies regulatory fines and elevated disposal surcharges directly upon the domestic purchasing brand.
Standard purchase order terms must incorporate explicit laboratory compliance clauses requiring suppliers to deliver third-party repulpability test reports under ISO 17025 accreditation. The clause must define the specific protocol, target yield minimums, maximum unpulped flake limits, and an obligation for the mill to absorb statutory modulation surcharges if independent testing demonstrates a yield deficiency. Without these contractual instruments, the domestic packaging buyer retains full commercial exposure for the mill’s formulation failures.
A supplier certificate asserting generic repulpability without identifying the test standard, water temperature, screening aperture, and gravimetric ash deduction holds no legal standing before regulatory compliance auditors. If commercial testing identifies an unpulped reject fraction exceeding fifteen percent, the regulatory desk reclassifies the entire product line as refractory composite packaging. This classification remains on the company’s compliance record, requiring mandatory third-party verification testing on every consecutive packaging import batch.