Standard Fiber Recovery Testing for Single Polyethylene Coated Cartonboard
Standard testing requires disintegrating 4% stock at 40°C, separating films via 0.15mm slotted screens, and confirming >80% yield with macro-stickies below thresholds.
Standard testing requires disintegrating 4% stock at 40°C, separating films via 0.15mm slotted screens, and confirming >80% yield with macro-stickies below thresholds.
Aqueous dispersion coatings replace extruded polyolefins by trading higher drying energy for mono-material EPR fee rebates when repulpable under CEPI rules.
Verify multi-wall containerboard wet strength using ISO 5378 nitrogen digestion and CEPI repulping to guarantee under two percent screen rejects for customs.
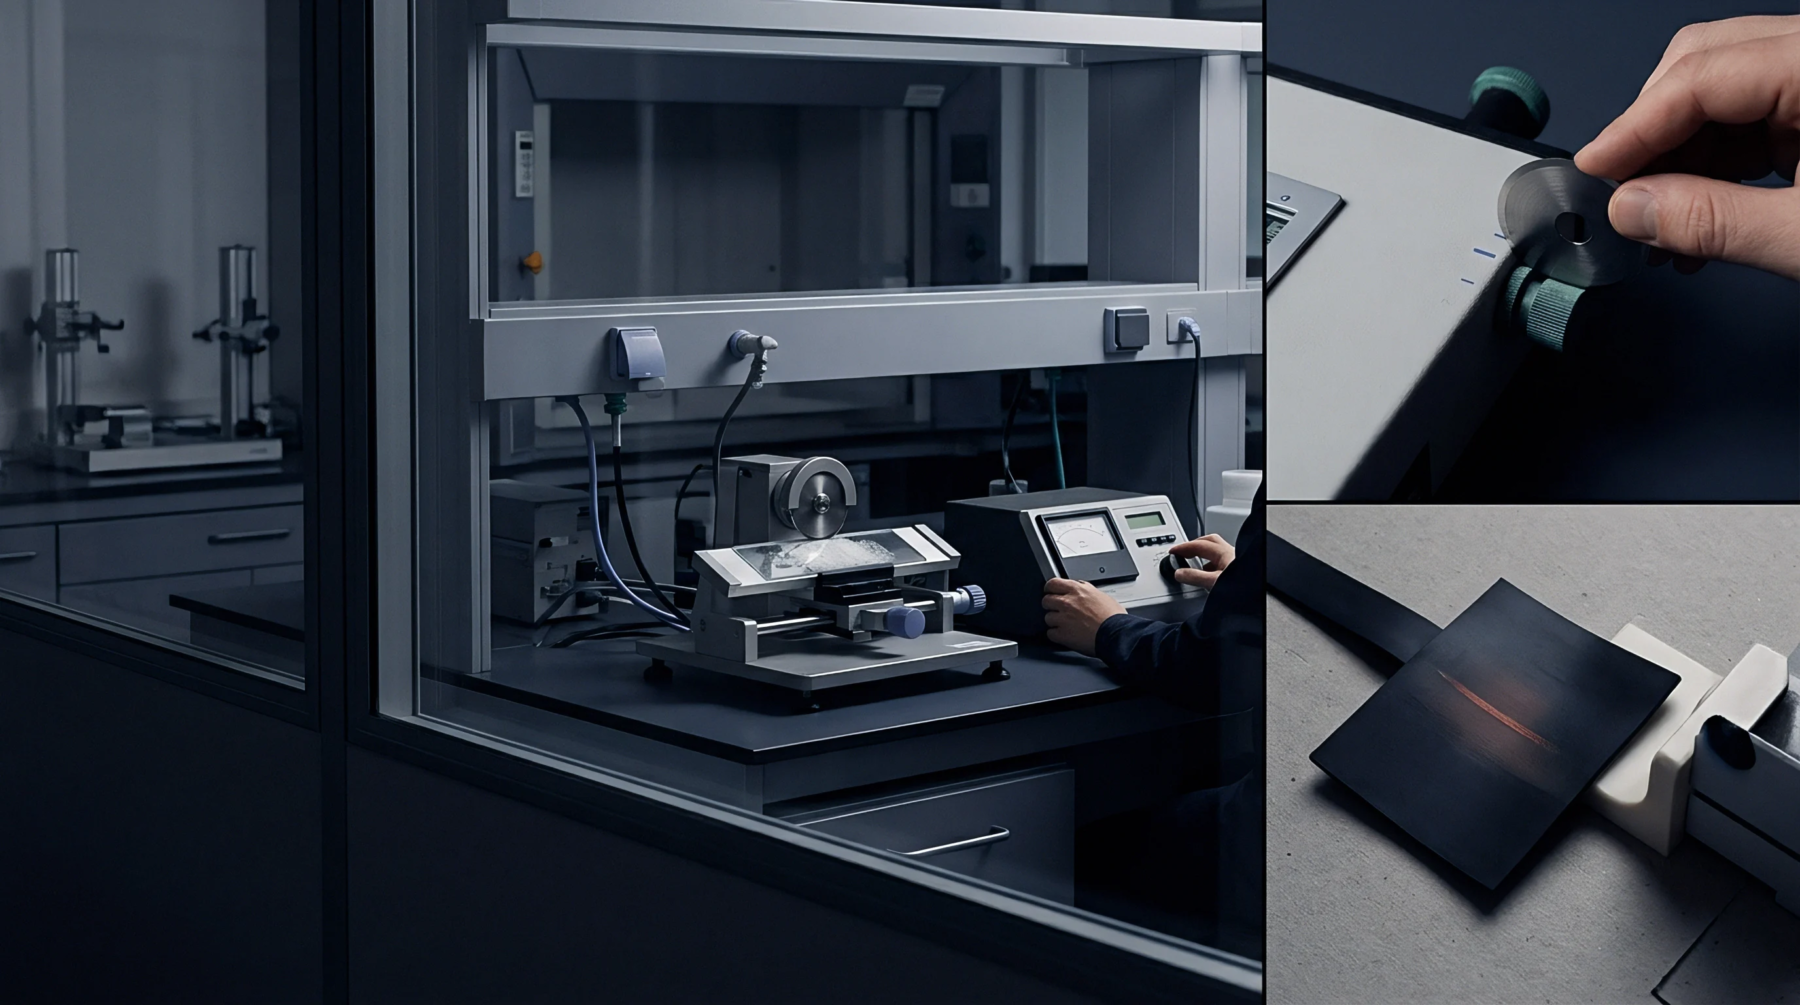
Laboratory screen slot dimensions dictate macro-stickie separation efficiency, requiring standardized 0.10 millimeter slot width calibration to calculate accurate area yields for packaging recyclability certification.
Aqueous dispersion barrier boards outperform extruded polyolefins by delivering over 95 percent wet end fiber yield and avoiding heavy EPR penalties.
Laboratory fiber yield metrics depend on screen slot geometry and ash corrections, directly determining EPR eco-modulation fee surcharges on packaging.
Optimizing CTMP core sulfonation and bulk yields lower grammage boxboard that maintains flexural rigidity while reducing landed carton cost.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.