Packaging Automation
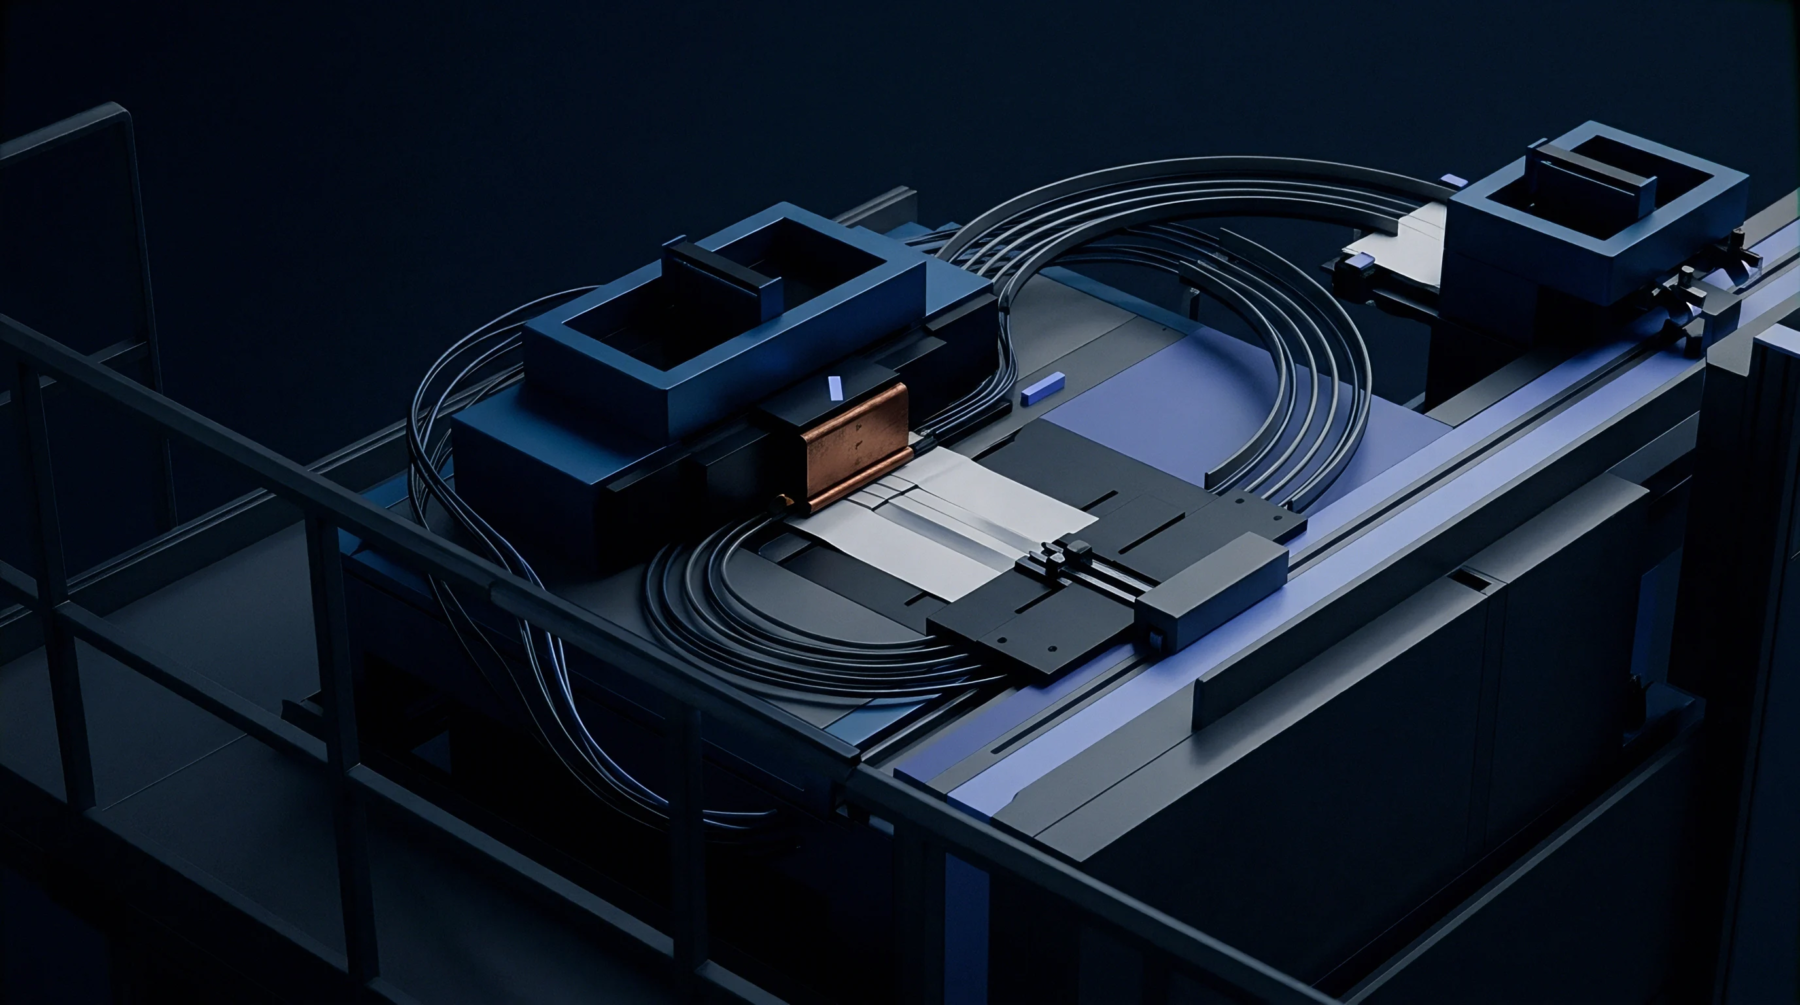
Continuous automated packaging systems convert flat rolled webs into filled, hermetically sealed pillow pouches or gusseted bags within a single downward progression. Mechanical assemblies execute vertical form fill seal cycles by pulling roll-fed material over a forming collar, sealing the overlapped edges longitudinally, and executing transverse heat seals across the bottom. Gravity directs metered food portions or consumer items through an internal fill pipe into the half-formed pouch while upper jaws clear product dust from seal zones.
Transverse seal bars compress, fuse, and sever the finished pack simultaneously, dropping completed units onto off-take conveyors below. Operational limits depend on the thermal sealing speed of the substrate, with mechanical timing dropping sharply for heavy paper-based barriers.
Sealing Sequence
Synchronized servos control pull belts, heat bars, and cut-off knives through programmable logic sequences. Intermittent systems halt the web during the dwell period of the sealing jaws, whereas continuous-motion variants move heat-sealing jaws alongside the traveling web to boost processing speeds. Sealing temperatures must not penetrate external decorative print coatings while ensuring internal sealant layers achieve complete melt flow.
Gaseous nitrogen flushing enters through the hollow filling mandrel, reducing residual oxygen within packages to prolong shelf life for sensitive dry food products. Machine vision photocells detect pre-printed register marks, adjusting web tension incrementally to keep brand graphics centred between transverse cut lines.
Substrate Requirements
Barrier laminates running through these vertical units require balanced mechanical and thermal properties. High static friction across back-seam mandrels introduces drag, stretching thin substrates and skewing cut-off points across consecutive bags. Coated paper solutions engineered to replace traditional multi-layer plastics demand wide seal-initiation windows, preventing seam pinholes around overlapping gussets.
Inadequate hot tack strength permits product drops to rupture freshly bonded bottom seals before polymers cool and set. Stiff corrugated papers resist the tight necking radii of standard forming shoulders, demanding modified collar profiles to eliminate vertical creasing and preserve protective barrier layers.