Surface Skin Shear Failure Analysis in Matte Polyolefin Packaging Films
Eliminate matte polyolefin skin shear failure by compatibilizing the skin-core interface and capping skin thickness below 1.5 micrometers to resist converting drag.
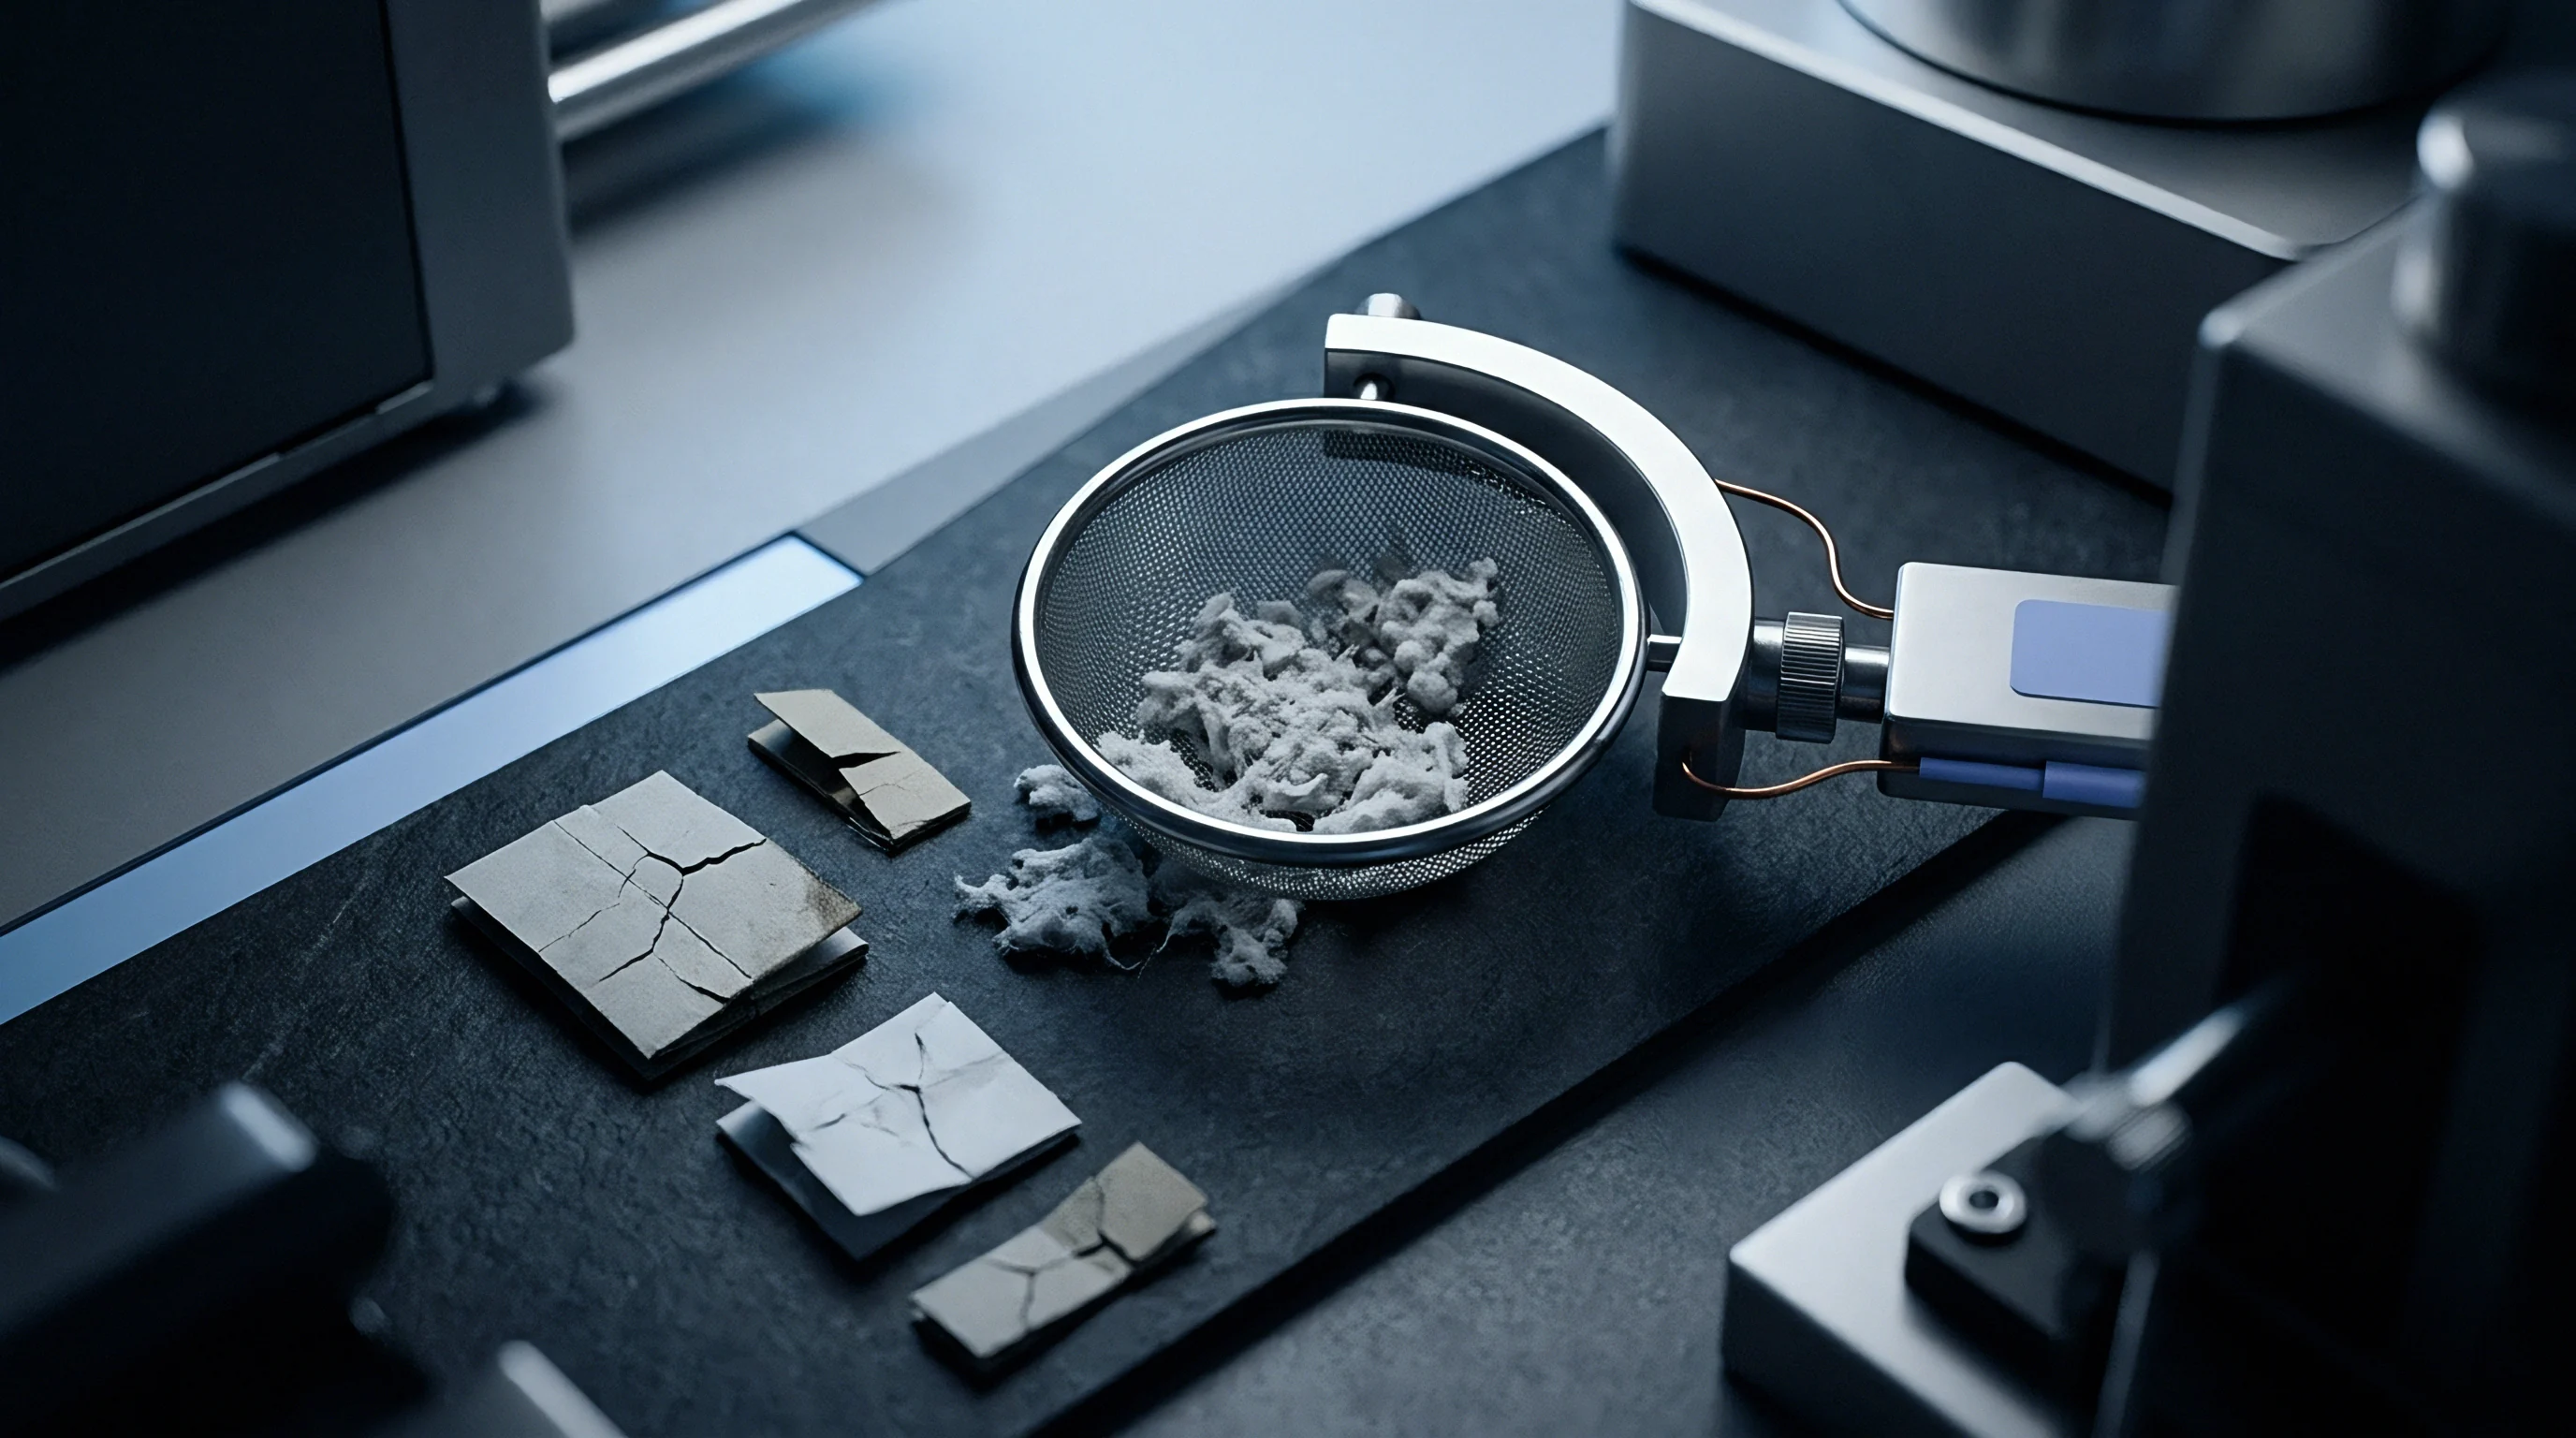
Fracture
Microscopic flakes detaching from a matte biaxially oriented polypropylene web during high-speed rewinding expose severe interfacial weakness across the coextruded structure. Coextruded packaging films achieve a low-gloss appearance by blending immiscible polymers within an external skin layer, typically combining a propylene homopolymer matrix with high-density polyethylene, polybutene-1, or crosslinked elastomeric particles. Differential thermal contraction and crystallization rates during film quenching produce a rough, light-scattering topography.
That same multi-phase morphology introduces mechanical stress concentrators throughout the skin plane.
Biaxial stretching during tenter-frame orientation magnifies microscopic boundaries between the incompatible polymer phases. Polyethylene domains draw at different rates than the surrounding polypropylene matrix, creating elliptical micro-voids around dispersed inclusions. When converting operations apply tension, winding nip pressure, or surface drag, these micro-voids act as fracture initiation sites.
Shear forces peel the skin. Rather than distributing mechanical loads through the film bulk, the applied shear localizes along the boundary between the matte skin and the core layer.
Cohesive failure takes place when the internal shear strength of the matte skin falls below the external friction applied by converting machinery. The core layer consists of highly crystalline, oriented homopolymer polypropylene designed for tensile stiffness and moisture barrier. The skin layer contains a high loading of incompatible resins and inorganic silica antiblock agents, reducing its cohesive shear resistance.
Microscopic voids initiate interfacial splits.
Agglomerated silica particles act as internal cutting edges within stretched polypropylene skins.
Delamination patterns fall into distinct morphological categories depending on resin distribution and orientation temperatures:
- Interfacial cavitation begins when incompatible polyethylene domains separate from the surrounding polypropylene matrix during transverse orientation, forming microscopic internal fissures.
- Transverse fibrillation occurs along orientation lines when high-speed slitting knives exert lateral cutting loads against cold web edges.
- Cohesive delamination shears the skin layer internally, leaving polymer remnants anchored to the underlying core while releasing loose surface debris.
- Abrasive micro-flaking releases powdery polymer dust onto guide rollers during high-tension web steering passes.
The boundary between the matte skin and the central core layer lacks molecular entanglement when coextrusion feedblocks operate with excessive viscosity mismatch. Viscosity ratios deviating significantly from parity push the lower-viscosity resin toward the die walls, creating non-uniform skin thicknesses. Thin regions concentrate shear loads during downstream processing, initiating localized peeling that propagates into broad interfacial delamination.
| Failure Mode | Primary Mechanism | Microscopic Appearance | Shear Threshold (N/mm) |
|---|---|---|---|
| Interface Cleavage | Core-skin adhesion breakdown | Smooth planar separation at boundary | 0.35 to 0.55 |
| Cohesive Matrix Tear | Weak skin layer cohesive strength | Fibrillated polymer remnants and rough tearing | 0.60 to 0.85 |
| Particle Debonding | Silica additive detachment | Spherical cavities containing loose particulates | 0.40 to 0.65 |
| Orientation Splitting | Excessive transverse draw ratio | Linear parallel fissures along orientation axes | 0.50 to 0.75 |
Extrusion resin suppliers routinely attribute the white powder accumulating on nip rolls to normal matting agent shedding rather than a systemic failure of core-skin compatibilization.
Peel
Tensile testing clamps mounted on a universal mechanical tester reveal whether surface separation stems from adhesive bonds or internal polymer detachment. Quantitative measurement of skin adhesion isolates mechanical resistance under controlled separation angles. ASTM F904 establishes the standard test method for comparing bond strength of flexible laminates, yet interpreting matte film traces demands microscopic inspection of the peeled specimen.
Tensile pull isolates bond strength.
Does Interfacial Cavitation Indicate Incompatible Resins?
Separation along the core-skin boundary produces an irregular, saw-toothed force curve during ninety-degree peel testing. Standard adhesive failures yield smooth plateau profiles reflecting uniform adhesive elongation. When a matte skin layer shears internally, force curves display rapid oscillations between crack initiation and arrest points.
Adhesive failure creates scrap.
A peel value below 1.2 N/15mm under ASTM F904 at 250 mm/min signals skin separation rather than adhesive bond failure.
Differentiating adhesive failure from skin shear failure requires identifying the physical location of the separation plane:
- Surface cleaning strips loose surface dust from the test specimen using dry compressed nitrogen.
- Cross-hatch scribing cuts through the skin layer into the core using a multi-blade cutter spaced at one-millimeter intervals.
- Pressure-sensitive taping applies calibrated roll pressure across the scribed lattice using standard cellophane tape.
- High-rate stripping pulls the tape at a ninety-degree angle within a precise half-second duration.
- Microscopic inspection categorizes detached debris by measuring the exposed core surface under polarized light.
Scanning electron microscopy coupled with energy dispersive X-ray spectroscopy confirms whether the detached layer contains silica additives specific to the matte formulation. The presence of silicon peaks on both the peeled tape and the remaining film core verifies cohesive failure inside the skin layer. Absence of skin resin on the core confirms true interfacial delamination.
| Standard Designation | Test Parameters | Measured Metric | Failure Indicator |
|---|---|---|---|
| ASTM F904 | 180-degree peel, 250 mm/min | Bond strength in N/15mm | Peel force below 1.2 N/15mm with film tearing |
| ISO 2409 | 6-blade cross-cut, 1 mm spacing | Flaking grade 0 to 5 | Classification exceeding grade 1 |
| ASTM D3359 Method B | Lattice pattern, pressure tape snap | Area percentage removed | Lattice detachment exceeding five percent |
| DIN 53375 | Sled friction, 100 g normal load | Dynamic coefficient of friction | Friction coefficient spikes during run duration |
| Test specimens conditioned at 23 degrees Celsius and 50 percent relative humidity under ISO 187 specifications. | |||
Purchase specifications referencing ASTM D3359 method B require zero flaking along lattice cuts, converting dispute resolutions from subjective visual arguments into definitive rejection thresholds.
Drag
Frictional resistance against polished chrome transport rolls and forming collars imposes severe lateral loads on running web faces. When packaging machinery accelerates to standard manufacturing speeds, film webs contact stationary metal formers, turning bars, and sealing jaws. Matte films exhibit complex frictional behavior because their microscopic surface peaks generate localized interlock with metal tooling.
Frictional heat accelerates polymer tearing.
Do Forming Collar Angles Exceed Interfacial Shear?
Vertical form-fill-seal packaging equipment pulls flat film webs over three-dimensional forming collars to construct tube structures. The web encounters acute wrap angles where normal forces concentrate along narrow geometric radii. Extrusion nips induce heavy shear.
Converting lines operating at line velocities above 200 meters per minute generate substantial interface temperatures through continuous frictional contact.
Heating softens the low-density polyolefin phases dispersed within the matte skin layer. As local temperatures approach the softening point of ethylene-propylene copolymers or polyethylene additives (typically 95 to 115 degrees Celsius), the shear modulus of the skin drops precipitously. The oriented polypropylene core maintains structural stiffness up to 160 degrees Celsius, creating an extreme mechanical shear gradient across the interface.
Roll pressures compress the web.
A typical high-speed flow-wrapper running a 30-micrometer matte film web provides a clear operational calculation. Consider an unwind tension set at 40 N per meter of web width, passing over a forming collar radius of 50 millimeters with a wrap angle of 1.2 radians. The kinetic coefficient of friction for an unmodified matte skin against chrome-plated steel climbs from 0.25 at ambient temperature to 0.55 at 90 degrees Celsius under running friction.
The normal force generated across the collar radius creates localized shear stresses exceeding 0.90 N/mm along the outer skin plane. When the core-skin interfacial bond strength equals only 0.65 N/mm, the skin tears away from the web structure, depositing white polymeric dust directly across the former nose.
Higher differential speeds across unwinding rollers accelerate delamination along the oriented transverse direction.
Slitting stations introduce further mechanical damage through blade-induced shear. Razor slitting applies high lateral pressure against unsupported web spans, whereas shear slitting utilizes overlapping rotary knives. Dull rotary blades compress the skin layer prior to cutting, initiating microscopic delamination cracks that propagate into the finished reel edges.
Surface dust clogs print plates. Delamination halts line operations.
| Processing Stage | Dominant Stress Mode | Critical Machine Variable | Delamination Limit |
|---|---|---|---|
| Rotary Slitting | Transverse shear compression | Knife overlap and blade sharpness | Blade side force exceeding 15 N |
| Forming Collar Pull | Dynamic sliding friction | Collar wrap angle and surface polish | Friction coefficient exceeding 0.40 |
| Nip Lamination | Hydrodynamic adhesive pressure | Nip durometer and cylinder loading | Nip pressure exceeding 4.5 bar |
| Pouch Heat Sealing | Thermal shear displacement | Jaw clamp pressure and dwell time | Interface temperature exceeding 110 C |
Uncontrolled surface shear at the packaging line generates abrasive polymer dust that fouls heat-seal bars, leading to leaker packages, contaminated sealing faces, and unscheduled line shutdowns.
Recycle
Mono-material polypropylene waste streams penalize blends that introduce incompatible polymer contamination into mechanical reprocessing systems. European circularity assessment protocols, including CEFLEX design guidelines and RecyClass evaluation standards, classify flexible packaging structures based on polymer purity. Matte films achieved through heavy loadings of immiscible polyethylene in the skin layer complicate mechanical reprocessing streams.
Specification clauses invoking ISO 2409 cross-hatch testing reject rolls displaying flaking greater than classification grade one.
Reprocessing facilities grind sorted post-consumer flexible films into flakes before melt extrusion and pelletization. During extrusion remelting, non-compatibilized polyethylene domains suspended in polypropylene matrices form gel defects and hazing within secondary compounds. Incompatible resins reduce melt strength.
Contamination triggers sorting rejection.
Circularity criteria define allowable thresholds for non-polypropylene additions in flexible packaging:
- Resin compatibility threshold limits incompatible polyethylene fractions to less than five percent of total package mass to retain mono-material classification.
- Filler loading limitation holds inorganic matting agents below three percent to prevent melt-flow disruption and filter clogging during mechanical pelletizing passes.
- Wash-off adhesive verification confirms that laminating adhesives release cleanly during hot caustic wash stages without tearing the polyolefin skin.
- Modulated fee tiering assesses whether the matte construction qualifies for reduced Extended Producer Responsibility rates or attracts economic penalties.
Extended Producer Responsibility schemes assign fee surcharges to packaging structures incorporating immiscible blends lacking chemical compatibilizers. These surcharges directly impact the landed unit cost of commercial packaging films.
Thinner skin layers maintain mechanical integrity under converting tension while preserving sorting acceptance in mono-olefin reclamation streams.
Recipe
Extrusion formulations determine interfacial tenacity through resin melt index ratios, grafting chemistry, and chill roll quenching dynamics. Balancing low surface gloss with mechanical shear resistance requires careful polymer architecture selection across every layer of the coextruded structure. Random copolymer polypropylene skin bases blended with maleic anhydride grafted polypropylene compatibilizers provide chemical bridges between core and skin polymers.
Grafted polymers bridge polymer phases.
Controlling crystallization speed during chill roll contact suppresses excessive domain growth in dispersed matting phases. Rapid quenching traps incompatible components in sub-micron morphologies, preventing large agglomerates that trigger void formation during tenter stretching. Chilled rolls quench the melt.
Thermal history governs crystal formation.
Skin layer thickness control represents another operational parameter. Skin thicknesses exceeding 2.5 micrometers generate elevated internal leverage during shear loading, facilitating cohesive tearing. Reducing skin thickness to between 1.0 and 1.5 micrometers limits the physical volume of weak material while maintaining sufficient surface roughness for light scattering.
Consider the production economics for a 20-tonne production run of 25-micrometer matte biaxially oriented polypropylene film. Standard commodity matte formulations utilize an uncompatibilized core-skin structure with 2.5-micrometer skin thickness, costing 1,850 euros per tonne in raw materials. An engineered formulation incorporating three percent maleic anhydride grafted polypropylene compatibilizer and an optimized 1.2-micrometer skin thickness raises raw material costs to 1,940 euros per tonne, adding 1,800 euros to total material expenditure.
Sourcing the compatibilized grade prevents line scrap: converting line trials show that uncompatibilized webs suffer an average 4.2 percent slitting and packaging reject rate from surface flaking and delamination, generating 1,554 euros in direct film waste plus approximately 3,200 euros in machine downtime costs. The compatibilized formulation saves 2,954 euros across the production lot.
Whether sub-micron core-skin tie layers can completely eliminate shear delamination without destroying the scattering haze required for premium matte packaging remains an unsettled technical challenge.