Standard Bench Viscometry for Aqueous Paper Coatings
Bench viscometry qualifies low-shear slurry pumping and leveling, requiring tight thermal control and correct spindle torque to prevent coater runnability failure.
Spindle
Brookfield rotational viscometry defines the standard baseline for slurry acceptance across mill receiving docks and coating preparation kitchens. Under TAPPI T 666 om-18 and ASTM D2196 Method A, testing technicians determine the apparent viscosity of aqueous paper coatings by measuring the torque resistance exerted on a driven element immersed in the fluid. The reading reflects fluid drag under low shear rates between one and fifty reciprocal seconds.
Low-shear behavior governs how an aqueous slip pumps through delivery pipework, flows across storage tanks, screens through vibrating meshes, and levels out across the base sheet after application. A formulation showing low resistance on the bench moves freely through supply loops. Conversely, an excessively viscous slip blocks delivery screens and creates uneven distribution across the web.
Low torque readings invite error. Technicians choose specific geometries from the RV series based on expected solids fraction and pigment loading. RV-1 through RV-3 handle thin pre-coat slurries and sizing formulations with apparent viscosities below two thousand millipascal-seconds.
Heavier topcoat formulations containing ground calcium carbonate, fine kaolin clay, and high latex ratios demand RV-4 or RV-5 elements to generate sufficient spring deflection. Running an undersized element in a heavy slip causes excessive fluid turbulence around the edges. Running an oversized element in a dense slurry stresses the internal sensor spring past its linear range.
Rotational Geometry on the Test Floor
Brookfield dial and digital instruments establish the primary baseline for inbound paper coating slips. When technicians lower the drive head into a testing beaker, centering the rotating shaft inside the fluid volume prevents wall effects from distorting the shear field. Standard RV guard legs shield the shaft against mechanical interference while setting a fixed hydrodynamic boundary.
Removing the guard leg alters the effective volume of the sample, which lowers the recorded drag value by five to twelve percent on the same coating batch. Testing laboratories that discard the guard leg produce numbers that cannot be verified across different testing sites.
- Fill a clean six-hundred-milliliter low-form glass beaker with five hundred milliliters of thoroughly blended coating slip.
- Immerse the temperature probe directly into the sample fluid while securing the beaker inside a thermostatic water circulation jacket.
- Inspect the drive element for dried pigment buildup, shaft runout, or surface scratches before attaching it to the instrument arbor.
- Thread the chosen test element onto the lower coupling using a counter-torque grip to protect the internal jewel pivot bearing.
- Lower the drive housing until the fluid meniscus aligns exactly with the fluid level groove etched on the rotating shaft.
- Select one hundred revolutions per minute on the motor drive controller to standardize low-shear flow rates.
- Engage the drive motor and allow the element to rotate continuously for exactly sixty seconds prior to recording the indicator dial or digital display value.
Viscosity numbers govern coater speed. Slurries exhibit complex non-Newtonian flow behavior where apparent resistance changes alongside the rotational rate. Technicians routinely record drag across four consecutive speeds: ten, twenty, fifty, and one hundred revolutions per minute.
Calculating the ratio of apparent viscosity at ten revolutions per minute over the reading at one hundred revolutions per minute yields the thixotropic index. A ratio between 2.5 and 4.0 indicates balanced leveling potential for blade and rod coating applications. Slips falling below 2.0 exhibit Newtonian tendencies that cause immediate color penetration into the sheet pores.
Formulations exceeding 4.5 level sluggishly, leaving blade lines, film split ridges, and uneven coat weight profiles across the finished paper surface.
Agitation speed during bench dilution changes measured apparent viscosity by breaking down the polymer network before thermal equilibrium arrives.
Thermal Equilibration in Jacketed Vessels
Temperature shifts alter fluid drag. Standard laboratory reporting requires a strict fluid target of 25.0 degrees Celsius, held within a narrow margin of plus or minus 0.2 degrees Celsius during agitation. Aqueous paper coatings incorporate water-soluble hydrocolloids including carboxymethyl cellulose, hydroxyethyl cellulose, and modified starches that expand or contract in response to thermal changes.
A temperature rise of three degrees Celsius drops the apparent viscosity of a sixty-four percent solids clay-carbonate slip by up to fifteen percent. Mill personnel checking tankers on outdoor offloading pads frequently measure slurry temperatures between 35 and 45 degrees Celsius directly after mechanical milling. Comparing hot tanker slurries against cooled laboratory reference samples produces false non-conformance disputes.
Mineral slips settle during transit. Jacketed circulation beakers connected to constant-temperature baths prevent thermal gradients across the measurement cup. Insulating the test station avoids room draft interference during winter testing cycles.
Coating slip stored in unheated drum stores forms dense, cold layers near the container bottom that resist pump movement. Technicians condition receiving samples inside closed water baths for at least twenty minutes prior to shaft immersion. Rapid heating with open immersion coils induces localized binder agglomeration and false grit generation.
Slurry consistency follows thermal control without exception.
Torque
Spring deflection inside the viscometer head translates fluid drag into a visible dial angle or digital register. Dial models utilize a calibrated beryllium-copper spring that twists proportionally under the hydrodynamic resistance generated by the immersed shaft. The standard RV spring mechanism generates full-scale deflection at 7,187 dyne-centimeters of torque.
The lighter LV mechanism reaches full scale at 673.7 dyne-centimeters, suited for clear sizing starch solutions and low-solids barrier emulsions. Operating either instrument below ten percent of full spring range magnifies mechanical pivot friction and meniscus resistance into large percentage errors. Operating above ninety percent approaches the mechanical stops of the spring assembly, risking plastic deformation of the sensing wire.
Low torque readings invite error. Dial indicators displaying readings below ten scale divisions deliver unreliable measurements. Changing the rotational speed or stepping up to a larger element shifts the registered torque into the optimal working window between twenty and eighty percent of full instrument scale.
Digital models calculate apparent viscosity automatically through embedded firmware algorithms that multiply recorded torque by element geometry factors. The operator records the instantaneous torque percentage alongside the calculated millipascal-second value to confirm valid instrument loading on every test run.
| Spindle Number | Viscosity Range (mPa·s) | Target Coating Grade | Typical Solids Range (%) |
|---|---|---|---|
| RV-1 | 10 to 100 | Surface sizing, barrier emulsions | 12 to 28 |
| RV-2 | 40 to 400 | Pre-coat slips, low-solids starch sizing | 35 to 48 |
| RV-3 | 100 to 1,000 | Mid-weight blade coatings, board base coats | 50 to 60 |
| RV-4 | 200 to 2,000 | High-solids topcoats, offset printing grades | 60 to 66 |
| RV-5 | 400 to 4,000 | High-solids gravure coatings, barrier slips | 64 to 68 |
| RV-6 | 1,000 to 10,000 | Specialty packaging barriers, high-viscosity pastes | 67 to 72 |
Spring Deflection and Sensor Boundaries
Accurate Brookfield dial records occupy a defined zone between ten and ninety percent of full spring tension. Calibration verification routines utilize certified silicone viscosity reference standards traceable to national metrology institutes. Silicone standards exhibit pure Newtonian behavior, maintaining identical apparent viscosity across diverse rotational speeds.
Mineral coating slips depart sharply from Newtonian behavior because pigment platelets and polymer chains realign under continuous shear. When silicone standards verify spring linearity within two percent of stated values, deviations recorded during slurry testing originate from fluid microstructure rather than mechanical sensor drift.
Starch retrogradation increases yield stress. High-purity silicone fluids maintain stability over months of testing, while aqueous paper coatings alter their internal structure across minutes. Mineral pigments settle, latex emulsion particles form loose agglomerates, and soluble binders re-associate into three-dimensional gel networks.
Viscometers equipped with digital data logging record the decay of torque across time at a fixed rotational speed. The initial peak reading captures the breakdown of static gel structures formed while the slip stood idle in the testing beaker. Subsequent torque decay traces the destruction of temporary pigment flocs under sustained hydrodynamic shear.
At 25.0 degrees Celsius and 100 revolutions per minute, a standard RV-3 element registers 1,240 millipascal-seconds in a sixty-four percent calcium carbonate slip.
Thixotropic Decay and Rest Intervals
Aqueous mineral suspensions undergo progressive gel structure breakdown under prolonged mechanical agitation. When testing staff engage the drive arbor, the recorded torque reaches a maximum value within five revolutions before decaying toward a stable plateau. This time-dependent loss of resistance defines thixotropy.
Standard testing protocols fix the elapsed rotation time at sixty seconds to ensure measurements reflect reproducible dynamic equilibrium. Taking readings after five seconds captures transient gel strength, producing values up to forty percent higher than sixty-second readings. Taking readings after ten minutes introduces viscous self-heating that thins the fluid artificially.
Testing technicians control sample history before lowering the measuring head into the fluid. Storing coating slips in sample jars without agitation allows pigments and polymer binders to rebuild structural networks. The qualification sequence tracks fluid rest intervals to guarantee repeatable initial conditions across shifts:
- Agitation duration sets the initial structural dispersion through three minutes of low-speed propeller stirring at five hundred revolutions per minute.
- Quiescence period allows entrapped air bubbles to rise out of the fluid during ten minutes of undisturbed rest inside a sealed vessel.
- Equilibration stage brings the core fluid mass to within 0.2 degrees Celsius of target temperature using a jacketed water bath.
- Pre-shear interval establishes uniform rotational momentum through fifteen seconds of drive element rotation prior to timed data acquisition.
- Reading acquisition locks the analog brake or triggers the digital register at sixty seconds of continuous drive element rotation.
Latex migration ruins print gloss. Chemical suppliers often claim that elevated bench viscosity readings simply reflect batch variability that disappears once the slip reaches the high-shear coating head.
Solids
Mineral slip volume fractions govern hydrodynamic resistance in aqueous formulations. The relationship between dry solids percentage and apparent viscosity follows an exponential curve dictated by the Krieger-Dougherty equation. Below sixty percent solids by weight, particles move freely through the continuous aqueous phase, producing low apparent viscosity and minimal inter-particle contact.
As dry solids increase toward sixty-eight percent, particle spacing contracts until the mineral volume approaches the maximum packing fraction. At this threshold, minor variations in dry substance trigger massive shifts in apparent viscosity. A formulation shift from 64.0 to 65.5 percent dry solids doubles Brookfield drag under identical temperature and chemical dispersion conditions.
Water loss thickens the slip. Paper mills maximize coating solids to reduce drying energy demand in air flotation hoods and gas infrared heaters. Evaporating water from a wet coating layer consumes substantial energy per metric ton of manufactured paper.
Increasing solids from 60 to 65 percent dry weight reduces required water evaporation by nearly twenty-two percent per ton of finished stock. This thermal efficiency improvement creates severe rheological trade-offs. Formulations running near maximum dry packing leave zero headroom for ambient evaporation or base sheet water absorption.
Slurries thicken rapidly inside coater feed pans, generating streaking defects and blade blade bleeding.
| Process Operation | Shear Rate Range (s⁻¹) | Target Viscosity (mPa·s) | Primary Measurement Tool | Dominant Failure Mode |
|---|---|---|---|---|
| Storage Tank Agitation | 1 to 10 | 1,500 to 3,500 | Brookfield RV (10 RPM) | Pigment settling, gel stratification |
| Screen Filtration | 50 to 200 | 800 to 1,800 | Brookfield RV (100 RPM) | Screen blinding, delivery starvation |
| Application Roll Nip | 1,000 to 10,000 | 150 to 450 | Rotational Cup-and-Bob | Mist generation, uneven film split |
| Metering Blade Nip | 500,000 to 1,500,000 | 25 to 65 | Hercules High-Shear / Capillary | Blade scratches, weeping, web breaks |
| Post-Blade Leveling | 1 to 50 | 500 to 1,200 | Brookfield RV (20 RPM) | Blade lines, orange peel pattern |
Slurry Concentration and Viscous Escalation
Pigment volume fraction sets the hydrodynamic boundary for aqueous paper coatings. Calcium carbonate particles ground to ninety percent finer than two microns pack more efficiently than plate-like kaolin clay. Clay platelets slide over one another during gentle flow, but their wide aspect ratios consume hydrodynamic volume, raising apparent viscosity at identical solids loading.
Pre-coat formulations combine sixty parts coarse carbonate with forty parts fine clay to balance opacity against flow resistance. Topcoat slips utilize ultrafine carbonate alongside delaminated clay to produce high gloss and ink holdout on coated woodfree grades.
Excess dispersant destabilizes the slurry. Sodium polyacrylate dispersants coat mineral surfaces with negative ionic charges, creating electrostatic repulsion that prevents particle agglomeration. Technicians establish the dispersant demand curve by adding incremental amounts of chemical additive while tracking Brookfield viscosity at one hundred revolutions per minute.
Viscosity drops steadily until reaching a sharp minimum known as the optimal dispersion point. Adding polyacrylate beyond this point introduces free sodium ions into the aqueous phase, which compresses the electrical double layer and triggers pigment flocculation. Viscosity rises sharply, mimicking the behavior of an under-dispersed slip.
Binder Demand and Water Retention Mechanics
Styrene-butadiene emulsions and soluble starches dictate how quickly an aqueous phase leaves the pigment filter cake into the base sheet. Synthetic latex polymers arrive as forty-eight to fifty percent solids dispersions that contribute minimal hydrodynamic drag compared to dissolved starches. Substituting starch with latex lowers Brookfield viscosity while maintaining total dry solids content.
Starches absorb free water, swelling into coiled molecular structures that generate significant low-shear flow resistance. Coating recipes requiring high stiffness, such as folding boxboard liners, accept the higher viscosity of cooked starch to control manufacturing costs.
Base sheet absorbency extracts water from wet coating films immediately upon application. If a formulation releases water too rapidly, solids content at the blade tip spikes several percent above the feed pan value. Technicians measure water retention values using AA-GWR gravimetric pressure filtration units under 0.5 bar pressure for two minutes.
Formulations demonstrating poor water retention lose their continuous phase into the raw base paper, leading to blade scratching and premature filter clogging. Adding synthetic rheology modifiers such as alkali-swellable acrylic emulsions or carboxymethyl cellulose stabilizes water retention while elevating Brookfield viscosity across low shear ranges.
What remains unsettled across regional testing programs is whether ambient humidity drift during bench testing alters the apparent solids fraction sufficiently to corrupt inter-laboratory correlation audits.
Metering
Blade coaters subject mineral slurries to velocity gradients reaching one million reciprocal seconds. The bench Brookfield instrument operates below fifty reciprocal seconds, creating a vast shear rate divide between receiving laboratory tests and high-speed coater heads. Slurries that display excellent leveling in a beaker can exhibit severe shear thickening under the mechanical pressure of a metering blade.
Shear thickening occurs when packed pigment particles dilate under intense hydrodynamic stress, jamming against one another and locking the fluid into a rigid, semi-solid state. When dilated coating reaches the blade nip, hydraulic force lifts the steel blade off the backing roll, causing coat weight surges, uneven coverage, and web breaks.
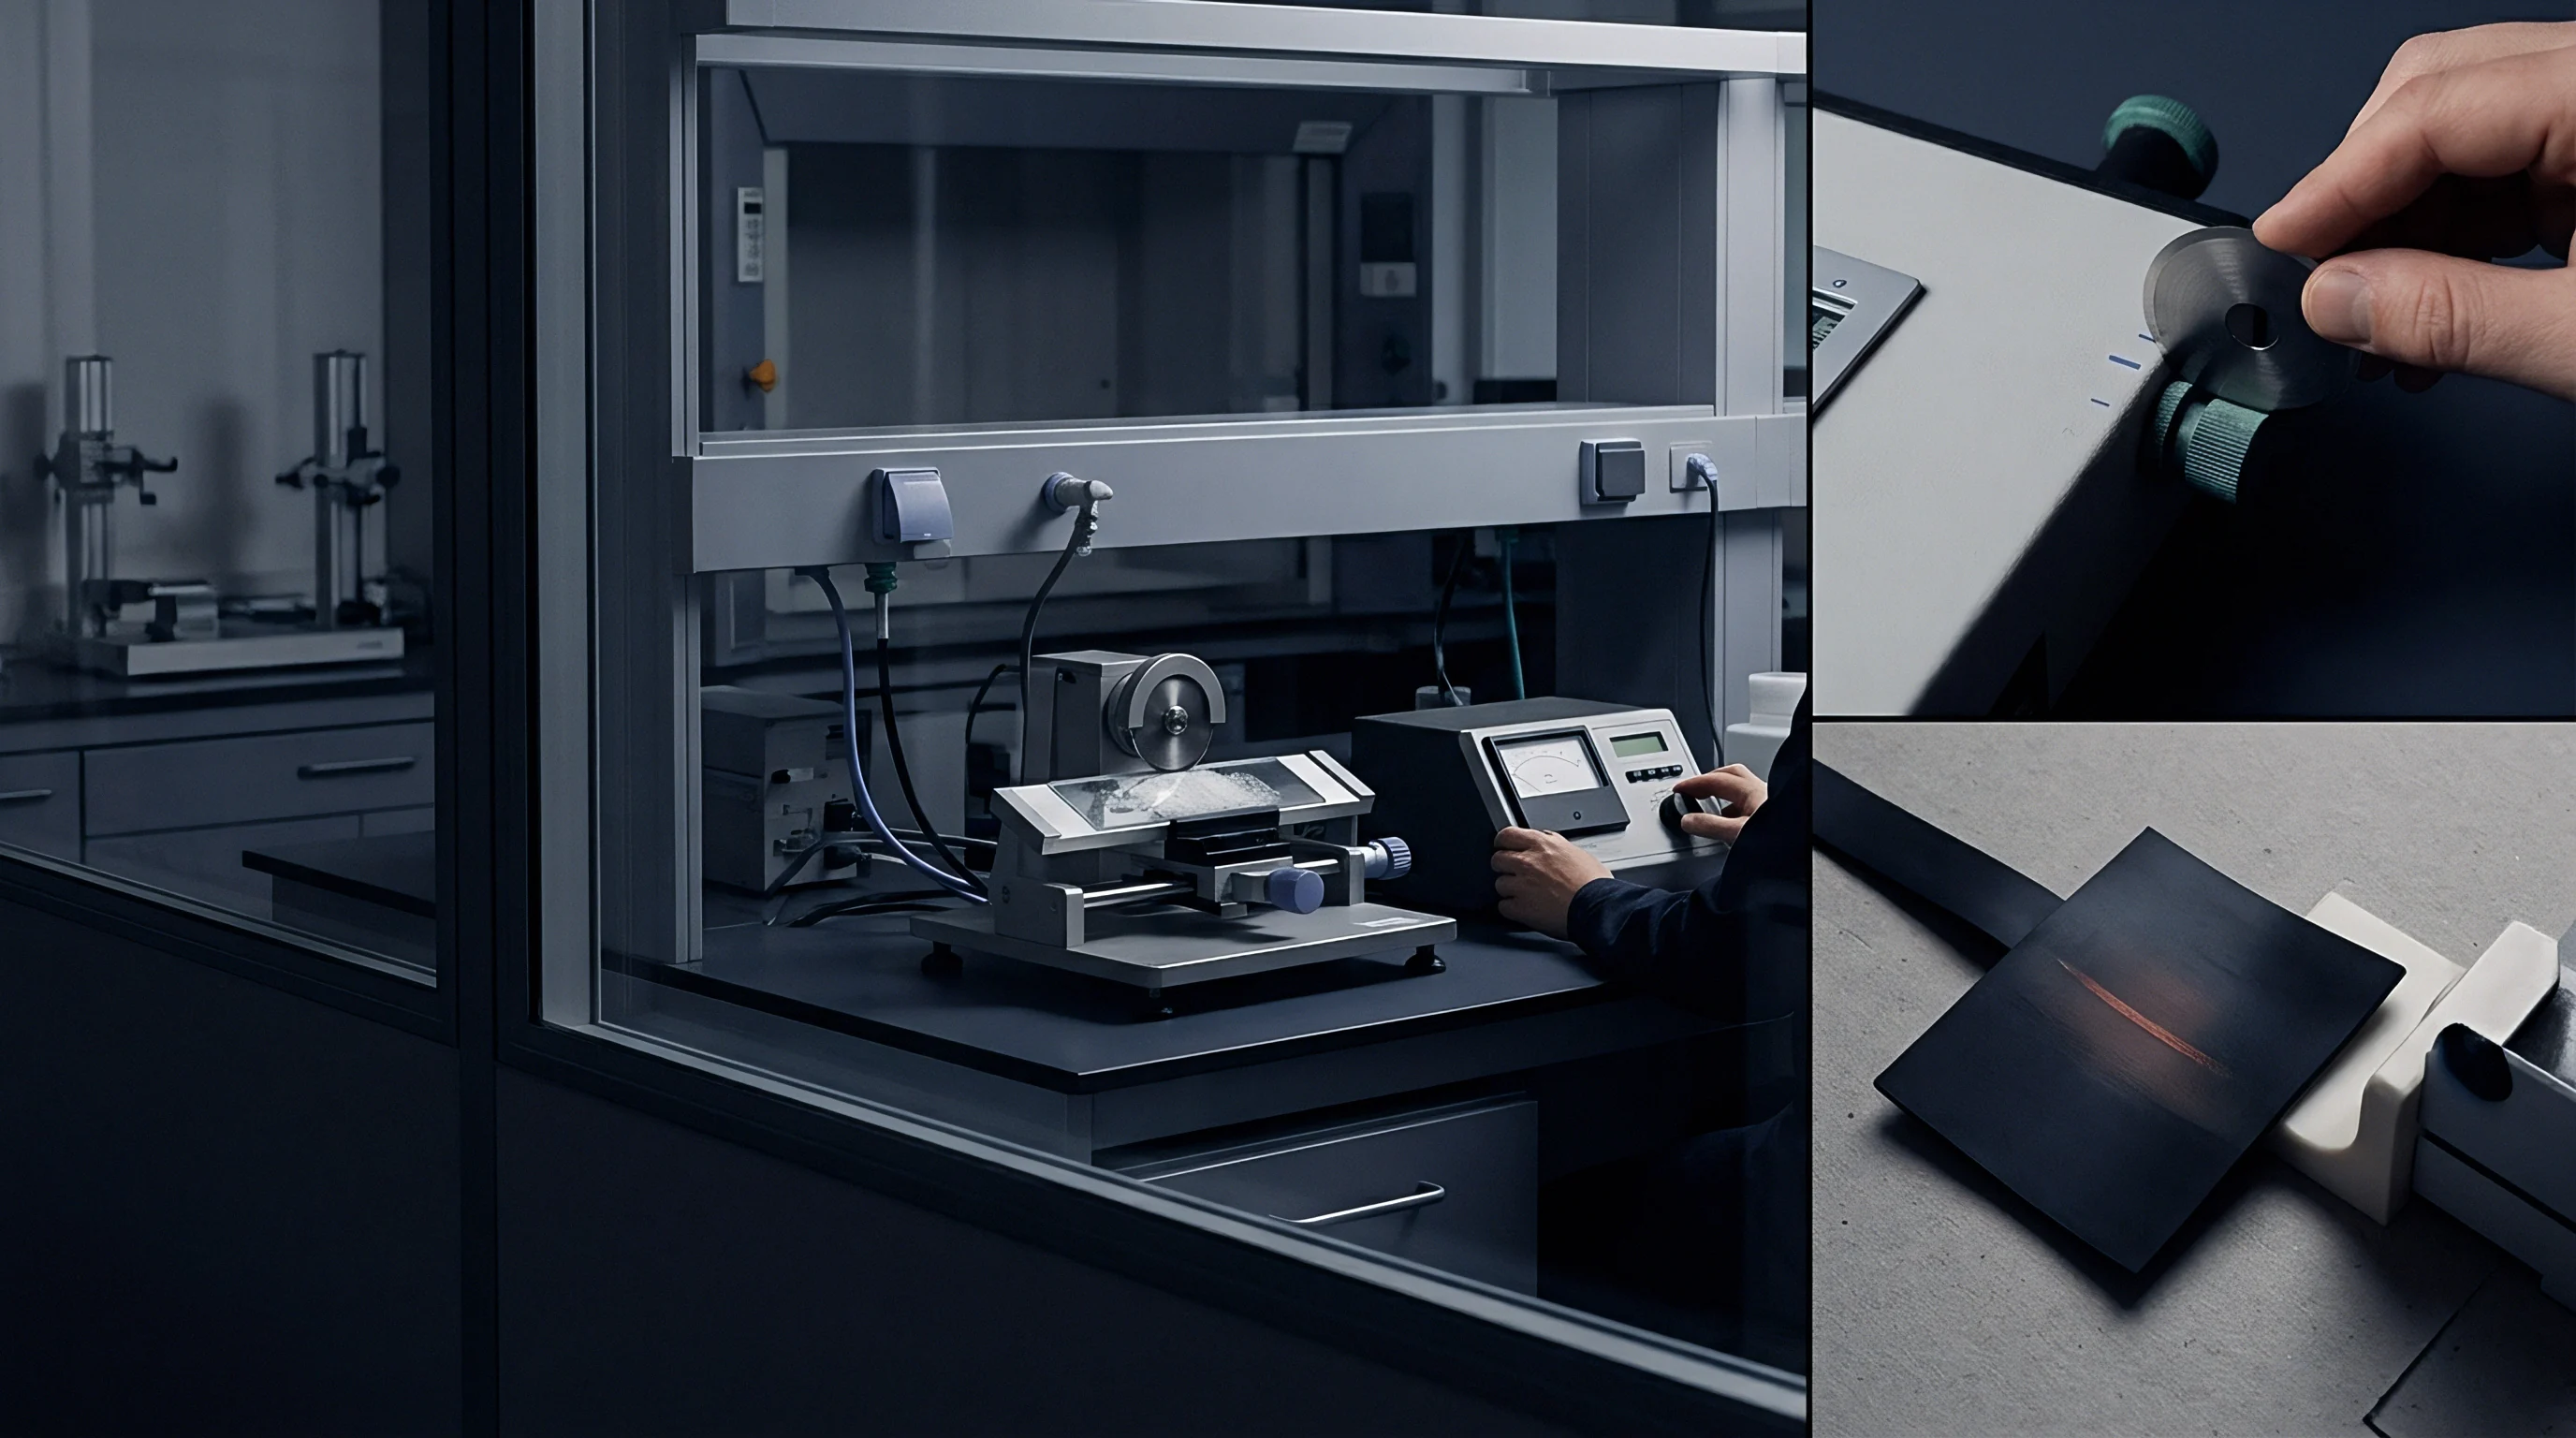
Blade scratches ruin finished rolls. Hercules high-shear viscometry bridges this measurement gap under TAPPI T 648 cm-88. The Hercules instrument employs an automated bob-and-cup geometry driven by an electric motor accelerating up to 8,800 revolutions per minute.
The bob sweeps a narrow annular gap of 0.05 millimeters, generating shear rates past forty thousand reciprocal seconds. Testing staff record the resulting torque deflection across a programmed acceleration and deceleration ramp, producing a complete rheogram curve. The shape of the up-curve and down-curve reveals structural characteristics that remain completely invisible on a bench Brookfield dial.
Under TAPPI T 648 cm-88, failure to report the thermal index within plus or minus 0.5 degrees Celsius voids the certified high-shear viscosity certificate.
Shear Regime Divergence across Processing Zones
High-speed application stations operate across distinct shear regimes simultaneously. In the supply pan and transfer pipework, low shear forces prevail, making Brookfield data relevant for pump sizing and line drainage. At the applicator roll nip, medium shear forces between five thousand and fifteen thousand reciprocal seconds govern film splitting and coat weight transfer.
Beneath the flexible steel metering blade, shear rates accelerate exponentially across a fraction of a millisecond. If the fluid cannot dissipate energy through laminar shear thinning, mechanical friction damages the web surface.
Kaolin particles align under shear. Under moderate flow, asymmetric clay platelets orient themselves parallel to the direction of web travel, lowering effective hydrodynamic resistance. Ultrafine ground calcium carbonate particles maintain spherical shapes that roll across one another, providing lower apparent viscosity across broad shear ranges.
Blending plate-like clay with spherical carbonate optimizes packing density while mitigating dilatant jamming under the blade. Technicians analyze the hysteresis loop generated during Hercules testing to verify that pigment particles realign smoothly during rapid machine speed transitions.
| Formulation Blend (Parts Dry) | Solids Level (%) | Brookfield (100 RPM, mPa·s) | Hercules (4,400 RPM, mPa·s) | Coater Runnability Profile |
|---|---|---|---|---|
| 100 GCC / 11 SB Latex / 0.5 CMC | 68.0 | 1,450 | 42.5 | Clean blade runnability, low drying load |
| 70 GCC / 30 Clay / 12 SB Latex / 1.0 Starch | 65.0 | 1,850 | 58.0 | Stable leveling, moderate fiber coverage |
| 40 GCC / 60 Clay / 10 Latex / 3.0 Starch | 61.5 | 2,400 | 76.0 | High fiber coverage, heavy drying demand |
| 100 Fine Clay / 14 SB Latex / 1.2 Synthetic Thickener | 58.0 | 2,100 | 84.0 | High gloss, prone to blade weeping at high speed |
High Rate Rheogram Construction under TAPPI Rules
Hercules bob-and-cup assemblies quantify structural resistance under rapid rotational acceleration. The instrument sweeps from zero to 4,400 or 8,800 revolutions per minute within twenty seconds, pausing briefly before decelerating back to zero along an identical timeline. Plotting rotational speed against torque generates a continuous flow curve.
The area between the up-curve and down-curve defines the thixotropic or dilatant hysteresis loop. A down-curve shifting to the left of the up-curve confirms structural thinning under shear, indicating that the coating color flows freely after passing through the blade nip.
High shear exposes dilatant rheology. A down-curve shifting to the right of the up-curve indicates shear-induced dilatancy. Slurries demonstrating dilatancy absorb mechanical energy from the coater drive, increasing motor loads and generating heat inside the application pan.
Technicians monitor several operational failure modes linked directly to abnormal flow curve profiles:
- Blade bleeding manifests as continuous dripping of dried pigment paste along the trailing edge of the metering blade assembly.
- Coating spitting ejects fine droplets of color forward onto the freshly coated sheet surface behind the blade tip.
- Scratch formation cuts continuous linear voids into the wet coating film when rigid particle clusters lodge beneath the blade.
- Whiskering defects generate fine, hair-like dried deposits along the coat weight control bevel during high-speed runs.
- Web severing tears the paper sheet under excessive hydraulic pressure peaks generated by dilatant fluid jamming.
Blade pressures exceed three bar. When mill operators fail to detect shear-thickening behavior in inbound slurries, excessive hydrodynamic blade deflection forces emergency line shutdowns that spoil tons of unfinished base paper.
Recirculation
Continuous pumping through pressure screens subjects returned slip volumes to intense hydrodynamic friction. Industrial coating kitchens deliver color to the coater head at flow rates three to five times higher than the actual coat weight applied to the paper web. Unmetered excess coating drains off the applicator roll and returns through open flumes back into the coater machine chest.
This returned fraction undergoes repeated heating, mechanical shearing, and atmospheric exposure. Over several hours of continuous operation, recirculated color accumulates paper fibers, surface lint, and loose sizing picked up from the moving base web.
Screen blinding stops coating delivery. De-aeration cyclones remove air bubbles entrained during drain flume transit. If foam control fails, compressed air bubbles pass through delivery screens, altering apparent viscosity measurements taken on the return line.
Entrained air acts as a compressible phase that dampens torque response in rotational viscometers, producing misleadingly low apparent readings while disrupting volumetric coat weight metering on the paper machine. Formulators add polysiloxane or fatty alcohol defoamers to destabilize surface foam without reducing pigment wetting.
Mineral slurries exhibiting pronounced shear thickening at the coater blade deposit streaks across the web regardless of base sheet smoothness.

Mechanical Degradation across Delivery Loops
Pumping cycles exert continuous mechanical work on soluble binder molecules. Centrifugal pumps running at high impellor speeds clip long-chain carboxymethyl cellulose and synthetic thickener molecules, permanently reducing low-shear viscosity over prolonged recirculation runs. At the same time, water evaporates continuously from open drain channels, elevating total solids content by 0.5 to 1.5 percent across an eight-hour shift.
These opposing mechanisms create a challenging balance where falling polymer molecular weight lowers structural body while rising solids levels elevates particle crowding.
Dry coat weight dictates opacity. To maintain stable running conditions, automated kitchen systems monitor return loop viscosity and density continuously. When line sensors detect rising solids, fresh demineralized water blends into the return chest to re-establish target dilution.
If low-shear viscosity drops due to polymer shear degradation, dosing pumps inject fresh rheology modifier directly into the working batch. Automated adjustments keep delivery color within acceptable processing limits, preventing variations in ink receptivity and mottle across coated print rolls.
Commercial Acceptance Criteria on Mill Delivery
Purchase agreements for pre-dispersed pigment slips define permissible variation before discharge into storage silos. Commercial contracts specify dry solids content, minimum ISO brightness, particle size distribution, and low-shear Brookfield viscosity bands measured under standard reference conditions. Tanker drivers submit a certified delivery docket listing laboratory test figures taken at the supply terminal prior to dispatch.
Mill receiving technicians pull verification samples directly from tanker discharge valves before authorizing hookup to bulk storage tanks. Slurry acceptance testing requires identical instrument geometries, rotational speeds, and temperature controls to resolve discrepancies.
Standard delivery clauses require apparent viscosity to fall within plus or minus one hundred millipascal-seconds of target values at 25.0 degrees Celsius, and any lot exceeding these thresholds triggers mandatory price adjustments or product rejection.