Sheet Margin
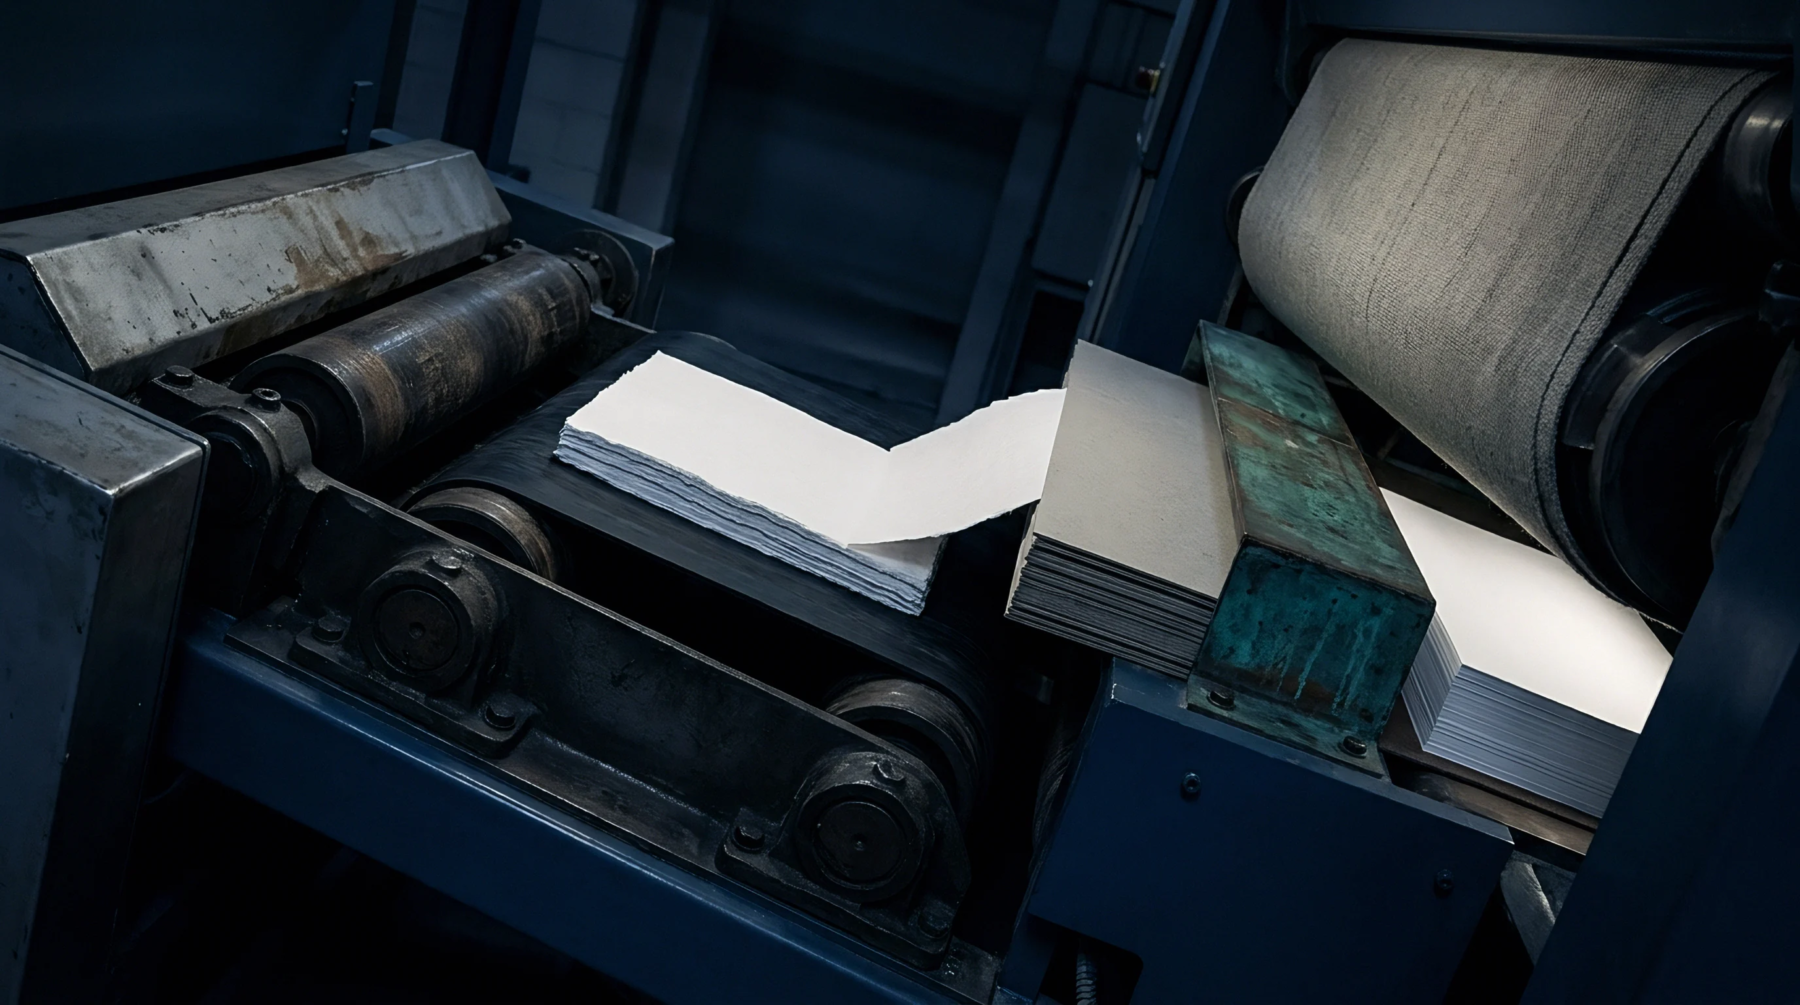
Mill operations remove the outer perimeter strip during web finishing to correct edge damage from winding tensions. Paper converters rely on trim waste recovery systems to capture fibrous edges generated by rotary slitters before the reels reach final sheeting lines. Production managers quantify this discarded fraction by weighing baled edge strips against total input tonnage delivered from the paper machine.
Converting plants generate trim waste continuously whenever wider parent rolls undergo slitting to match narrower customer specifications. Slitter blades operating at high speeds create a continuous ribbon of surplus cellulose along both sides of the moving web. Pneumatic suction ducts draw these fibrous remnants away from the cutting heads toward central collection cyclones situated outside the main production floor.
Automated balers compress the collected side strips into dense cubes for transport back to the pulping room. Pulpers dissolve the baled trimmings alongside virgin chemical pulp to reclaim the cellulose fibres within the internal recycling loop. Slitting tolerances dictate the minimum width required for clean edge removal without sacrificing usable substrate surface area.
Scrap Value
Financial recovery depends heavily on cleanliness standards applied during edge collection and subsequent baling operations. Purchasing departments track scrap pricing fluctuations across regional paper markets to determine whether selling baled trimmings yields higher returns than internal repulping. Contaminated edge strips containing extrusion coatings or solvent-based printing inks suffer severe market devaluation because deinking plants reject mixed paper grades.
Converting facilities achieve higher yields by separating unprinted white board trimmings from laminated duplex grades at the extraction point. Mill accountants monitor the monetary loss incurred when high-cost specialty substrates end up in low-grade baled scrap categories.
Fiber Yield
Cellulose recovery rates drop when slitting blades become dull and generate excessive dust rather than clean side ribbons. Board manufacturers measure fibre retention efficiency by comparing dry input weight against finished output tonnage minus collected edge mass. Proper tension control prevents web wandering which forces operators to widen the cutting margin and discard greater volumes of usable board.
Plant engineers adjust blade angles periodically to minimize the surface area lost to side trimming during high-speed board production runs.