Repulpable Barrier Board Moisture Resistance Testing Protocols
Water resistance on repulpable barrier board requires paired flat and scored gravimetric transmission data alongside verified fiber acceptance screen yields.

Barrier
Water resistance on repulpable paperboard relies on water-based dispersion coatings applied directly to virgin or recycled solid bleached sulphate and folding boxboard substrates. These polymer chemistries, predominantly acrylic co-polymers, styrene-butadiene emulsions, and bio-derived polyester dispersions, replace extruded polyethylene or laminated aluminum foil layers. The operational objective balances liquid water holdout and water vapor retardation against the chemical fragmentation required inside a hydrapulper.
The sheet must release its fibers cleanly through standard mill screening baskets without yielding micro-stickies or tacky polymeric agglomerations that blind wire meshes.
Liquid water holdout differs mechanically from water vapor resistance. Hydrophobic surface sizing treatments prevent bulk droplet penetration by elevating contact angles above ninety degrees. Water vapor molecules exploit microscopic voids, pinholes, and polymer free volume under driven relative humidity gradients.
Achieving a low water vapor transmission rate demands a dense, defect-free polymer matrix across the cellulose surface. The converting line tests this coating matrix through severe shear, tension, and heat exposure during calendering, printing, and rotary die-cutting.
ISO 535 standardizes the liquid water absorption rate by clamping one hundred square centimeters of board beneath a specified head of distilled water for exact exposure intervals.
The Cobb test remains the entry-level verification tool on the finishing floor. Mill datasheets quote thirty-minute or two-hour Cobb values, yet barrier performance for chilled food or frozen secondary cartons hinges on long-exposure regimes. Water penetration under hydrostatic head swells the underlying cellulose networks, disrupting the coating bond.
The table below outlines standard laboratory targets applied to repulpable dispersion-coated folding boxboard grades across primary industrial testing protocols.
| Substrate Class | Coating Chemistry | Test Standard | Target Range | Operational Criterion |
|---|---|---|---|---|
| Solid Bleached Sulphate 280 gsm | Styrene-Acrylic Dispersion | ISO 535 (Cobb 1800s) | 6 to 12 g/m² | Edge wicking suppression |
| Folding Boxboard 320 gsm | Bio-PBS Dispersion | ASTM E96 (38°C, 90% RH) | 15 to 25 g/m²·day | Tropical vapor exclusion |
| Recycled Clay Coated 350 gsm | Aqueous Wax-Free Polymer | ASTM F1249 (23°C, 50% RH) | 3 to 8 g/m²·day | Dry ambient storage barrier |
| Solid Bleached Sulphate 300 gsm | Ethylene Acrylic Dispersion | TAPPI T 441 (Cobb 300s) | 2 to 5 g/m² | Direct condensation resistance |
A dispersion coating that meets twenty grams per square meter per day on an unprinted flat swatch routinely fails at sixty grams when evaluated on the plant floor. Mechanical stresses from downstream converting passes alter the barrier film. Line managers observe coating micro-fissures behind the pull rolls and die nip.
The sheet structure retains the memory of each nip excursion.
When converters ignore this structural shift, finished carton contents cake, soften, or pull moisture from the refrigerated air supply, invalidating shelf-life agreements across distributed logistics channels.

Flaw
Pinholes and micro-cracks compromise barrier coatings before the printed sheet leaves the die press. Aqueous dispersions form dry films through particle coalescence driven by moisture evaporation in the drying tunnel. Insufficient dwell time, rapid surface skinning, or uneven air knife air delivery traps residual moisture pockets.
These pockets rupture, forming capillary pathways through the coating plane down to the raw cellulose fibers. Pinholes allow rapid liquid transfer independent of the polymer bulk permeability values.
Porosity detection protocols determine the physical frequency of these film discontinuities. The turpentine test under TAPPI T 454 offers a crude indicator, but modern aqueous barriers require surface tension dye penetration solutions. A typical testing formulation pairs ethanol with water and a contrasting red rhodamine or methyl blue dye.
Technicians distribute the fluid across an exposed quadrant of board for two minutes, wiping the residue cleanly before inspecting the unconditioned reverse face. Discoloration indicates continuous capillary paths directly through the substrate caliper.
Why Do Coated Films Rupture at Creasing Rules?
Die-cutting imposes acute tensile deformation on the board surface. The steel creasing rule strikes the reverse face, forcing the board into an open channel matrix. The liner layer stretches across the female channel shoulder.
Cellulose fibers flex to accommodate the strain, while the crystalline segments of the dispersion coating reach elongation limits quickly.
Formulations deficient in elastic plasticizers split along the fold ridge. The following failure sequence governs sheet degradation during creasing and folder-gluer operations:
- Tensile strain accumulation occurs when the female matrix depth stretches the outer board plies beyond their native three percent elongation tolerance.
- Coating delamination spreads laterally along the pigment interface when adhesion energy drops below the cohesive shear resistance of the base liner.
- Micro-void propagation creates open fracture channels across the outer apex of the fold, exposing untreated inner cellulose plies directly to ambient relative humidity.
- Capillary wicking pulls condensed water droplets into the internal core, collapsing carton bulge stiffness and dropping flat crush resistance.
Brittle barrier films fail at the outer score line long before base fibers experience physical tearing.
The operational dispute centers on coating weight against flexibility. Increasing aqueous dry coat weights from six grams per square meter to fourteen grams improves flat water vapor barrier figures on the lab bench. The thicker layer hardens, creating brittle zones that shatter into network cracks during folding.
Testing protocols evaluate performance across folded specimens rather than uncreased blanks.
Converters verify fissure severity using microscopic inspection under fifty-times optical magnification. Technicians count fracture occurrences per linear centimeter of crease length. Laboratory measurements verify that a carton with twenty micro-fissures per linear centimeter displays water vapor transmission rates four times higher than flat control swatches.
The plant encounters suppliers asserting that minor score-line micro-fissuring represents normal converting behaviour within standard carton manufacturing tolerances.
Screen
Moisture testing protocols are commercially meaningless if the barrier chemistry prevents the carton scrap from passing standard mill repulpability qualifications. Mill hydrapulpers disperse post-industrial trim and post-consumer packaging using high-shear hydro-mechanical agitation at consistencies between four and twelve percent. Laminated poly-coated boards require specialized mechanical pulpers with extended cycle durations to tear plastic films from the pulp mat.
Repulpable barriers must disintegrate cleanly during standard low-energy cycles within standard ten to twenty-minute processing limits.
Laboratories quantify repulpability following harmonized standards such as PTS RH 021 97 or the CEPI Recyclability Laboratory Test Method Version 2. The pulp slurry travels through standardized Somerville or Haindl screening apparatus equipped with slotted plates. The slots measure precisely 0.15 millimeters in width.
Material retained on top of the slot plate constitutes rejected packaging waste, composed of flakes, unpulped base board, and intact polymer films.
| Substrate Barrier System | Pulper Retention Time | Screen Rejects (0.15 mm) | Acceptance Yield | Standard Classification |
|---|---|---|---|---|
| Extruded LDPE Film (18 gsm) | 20 Minutes | 14.8 Percent | 85.2 Percent | Non-repulpable standard stream |
| Styrene-Acrylic Dispersion (8 gsm) | 10 Minutes | 1.1 Percent | 98.9 Percent | Fully repulpable standard pass |
| Aqueous Dispersion High Wax (12 gsm) | 15 Minutes | 4.6 Percent | 95.4 Percent | Repulpable with stickie risk |
| Bio-Polyester Aqueous Layer (10 gsm) | 20 Minutes | 7.9 Percent | 92.1 Percent | Conditional mill acceptance |
| Test data derived under standard CEPI pulping protocol at 40°C neutral pH without chemical dispersion aids. | ||||
The standard balance creates operational tension. Chemical formulators incorporate cross-linking agents, such as zinc oxide or zirconium compounds, to tie up hydrophilic carboxyl groups and maximize moisture barrier resistance. High degrees of chemical cross-linking resist warm water dispersion inside the pulper vat.
The polymer remains intact as a sheet or fragments into resilient flakes that exceed the 0.15-millimeter screen threshold. The batch yields low accepted fiber ratios, earning a failing grade under standard paper mill collection guidelines.
Micro-stickies pose an equal processing hazard. Water-soluble or colloidal polymer fragments passing through the screen plate re-agglomerate under the mechanical action and temperature fluctuations of downstream papermaking machines. These tacky masses coat dewatering wires, deposit onto drying cylinders, and cause sheet tears.
Repulpability certification requires macro-sorter evaluations and stickie deposition tests on laboratory membrane filtration equipment.
CEPI testing parameters dictate that total laboratory coarse rejects on the 0.15-millimeter slotted plate remain strictly below ten percent of the starting dry board weight.
The testing engineer confirms that the repulping protocol runs at neutral pH without caustic additives unless the packaging specification explicitly states specialty de-inking plant destination channels. Caustic soda swells fibers rapidly, artificially lowering the measured reject percentage on laboratory benches. A packaging substrate depending on alkaline dissolution clogs screens inside standard commercial mills operating closed-loop neutral water circuits.
The testing protocol leaves open the question of how future multi-ply board structures featuring barrier coatings within internal plies will behave during automated optical sorting across recovery plants.
Score
Evaluating barrier performance on pristine flat swatches provides false confidence to packaging engineers. Real packages experience converting, folding, gluing, and environmental cycling. Comprehensive testing protocols mandate measuring the Water Vapor Transmission Rate, Cobb absorption, and dye penetration across defined, repeatable crease structures.
Creasing procedures follow ISO 2493-1 or TAPPI T 829 protocols using precision laboratory creasing apparatus such as the Marbach or Lorentzen & Wettre carton crease testers.
Specimens receive controlled creases along the cross-direction and machine-direction axes. The creasing rule profile, rule height, and die channel width align exactly with the board caliper. An operator folds the creased sample through a one-hundred-and-eighty-degree arc, rolls the fold with a standard two-kilogram rubber roller to simulate automated folder-gluer operations, and flattens the board back to the ninety-degree position.
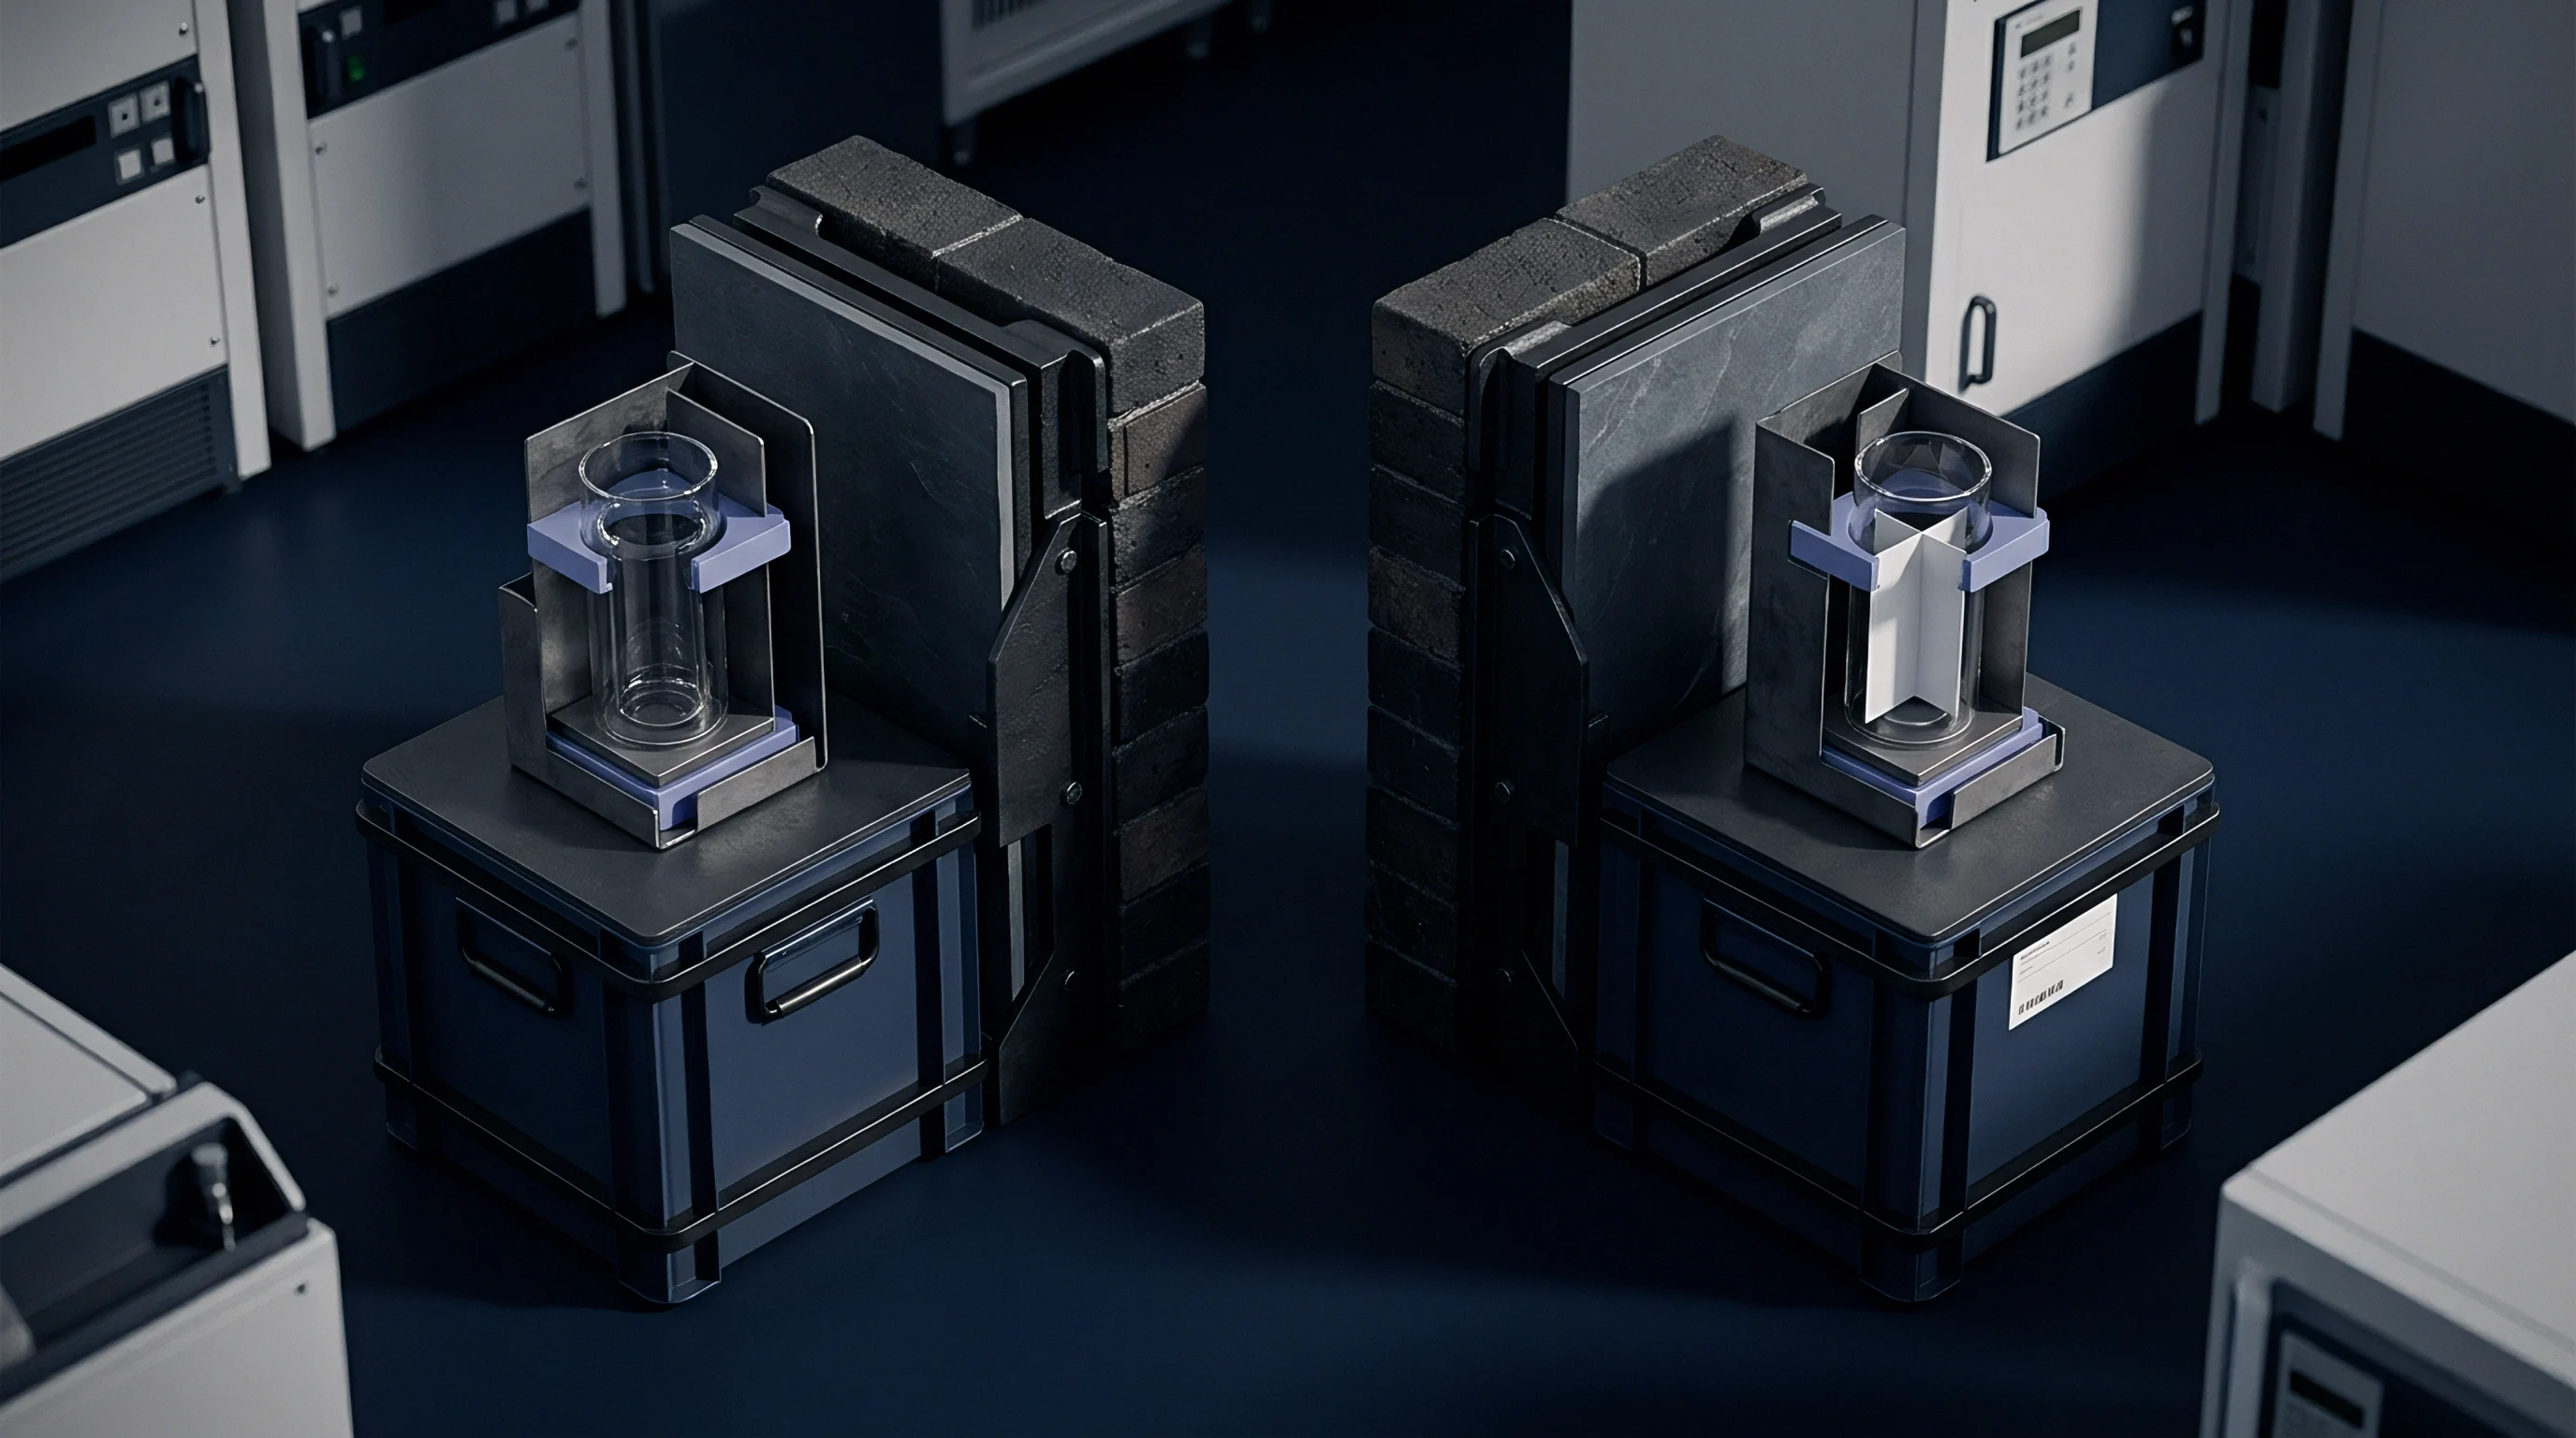
Water vapor transmission cells, such as Mocon or gravimetric cup assemblies, secure this creased apex across the center of the active test chamber orifice.
Where Do Measured Rates Drift Most across Run Batches?
The gravimetric cup procedure governed by ASTM E96 provides an accessible, reproducible protocol for assessing folded barrier board performance under steady-state conditions. Gravimetric cups contain either dry desiccant or distilled water, placed inside environmental chambers held at twenty-three degrees Celsius and fifty percent relative humidity, or tropical conditions of thirty-eight degrees Celsius and ninety percent relative humidity. Automated diffusion cells operating under ASTM F1249 utilize infrared sensors to record transmission kinetics in shorter time spans.
Data consistently reveals performance divergence between flat and folded specimens across diverse aqueous formulations. The list below highlights critical testing failure profiles identified during scored barrier assessments:
- Cross direction fracture spikes appear when the crease runs parallel to the paper machine direction, stressing fragile transverse cross-linked polymer domains beyond their structural threshold.
- Edge wicking delamination occurs where raw unprotected cut board edges absorb migrating condensate, lifting the aqueous barrier film cleanly off the top liner.
- Pinpoint fatigue rupture develops along the corner intersections of trihedral carton folds where compound compressive and tensile forces crush the polymer matrix.
- Adhesive interaction failure emerges when emulsion glue solvents dissolve the underlying moisture barrier, causing structural packaging collapses at the carton side seams.
Consider a standard production run to demonstrate the arithmetic reality of this performance drop. Assume an initial procurement run of forty metric tons of folding boxboard at 300 grams per square meter, bearing an eight-gram aqueous barrier dispersion. The laboratory qualifies the virgin flat sheet at a water vapor transmission rate of 12 grams per square meter per day under thirty-eight degrees Celsius and ninety percent relative humidity.
Production cartons require six mechanical creases across their body panels.
When the scored areas enter the diffusion cell, the measured transmission jumps to 48 grams per square meter per day across the crease zone. Because the creased area represents twelve percent of the total carton surface, the effective average pack transmission calculates to 16.3 grams per square meter per day. This 35 percent jump in daily vapor ingress exceeds the twenty-day critical moisture threshold for powdered food contents.
The entire batch becomes unmarketable for the specified product shelf life.
Crease matrix depth, rule width, and clearance tolerances must match the caliper precisely on the conversion press.
Audit
Verifying moisture barrier packaging requires a structured quality dossier that links raw material mill certificates to converted carton performance. Sourcing teams enforce incoming inspection protocols on delivered board lots. Standard sampling frequencies dictate drawing three random sample sheets from every ten pallets delivered, conditioning the specimens according to ISO 187 parameters of twenty-three degrees Celsius and fifty percent relative humidity for a minimum of twenty-four hours before initiating destructive testing.
An audit protocol mandates continuous traceability from the chemical coater through the die cutter. The technical dossier must incorporate four foundational performance pillars before commercial sign-off:
- Liquid holdout profiles documenting sixty-second, three-hundred-second, and eighteen-hundred-second Cobb absorption values across the coated surface, unprinted reverse face, and cross-directional score lines.
- Vapor transmission records tracking ASTM F1249 or ASTM E96 transmission rates on both pristine and mechanically creased specimens under ambient and accelerated tropical environmental conditions.
- Standard repulpability certifications issued by accredited third-party laboratories executing PTS RH 021 97 or CEPI testing schemes, verifying fiber accept recovery rates above ninety percent.
- Food contact declarations of compliance confirming that the dispersion chemistry, including all defoamers, biocides, and surfactants, adheres strictly to Regulation (EC) No 1935/2004 and FDA 21 CFR 176.170.
Plant auditors run ultrasonic coating thickness gauges or continuous beta-gauge backscatter sensors across the web to detect coat weight variance. Aqueous barrier dispersions applied unevenly across the machine width generate localized hot spots for moisture failure. A dry coat weight tolerance of plus or minus 0.5 grams per square meter represents the commercial ceiling for stable water vapor performance.
When coat weights drift below the minimum threshold, pinhole frequency escalates exponentially.
Converting agreements specify economic remedies when delivered board fails water holdout parameters. Standard contracts establish that any production lot demonstrating creased moisture transmission rates exceeding the agreed threshold by more than fifteen percent triggers an immediate replacement claim at the mill’s expense, alongside reimbursement for downtime and setup tooling on the customer converting floor.