Specular Measurement
A protocol defined by the American Society for Testing and Materials determines the degree of light reflected from a coated or uncoated surface at fixed angles. Known as astm d523, the procedure quantifies the level of visual gloss by comparing reflected intensity against a polished black glass standard. Manufacturers apply this method during the production of packaging materials to ensure that high-finish folding cartons or specialty labels maintain consistent optical properties across production runs.
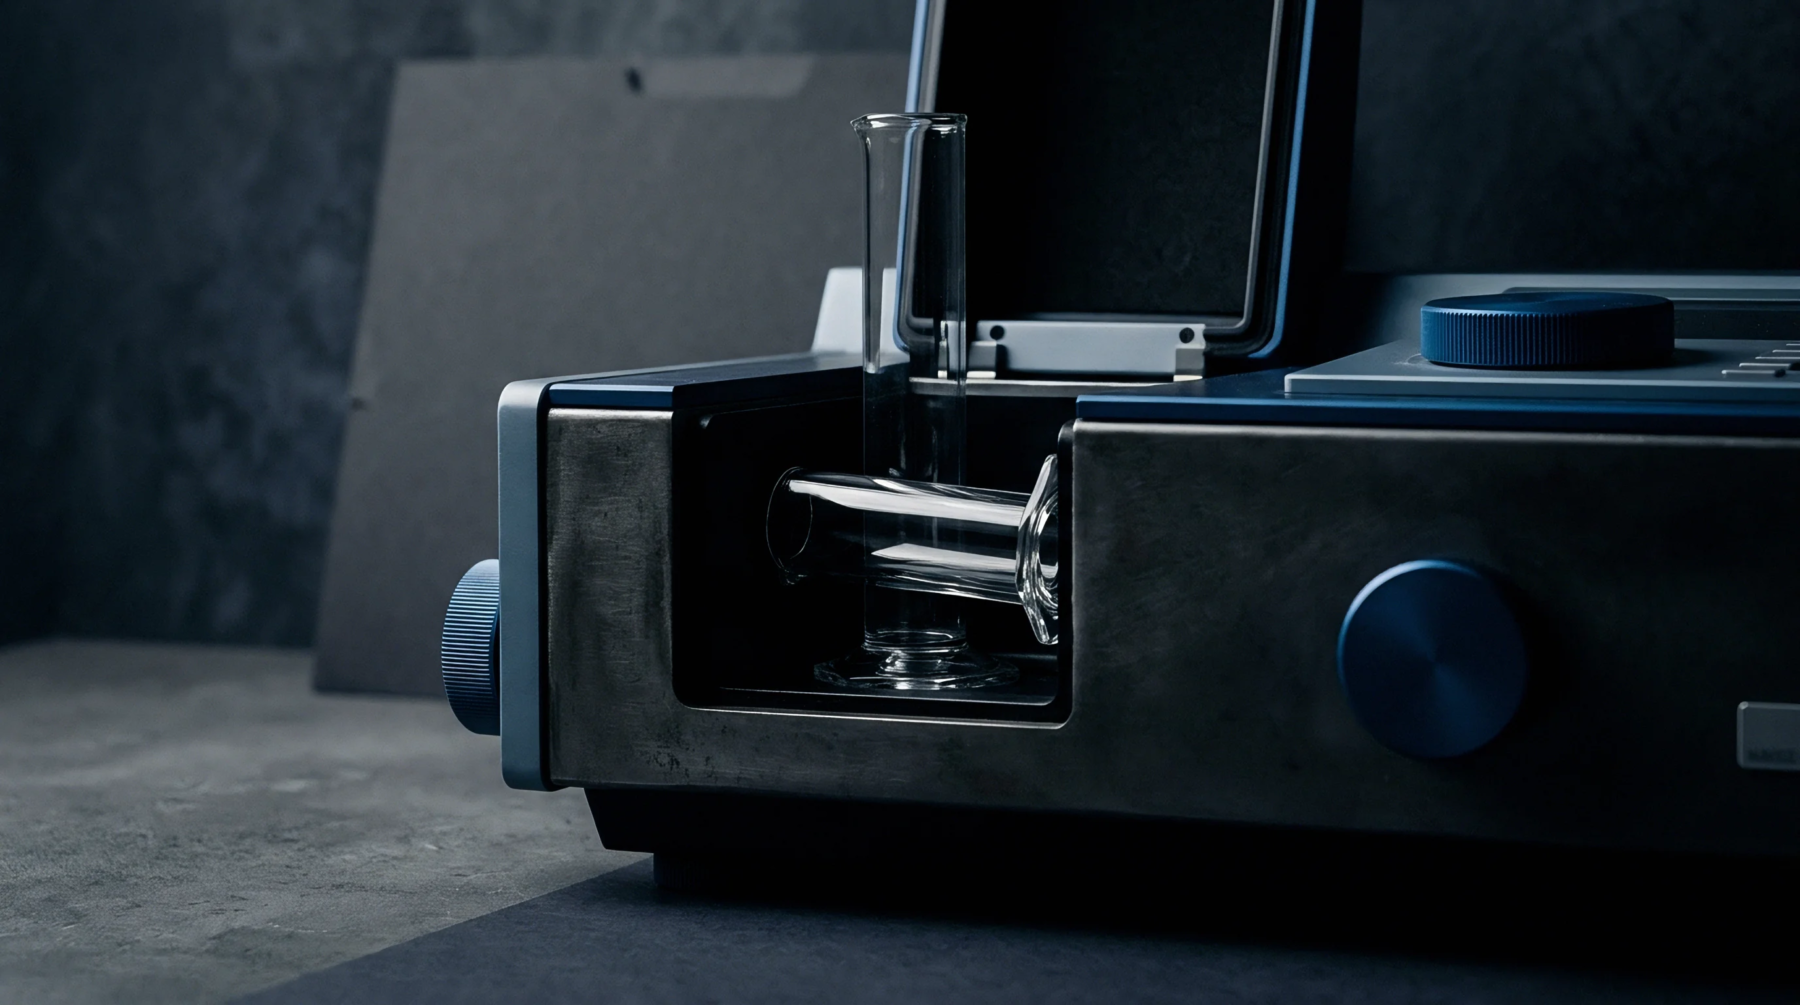
Equipment used in this process includes a glossmeter which projects a beam at an angle of 20, 60 or 85 degrees depending on the target finish range. Sensors detect the amount of light that returns from the specimen to generate a numerical value on a scale from zero to one hundred. Low values indicate a matte texture while higher figures designate a glossy appearance suitable for high-end shelf appeal.
Surface Calibration
Calibration remains the primary safeguard for ensuring that astm d523 provides repeatable output on the converting floor. Technicians verify the accuracy of the light source and the sensitivity of the internal photodetectors before starting a shift. Any variation in the background temperature of the testing room or the orientation of the substrate sample alters the recorded light intensity.
Laboratories establish specific control limits based on the capability of the coating station to produce a stable varnish layer. Operators check these limits against the reference glass tiles supplied with the meter to maintain correlation between different testing stations. Periodic maintenance of the optical lenses removes dust and residue that otherwise interfere with the reflection path.
Accurate data collection depends on the flatness of the paper sample because curls or wrinkles introduce errors in the light angle.
Gloss Tolerance
Printing facilities negotiate a defined window of numerical output to control the visual quality of consumer packaging. Clients demand strict adherence to these limits because variation in reflective output distorts the appearance of printed graphics and brand identity markers. The target value chosen for a specific job dictates the selection of coating chemistry and the application weight of the wet varnish layer.
Production lines reject batches that drift outside the agreed boundaries because the human eye detects small discrepancies in surface finish during bulk display. Measurements provide the objective proof required for quality auditing and supplier compliance.