Friction Measurement
Standardized coefficients of kinetic and static friction define the material performance of paper and board substrates during high speed mechanical processing on filling or conversion lines. Practitioners use iso 8295 to quantify the resistance force encountered when two flat surfaces slide against each other under controlled conditions. This protocol prescribes the use of a sled with a specific mass pulled across a stationary specimen at a constant velocity to generate repeatable data.
Accurate assessment of these surface properties allows engineers to predict how sheets will behave within stackers, hoppers and automated folding equipment. Measurements derived from this process provide the baseline for identifying surface drag that triggers machine jams or erratic sheet feeding.
Processing Dynamics
Converters apply these friction values to verify the performance of aqueous coatings, clay finishes or synthetic laminates applied to base stocks. Excessive static friction prevents single sheets from separating during the feeding sequence of a printing press or a carton forming machine. Low kinetic friction creates instability in a vertical column of stacked packaging materials that causes units to slide out of alignment during shipping or transit.
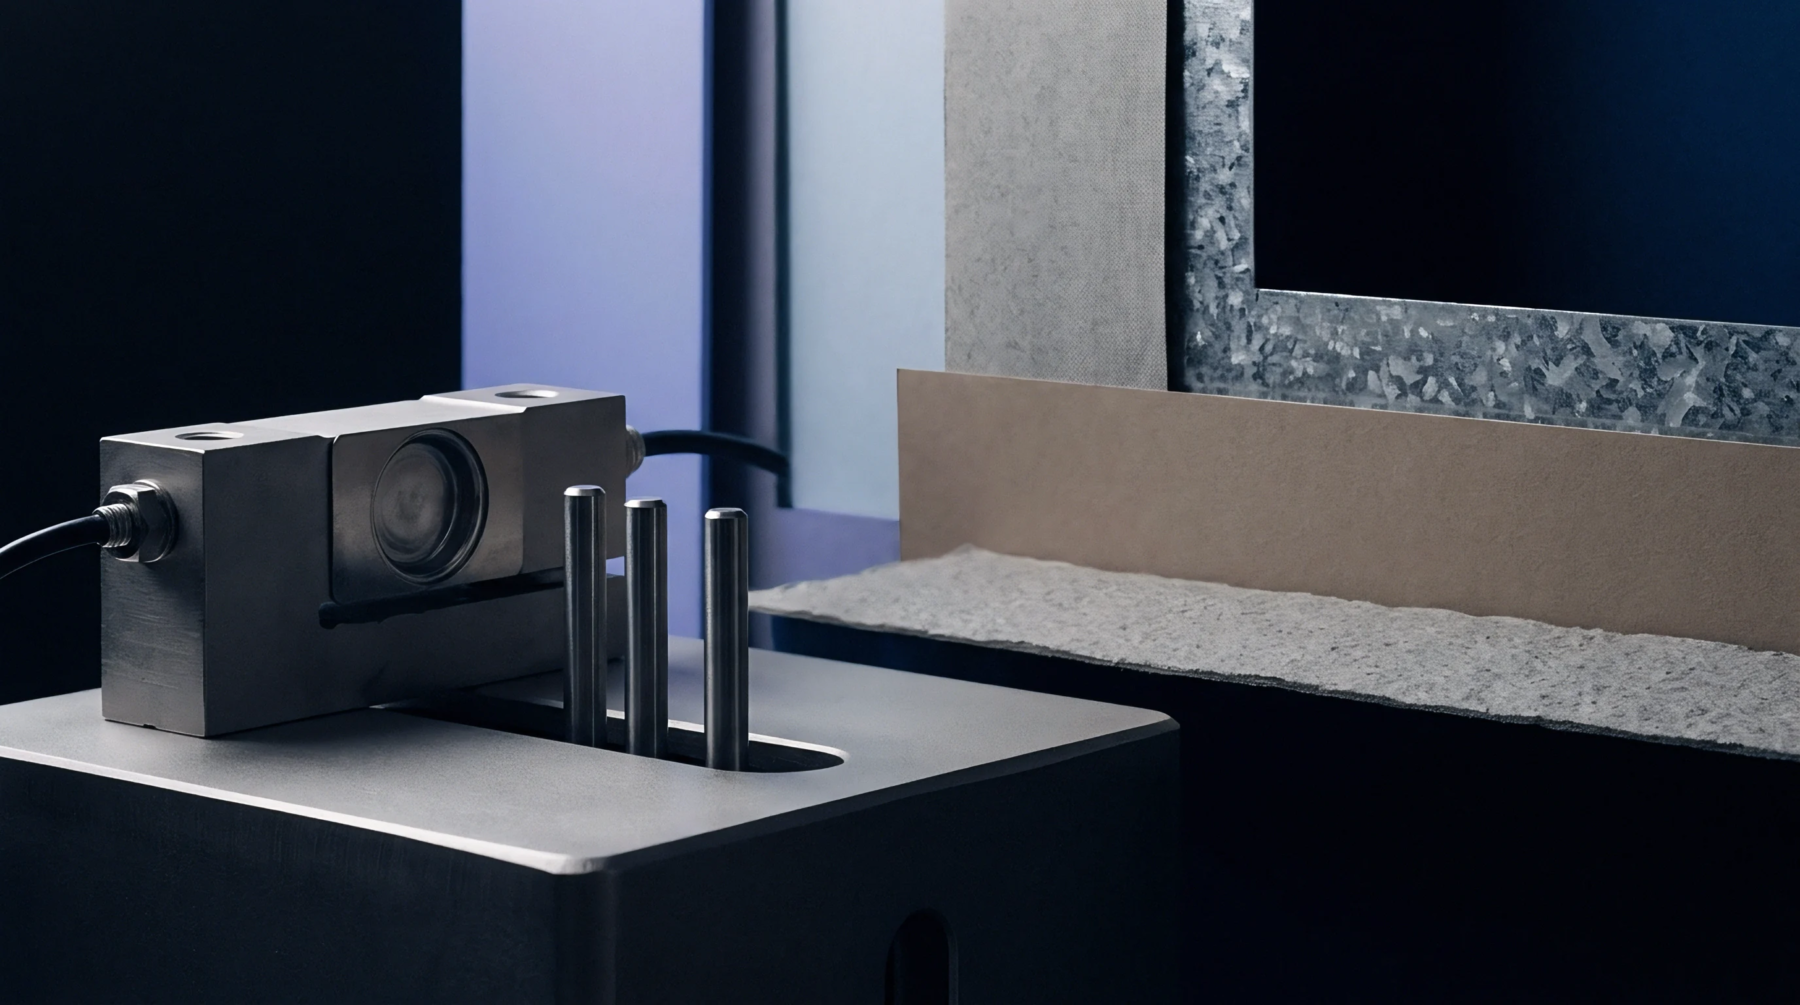
Manufacturers monitor these characteristics to calibrate the tension settings on web fed converting lines where friction variations dictate the success of complex mechanical operations. Lab technicians fix a sample to a horizontal plane and place a weighted sled on the surface to initiate the sliding motion. A load cell records the peak force required to start movement while the average force maintains the sliding velocity.
These numbers feed directly into the friction index required for site specific packaging design.
Surface Constraints
The boundary for these measurements stops at the interface between two similar or dissimilar materials intended for final packaging production. Environmental factors like local humidity and ambient temperature shift the coefficient results by altering the moisture content and surface energy of the substrate. Calibration of the equipment occurs through regular weight verification and alignment checks on the sled path to eliminate bias from mechanical vibration.
Reliability of the reported data depends on the strict adherence to the sled velocity prescribed by the standard. Proper monitoring of these parameters ensures that converted packaging stock maintains the necessary surface grip for high speed production stability.