Z-Direction Shear Resistance and Ply Delamination Mechanics in Recycled Uncoated Folding Grades
Controlled interply shear delamination during creasing prevents outer liner cracking and hinge failure in multi-ply recycled folding cartonboard.
Nip
An internal bond tester releases a pendulum striking an aluminium angle specimen adhered to a 380-micrometre sheet of uncoated recycled folding boxboard. The digital readout records 112 Joules per square metre under ISO 16260 conditions at 23 degrees Celsius and 50 percent relative humidity. That number determines whether five hundred thousand carton blanks pass through a high-speed folder-gluer without blister formation, liner separation, or hinge rupture.
Recycled uncoated boxboard, categorized under commercial designations such as European GD2 and GD3 or North American bending chipboard, relies on stratified multi-ply construction. The outer liners contain sorted recovered office papers or deinked chemical fibres. The thick central core incorporates unsorted mixed waste, recovered corrugated cuttings, and mechanically degraded municipal collections.
Every paper machine press nip consolidates these distinct wet webs into a unitary structure. The resulting z-direction mechanical properties govern how the board responds to shearing forces in carton conversion. Converting failures trace directly to interfacial weaknesses formed during web couching and consolidation.
- Offset blanket delamination pulls the outer liner away from the grey core during high-tack lithographic ink splits. The sheet surface lifts under radial tensile forces.
- Crease line cracking shatters the exterior ply when excessive internal cohesion prevents clean cleavage within the core. Tensile strain exceeds the ultimate elongation limit of recycled fibres.
- Glue tab cleavage splits the internal board strata along packaging line packing funnels. The adhesive joint holds while the recycled core tears apart under spring-back torque.
- Stripping jam cleavage tears carton edges unevenly during automated scrap evacuation on flatbed die-cutters. Jagged borders trigger packing line rejections.
Uncoated recycled chipboard shears along the weakest recycled furnish boundary under rotary creasing stress.
Goods-in verification procedures test basis weight, caliper, and Taber stiffness across machine directions. Delamination resistance receives minimal routine scrutiny at commercial receiving docks. Mill test certificates routinely report Scott internal bond averages gathered from composite reel samples.
Those reel composites smooth out cross-directional variations that cause line stoppages on folder-gluers running eighty thousand units per hour. A board lot presenting compliant bending stiffness can hide catastrophic z-direction shear deficiencies. Converters discover the defect only when creasing knives induce interply cleavage that spreads beyond the designated hinge line.
Machine tenders frequently counter that the board met every nominal caliper and grammage parameter specified on the purchase order.
Interface
Cross-sectional inspection reveals discrete boundaries between the top liner, intermediate filler plies, and bottom backing. Uncoated recycled grades run without mineral pigment coats or synthetic latex binders on the printing surface. Structural strength depends entirely on natural hydrogen bonds formed between cellulosic fibres during press section water removal.
Secondary fibres enter the headbox with reduced swelling potential and irreversible pore collapse from previous drying cycles. Hornification limits specific surface area available for interfacial bonding between successive plies. Papermakers spray cationic corn or potato starch between the couched webs to restore ply adhesion across forming vats.
| Ply Stratum | Furnish Composition | Ash Content (%) | Fibre Length (mm) | ZD Tensile (kPa) |
|---|---|---|---|---|
| Top Liner | Deinked ledger and sorted white shavings | 11.2 | 1.45 | 410 |
| Sub-Liner | Over-issue news and unprinted unbleached kraft | 13.8 | 1.10 | 325 |
| Core Plies | Mixed municipal paper and corrugated scrap | 22.4 | 0.78 | 215 |
| Back Liner | Sorted unbleached kraft cuttings | 8.5 | 1.85 | 380 |
Starch retention depends heavily on spray nozzle distribution, drainage timing, and press section temperature profiles. Uneven starch gelatinization creates dry pockets that shear under minimal load. High ash contents from mineral fillers and deinking residues aggregate in the core.
These calcium carbonate and clay particles occupy hydrogen bonding sites without contributing cohesive strength. When core plies carry twenty percent inorganic filler, cohesive z-direction resistance falls steeply.
Internal bond strength drops twenty-two percent when core ply moisture content increases from six to nine percent under ISO 187 standard atmosphere.
Interply bonding mechanics follow a predictable sequence during cylinder vat and multi-fourdrinier forming.
- Aqueous couching joins individual wet webs at solids contents between twelve and eighteen percent. Dewatering rates dictate physical contact between opposing fibre mats.
- Starch mist application delivers dissolved amylase polymers directly onto the wet consolidating interface. Droplet size governs uniform coverage across the moving web.
- Press nip compaction forces dissolved polymers into opposing porous surfaces while expressing interstitial water. Peak nip pressures range from four to seven megapascals.
- Cylinder drying gelatinization completes the cure cycle as web temperatures pass sixty-five degrees Celsius. Final starch crystallization locks interfacial hydrogen bonds.
Lacking adequate nip compression during couching, the resulting boundary remains fragile throughout converting.
Rupture
Laboratory evaluation separates tensile delamination from pure shearing separation along board plies. Standardized testing under ISO 15754 measures z-direction tensile strength by pulling double-sided adhesive tape fixtures perpendicular to the sheet plane. This method applies uniform normal stress across a thirty-millimetre circular area.
Dynamic creasing and folding subject the internal structure to shear strain parallel to the sheet surface. In-plane shear stresses develop as the creasing rule forces the outer liner into the female channel. The board must delaminate internally into discrete lamellae to relieve compression along the inner fold.
What Governs Delamination Resistance in Recycled Uncoated Cartons?
Placing a recycled folding sheet into a creasing die exposes the internal plies to rapid shear displacement. The male rule compresses the sheet while forcing material downward into the female counter-channel. A properly formulated board shears internally into three or four distinct sheets without tensile rupture on the top face.
This controlled delamination forms a hollow rounded bead on the carton interior. The bead accommodates compressive strain as the carton folds flat. If z-direction shear resistance runs too high, the core refuses to delaminate internally.
| Scott Bond (J/m2) | ZD Tensile (kPa) | Creasing Performance | Litho Tack Resistance |
|---|---|---|---|
| Below 95 | Below 210 | Blistering along hinge lines | Severe blanket delamination |
| 95 to 135 | 210 to 300 | Clean bead delamination | Sufficient for medium tack inks |
| 136 to 180 | 301 to 390 | Optimal hinge folding | Sufficient for high tack inks |
| Above 180 | Above 390 | External liner cracking | Zero blanket lift |
The Scott bond figure of 135 Joules per square metre represents a baseline across European box plants. That value rests on testing protocols using five-sample averages from single reels conditioned under TAPPI T 569. Testing samples across seasonal ambient shifts reveals substantial drift.
Elevating ambient relative humidity from fifty to sixty-five percent drops internal bond values by twenty Joules per square metre. This reduction occurs because moisture plasticizes the cellulosic matrix and softens the retrograded interply starch. The desk cannot fully defend single-point laboratory ratings gathered at the mill when pallets travel through unconditioned winter freight corridors.
Buyers counter this vulnerability by requesting statistical process control charts showing three-sigma margins above minimum shear thresholds.
Specification sheets adhering to ISO 16260 without stated cross-machine sampling intervals leave converters unprotected against localized ply cleavage.
Laminating secondary packaging involves balancing contradictory performance demands. The outer plies demand high tensile modulus, while the core demands moderate shear compliance. Thin packaging geometries exacerbate this balance on carton packaging lines.
In-line vision systems stop high-speed cartoning machines when carton panels bow outward from uncontrolled delamination, generating massive scrap loads and unrecoverable packing down-time.
Rule
Die-cutting tooling setup directly determines whether board plies separate cleanly or fracture under impact. Flatbed and rotary die tools require steel creasing rules with rounded profiles matching the caliper of the cartonboard. Selecting the width of the male rule and the clearance of the female matrix channel governs shear distribution within the sheet.
Channel calculation formulas established in packaging standards specify channel width equal to 1.5 times the sheet thickness plus the rule thickness.
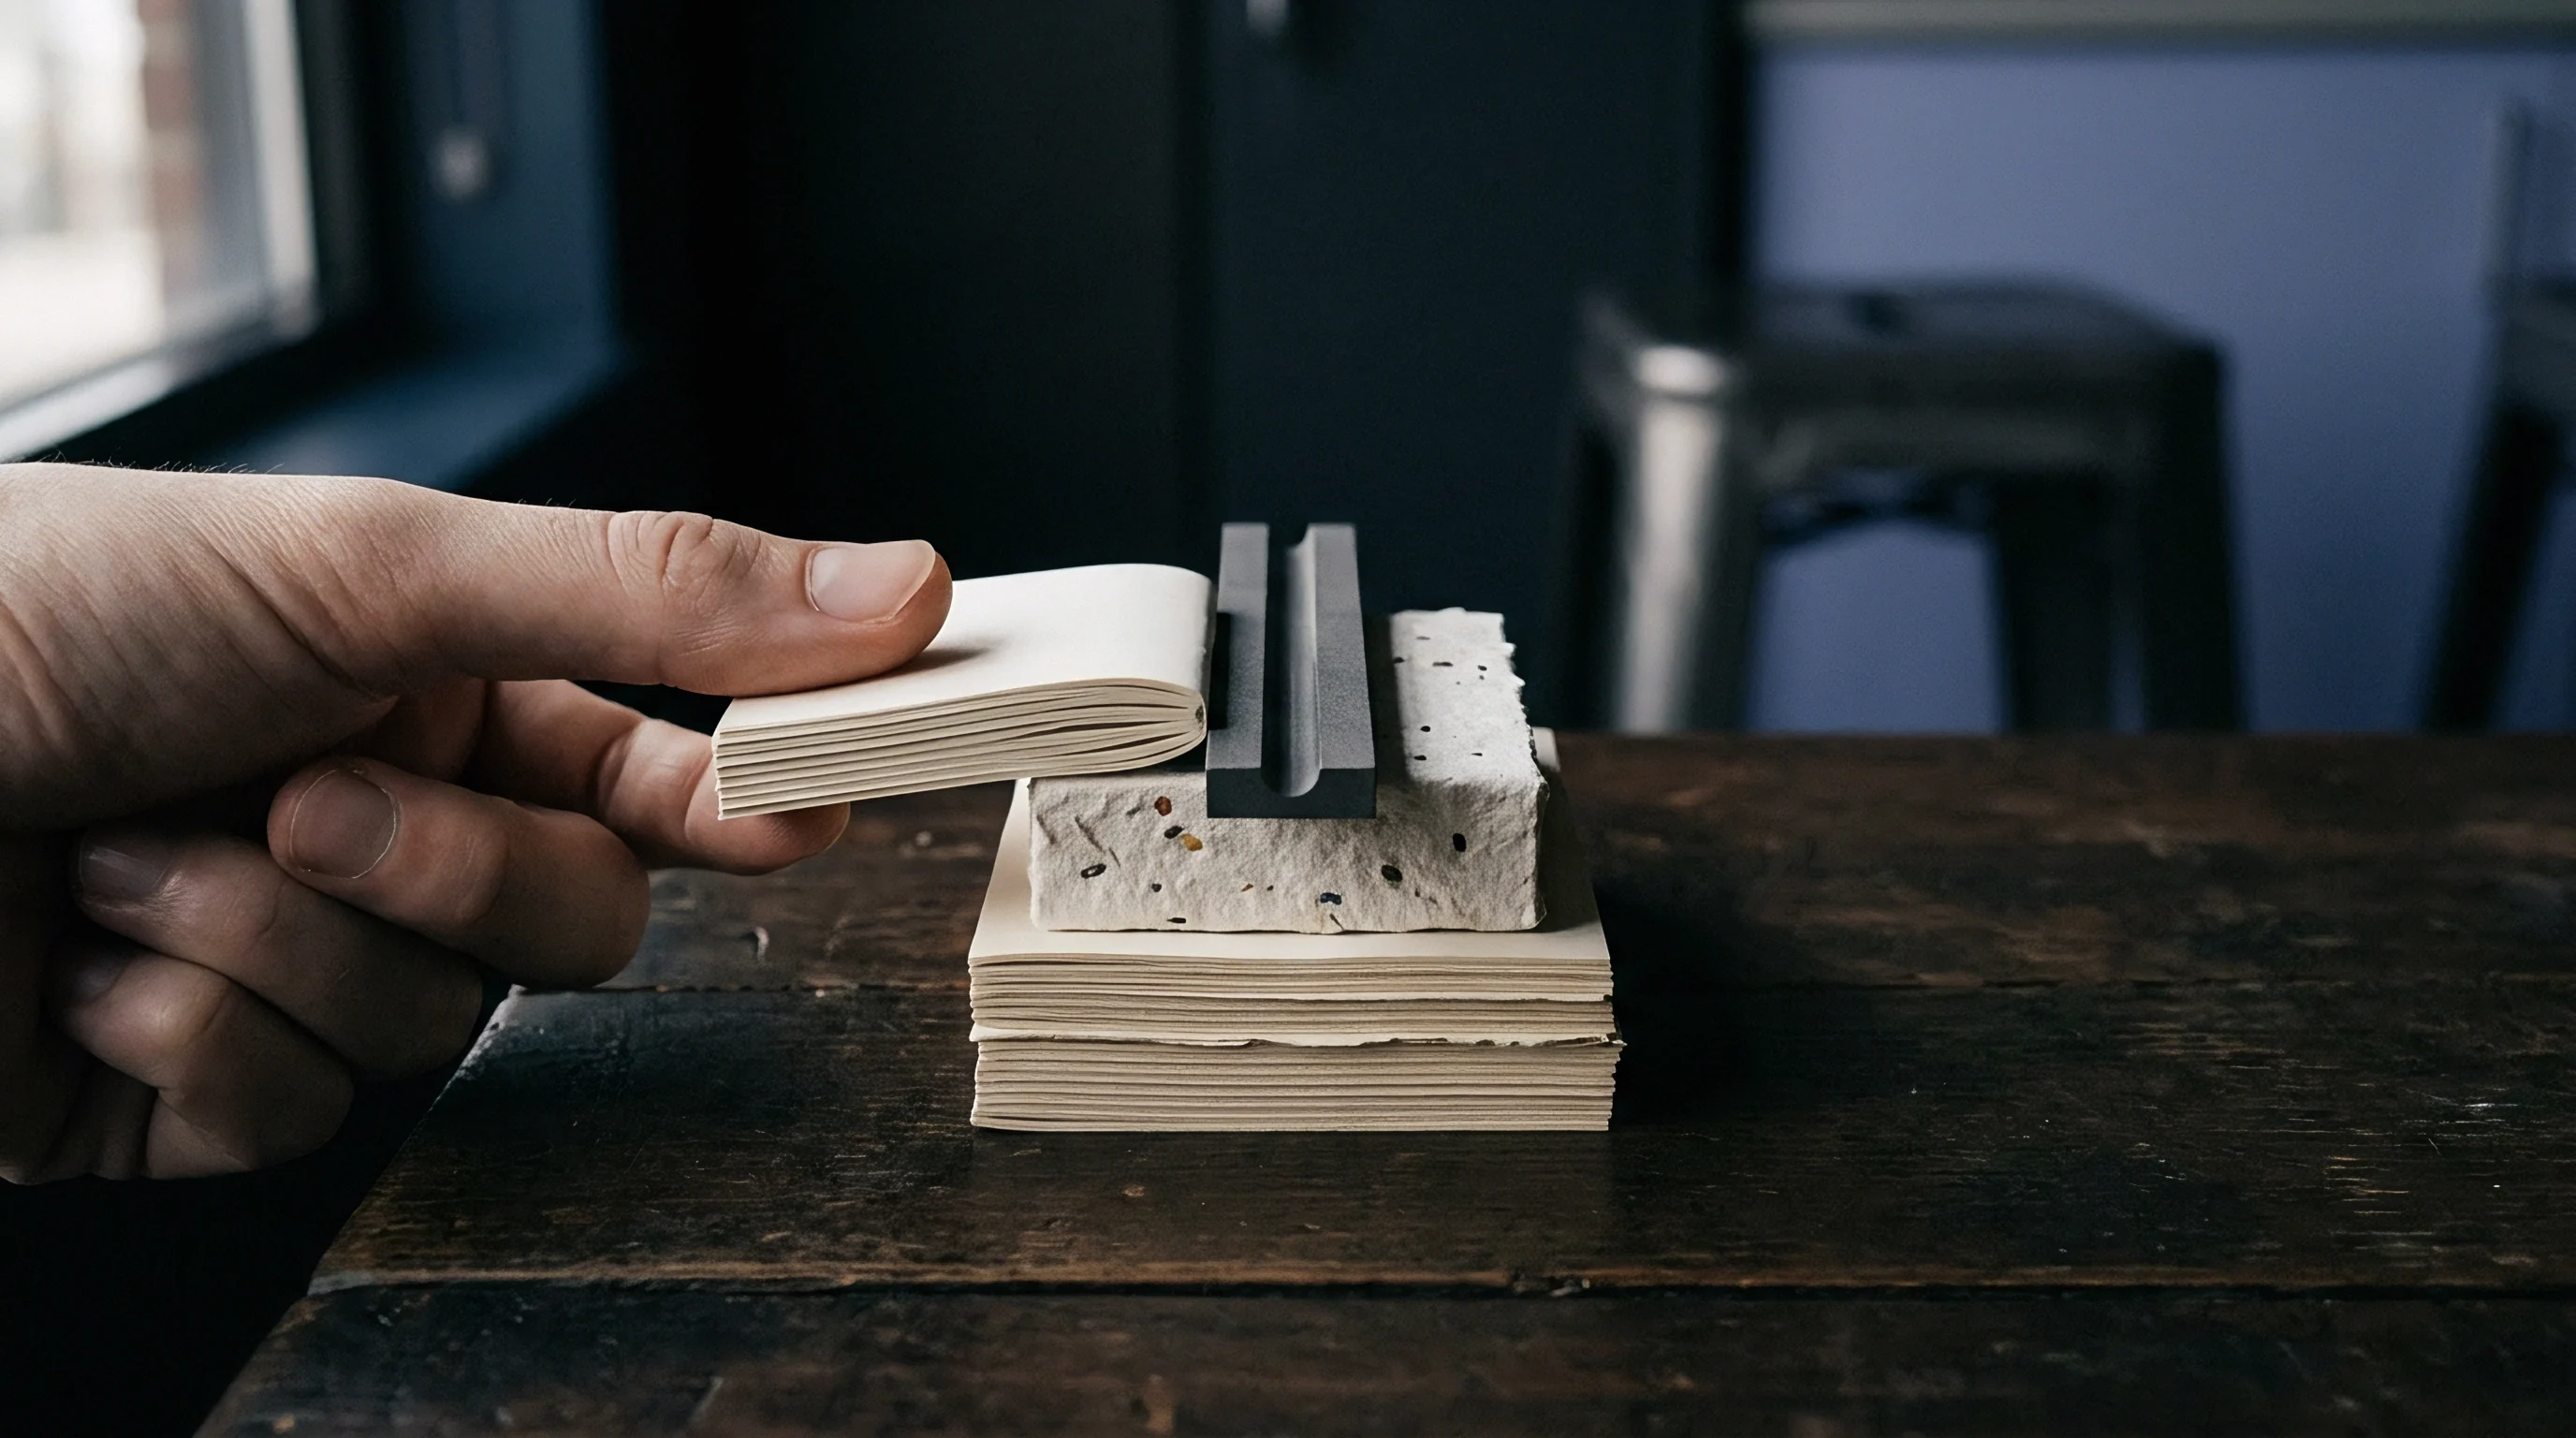
When Does Platen Crease Pressure Exceed Interfacial Strength?
Caliper variations across recycled mill runs complicate die calibration on the press floor. A nominal 450-micrometre recycled chipboard sheet often drifts between 425 and 485 micrometres from reel edge to reel center. Fixed-depth pertinence counters or steel counter plates cannot compensate dynamically for basis-weight drifting during a five-thousand-sheet run.
When heavy caliper board enters a tool configured for nominal thickness, rule penetration exceeds sixty percent of sheet depth. Crushing replaces delamination. The female counter matrix walls pinch the lower plies while shearing the outer liner completely.
| Caliper (µm) | Grammage (g/m2) | Rule Thickness (pt) | Rule Width (mm) | Channel Width (mm) | Channel Depth (µm) |
|---|---|---|---|---|---|
| 350 | 280 | 1.5 | 0.53 | 1.05 | 350 |
| 400 | 320 | 2.0 | 0.71 | 1.31 | 400 |
| 500 | 390 | 2.0 | 0.71 | 1.46 | 500 |
| 600 | 460 | 3.0 | 1.05 | 1.95 | 600 |
Tooling engineers adjust counterplate properties to prevent destructive core displacement.
- Channel chamfering eliminates sharp steel edges that score bottom plies during rule penetration. Bevelled entry angles distribute shear forces outward.
- Pertinax counter calibration aligns die channels within twenty-micrometre positional tolerances. Misaligned grooves create asymmetrical delamination across carton panels.
- Patch tape shimming compensates for platen deflection across large format cutting areas. Micrometre-accurate shimming balances penetration forces across seventy-carton layouts.
Excessive creasing rule penetration fractures surface fibres before internal delamination relieves tension across the hinge.
Consider a run of eighty thousand pharmaceutical cartons stamped on a standard format flatbed press. Tooling technicians shim the cutting chase to accommodate an average board thickness of 400 micrometres. The delivery arrives from a mill using high fractions of mechanical screenings in the filler vat.
Fiber flexibility drops sharply in comparison to chemical pulp mixes. Dynamic shear stress rises above the ultimate shear capacity of the core. As the creasing blade descends, brittle core fibres shatter instead of slipping into discrete plies.
The board displays fractured fold corners immediately after the ninety-degree folder belts. Can adjusted matrix geometry fully compensate for embrittled, multi-recycled municipal furnish without degrading final carton compression stiffness?
Settlement
Commercial claims arising from ply delamination center on whether the fault originated in raw furnish compounding or improper die setup. Sourcing contracts specify basis weight under ISO 536 and caliper under ISO 534 within plus or minus five percent tolerances. Internal bond values rarely appear as binding commercial thresholds unless the buyer insists on their insertion.
When cartons split open on filling lines, converters blame low interply starch adhesion. Board manufacturers inspect recovered carton blanks and attribute the failure to excessive creasing knife penetration or incorrect female matrix channel clearance. Resolving these disputes requires definitive forensic testing of unconverted parent stock retained from the original production lots.
Calculating financial exposure clarifies the stakes behind substrate verification. Take a fifty-tonne order of 380-micrometre uncoated bending chipboard priced at 820 euros per metric tonne delivered. That shipment yields approximately 330,000 finished carton sheets in standard press format.
Converting costs add 450 euros per thousand finished sheets in printing, die-cutting, and folding operations. Rejecting the job at the folder-gluer due to uncontrolled ply cleavage destroys 148,500 euros in converting value against a raw substrate cost of 41,000 euros. The converted carton loss outstrips the substrate price by more than three to one.
Sourcing agreements protect purchasing organizations by inserting strict verification clauses covering mechanical shear properties. A standard warranty line incorporates ISO 16260 minimums of 120 Joules per square metre across all reels, tied to DIN 55437 crease visual rating benchmarks that penalize liner cracking and delamination spread. Inclusion of this contractual clause shifts complete financial liability for converted scrap and press downtime back to the mill whenever retained pallet samples fail verified laboratory shear limits.