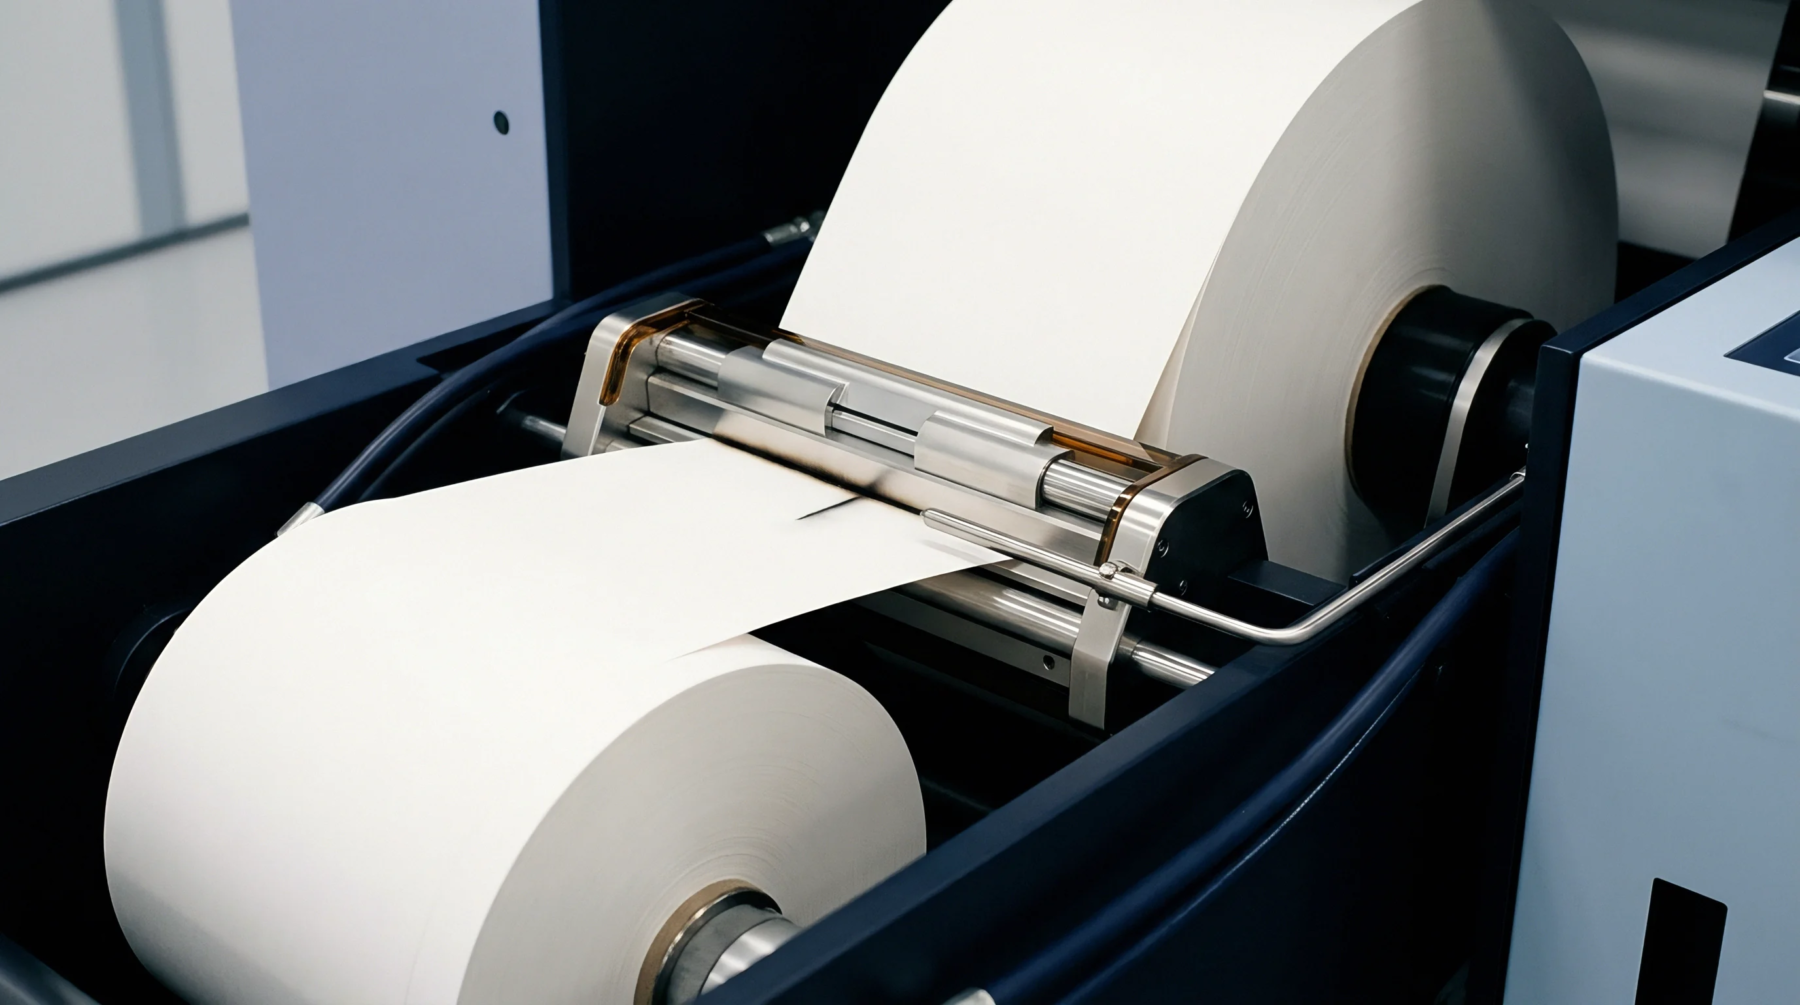
Planning System
Deckle optimization and web format controls align primary papermaking widths with downstream slitting schedules to minimize trim waste. Systematic parent web width management coordinates mill deckle capacities with incoming packaging orders to maximize operational slitter efficiency. Converting operations configure mother roll dimensions to prevent unnecessary cross-direction fiber waste during primary slitting.
Production schedulers assign order combinations that match total parent deckle widths without leaving unusable outer edge strips. Process control systems monitor cross-machine shrinkage from the wet forming wire to dry reel winders.
Deckle Allocation
Papermaking machinery produces master reels whose usable widths vary with fiber furnish compositions, machine speeds and seasonal drying profiles. Effective parent web width management matches incoming customer roll orders to current deckle availability, selecting patterns that leave minimal edge waste. Combining diverse roll sizes onto single master rolls prevents costly edge loss while satisfying diverse boxboard specifications.
Slitting winders adjust edge knives to remove unstable web deckles, delivering smooth outer margins on finished packaging reels. Sophisticated cutting stock algorithms merge customer orders across multiple production runs to avoid low-yield slitting combinations. When trim margins shrink below operational thresholds, web edge flutter risks blade jams or reel break incidents on high-speed winders.
Production planners reallocate orders across alternative paper machines when width schedules produce excessive trim loss. Managing master roll widths minimizes virgin fiber recycling cycles, conserving energy across the papermaking complex.
Operating Limitation
Fixed paper machine deckles restrict width adjustments without structural modifications to slice openings and headbox configurations. Inflexible parent web width management practices cause long order lead times if facilities wait for matching roll widths to fill deckle schedules. Shrinkage variations across differing basis weights cause finished reel widths to drift away from target dimensions.
Mechanical knife count limits on older slitter winders prevent high-density slit combinations, forcing wider edge trim waste. Operations accept minor edge waste losses when tight packaging delivery deadlines prevent optimal pattern consolidation.