Coefficient Friction
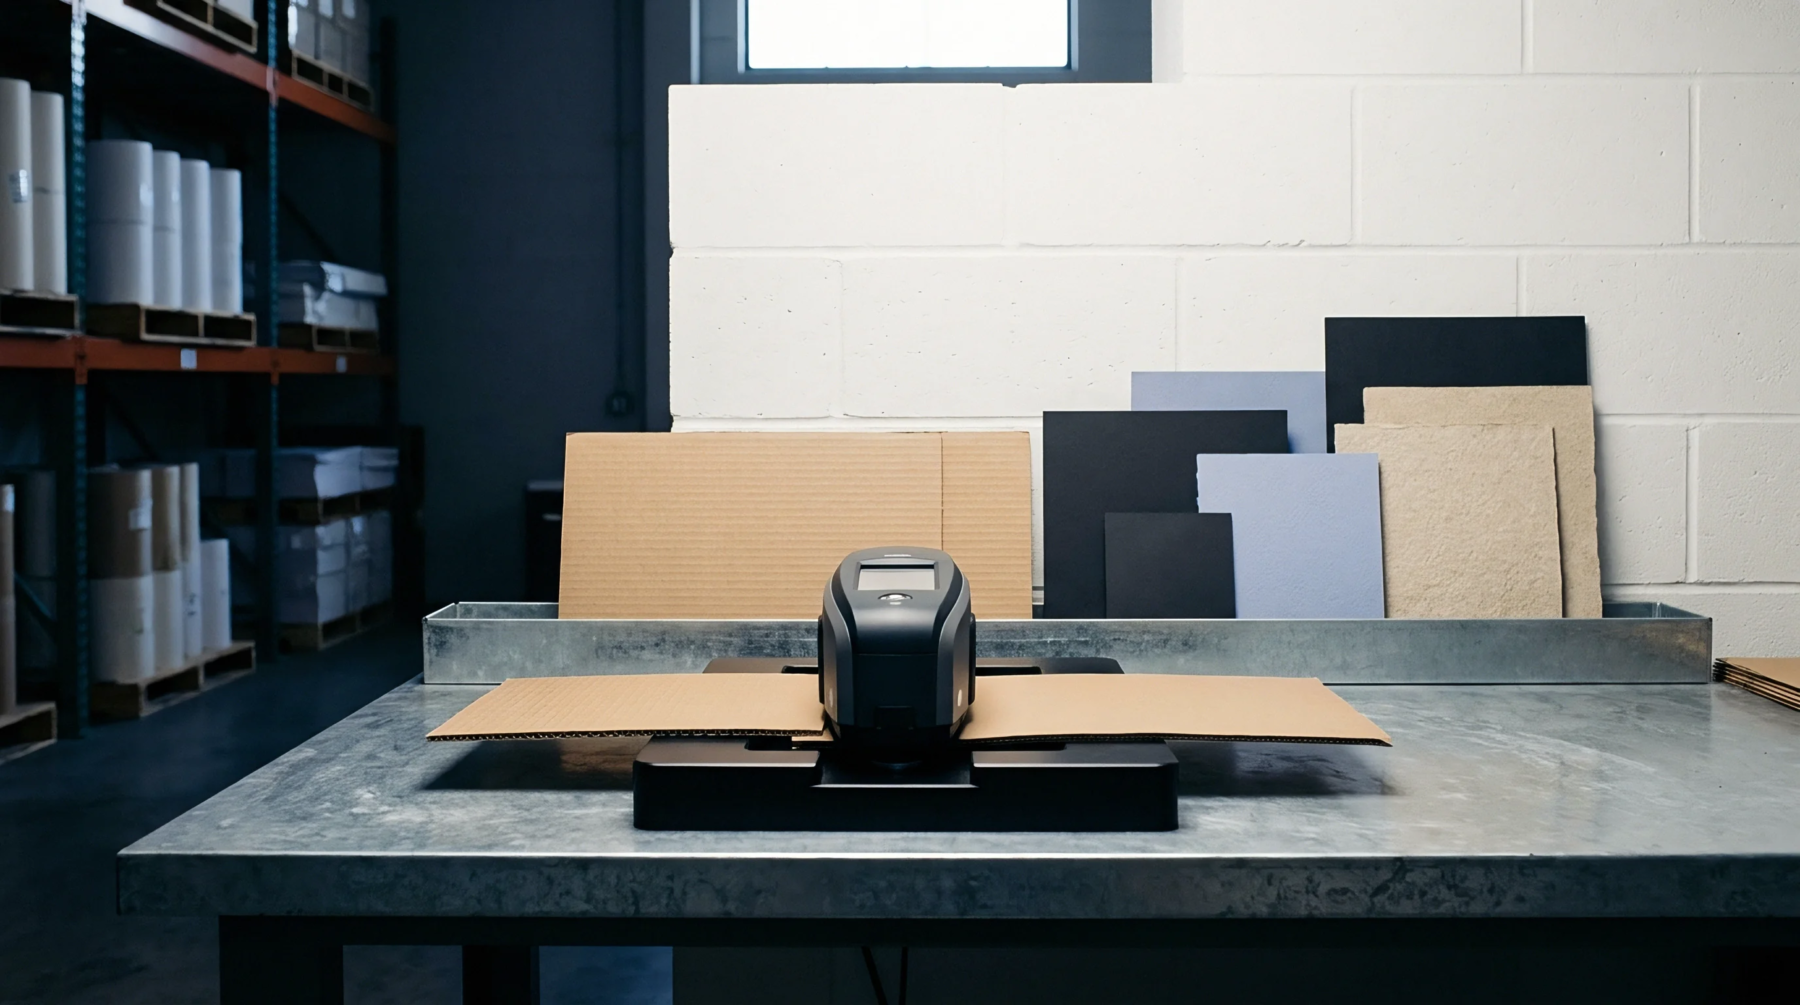
Cohesion and slip resistance on a paper surface are measured by TAPPI T 549, which defines the static and kinetic angles for corrugated containers and folding boxboards. Slated testing sleds are pulled across a horizontal plane to establish the force required to start movement and maintain sliding speed under a constant normal load. Board converters rely on this specification to prevent unstable stacks during palletization and high speed filling operations on automated packaging lines.
Deviations outside the accepted friction window lead directly to carton jams on vacuum feed mechanisms or dangerous load shifts in transit warehouses. The standard stops applying once non paper coatings or specialized wax treatments alter the natural fibre interaction beyond standard calibration limits.
Sliding Mechanics
Gravity exerts a downward force on the weighted metal sled resting on the horizontal substrate while a motor driven winch pulls the assembly at a steady rate. Load cells record the peak force required to overcome initial static adhesion before the sled breaks free and transitions into kinetic motion. Surface roughness and mineral fillers embedded in the sheet topography dictate the actual contact area between the two sliding planes.
Ambient humidity alters this frictional behavior because moisture softens cellulose fibres and increases surface tackiness during the test cycle.
Line Performance
Packaging plants establish strict friction thresholds to guarantee that corrugated boxes do not slide off inclined conveyor belts or tumble during pallet wrapping routines. Automated erecting machinery depends on predictable board interactions so that vacuum suction cups pick single blanks without dragging adjacent sheets from the magazine. Operators adjust calendering pressures at the wet end of the paper machine when laboratory friction values deviate from target tolerances.
Excessive slip causes warehouse instability while excessive drag tears container flaps during high speed folding operations.