Evaluating Wet-End Charge Neutralization and Dewatering Thresholds in BCTMP
Charge neutralization to a negative two millivolt threshold maximizes wet-end drainage and press dryness without sacrificing mechanical pulp sheet bulk.

Extractives
Unmanaged wet-end systems suffer severe drainage penalties from the chemical load intrinsic to bleached chemi-thermomechanical pulp. Alkaline peroxide bleaching releases substantial dissolved and colloidal material into process water, leaving a carryover rich in pectins, galacturonans, fatty acids, resin acids, and sulfonated lignin fragments. While refining virgin kraft fiber generates minimal colloidal matter, high-yield mechanical pulping disperses up to thirty kilograms of organic material per air-dry tonne into solution.
This carryover drives headbox white water anionic charge demand up to 120 to 350 microequivalents per litre. Left unchecked, this anionic trash scavenges cationic wet-end additives before they can promote retention or sizing on wood fibres.
Evaluating the pulp starts with streaming current detection and polyelectrolyte titration against standard polydiallyldimethylammonium chloride at neutral pH. Before chemical treatment, virgin bleached birch or aspen mechanical stock shows a native zeta potential of negative twenty-five to negative thirty-five millivolts. Bringing net charge near the isoelectric boundary ~ between negative five and zero millivolts ~ neutralizes these colloids completely.
Untreated electrokinetic charges leave colloidal spheres suspended between fibres, where they drift into forming fabric voids, plug microscopic drainage channels, and choke off early gravity dewatering.
Streaming current titration under ISO 5360 establishes that unwashed high-yield mechanical pulps demand up to 280 microequivalents of cationic charge per litre to reach the isoelectric point.
Tighter machine water loops sharply elevate cationic demand. Mills running freshwater intake below ten cubic metres per tonne accumulate dissolved solids quickly. The resulting high conductivity compresses the electrical double layer around cellulosic fibres, checking osmotic swelling and stiffening natural fibre conformability.
Once electrolyte levels pass 2500 microsiemens per centimetre, calcium and magnesium ions fight synthetic polyelectrolytes for carboxylate sites along the fibre wall. Responsive polymer retention breaks down, introducing pinholes, sheet two-sidedness, and erratic cross-wire basis weights.
Unneutralized colloidal carryover creates distinct operational failures across the paper machine:
- Anionic trash agglomeration deposits sticky pitch complexes onto forming fabrics, creating pinholes and uncalendered sheet defects during high-speed runs.
- Hydrophobic sizing collapse starves alkyl ketene dimer and alkenyl succinic anhydride molecules of anchoring sites on cellulose fibrils. This sizing decay elevates water absorption values past allowable specification limits.
- Retention aid starvation consumes expensive high-molecular-weight polyacrylamides in the liquid phase before polymer chains can bridge across fibre surfaces.
- White-water foaming traps air bubbles within the stock suspension, generating micro-flocs and cross-direction grammage streaks.
Without neutralization, stock systems drive vacuum elements into extreme negative pressure. Forming fabrics blind rapidly, forcing emergency wash-ups, boil-outs, and premature fabric replacement.
Coagulation
Balancing high-yield stock at the wet end requires a clear dual-polymer program: low-molecular-weight, highly charged coagulants scavenge dissolved colloidal trash before bridging polymers enter the stream. Polyaluminium chloride, polyamines, and polyDADMAC act as primary scavengers. Introducing a high charge density coagulant with an intrinsic viscosity between 0.1 and 0.5 decilitres per gram forces dissolved wood polymers onto fibre surfaces.
This targeted deposition neutralizes steric repulsion without forming the coarse flocs that ruin sheet formation, leveraging small spatial geometries to condition the furnish for subsequent polymer bridging.
Where Do Anionic Trash Colloids Settle?
Precipitated colloids cling to high-surface-area fines rather than long tracheid fibres. Mechanical pulps carry twenty-five to forty percent fines that pass a two-hundred-mesh Bauer-McNett screen, and these fines hold over three times the specific surface charge of long fibres per dry mass unit. Dosing coagulants at the thick-stock or blend chest provides 45 to 90 seconds of dwell time, binding colloidal complexes to fines before approach piping dilution.
Downstream of machine screens, secondary additions of high-molecular-weight cationic polyacrylamide form controlled micro-flocs through patch and bridging action.
| Coagulant Chemistry | Molecular Weight (Da) | Charge Density (meq/g) | Specific Dose (kg/t dry) | Headbox Turbidity (NTU) | Zeta Potential (mV) |
|---|---|---|---|---|---|
| Polyaluminium Chloride (18% Al2O3) | 500 to 1,500 | 5.2 | 2.50 to 4.20 | 42 to 58 | -6.2 to -2.1 |
| PolyDADMAC (Liquid Aqueous) | 100,000 to 250,000 | 6.8 | 0.80 to 1.60 | 24 to 36 | -4.5 to +0.8 |
| Polyethyleneimine (Modified Branched) | 500,000 to 1,200,000 | 9.5 | 0.50 to 1.10 | 18 to 28 | -2.8 to +1.5 |
| Polyamine (Epichlorohydrin-DMA) | 20,000 to 75,000 | 7.2 | 1.10 to 2.20 | 31 to 46 | -5.0 to -1.2 |
Over-neutralizing past zero into positive charge destabilizes process control. Excess polymer builds positive repulsive charges that disperse fibres, undoing initial dewatering gains. Chemical qualification follows a four-step sequence:
- Thick stock charge titration establishes the baseline cationic demand of the untreated mechanical pulp suspension before chemical addition.
- Coagulant screening jar testing identifies the minimum chemical dose required to shift supernatant zeta potential into the negative four to negative two millivolt band without overshooting. High dosages increase chemistry costs.
- Flocculant bridging optimization measures drainage velocity in a dynamic drainage jar to verify that flocculation avoids fiber clumping. Sheet formation suffers if micro-flocs grow beyond two millimetres in diameter.
- Microparticle addition calibration balances colloidal silica or bentonite dosage to re-flocculate shear-broken polymers and clear the white-water phase.
Coagulant overdosing shifts furnish charge into net positive territory and disperses fibres as aggressively as unneutralized anionic trash.
Higher coagulant additions do not guarantee cleaner process loops when raw furnish quality varies.
Wire
Forming table dewatering governs both machine speed and final board bulk. Bleached chemi-thermomechanical pulp drains slower under initial gravity than chemical kraft pulp of equivalent freeness because rigid lignin stops mechanical fibres from lying flat, yielding a porous yet tortuous filter cake. Canadian Standard Freeness under ISO 5267-2 typically runs 300 to 450 millilitres for middle-ply board grades.
As micro-fines wash from the web interior toward the wire under suction, they seal the bottom of the mat ~ a localized drainage barrier known as wire blinding.
Pulp drainage responds non-linearly to furnish charge and hydrodynamic shear. Bringing wet-end charge into the negative four to negative two millivolt window noticeably accelerates forming table drainage. On modern multi-ply board formers, gravity elements handle up to sixty percent of total water removal.
Neutralized stock lets the dry line move back toward the headbox, widening the effective drainage window before vacuum boxes take over. Unneutralized stock pushes the dry line toward the couch roll, cutting off high-vacuum flatbox efficiency.
A wet line advancing toward the couch roll indicates severe drainage retardation and impending sheet crushing in the press nip.
Charge states directly alter vacuum response and water removal across the forming wire:
| Furnish Charge State | Gravity Table Water Removal (%) | Foil Box Vacuum (kPa) | High-Vacuum Flatbox (kPa) | Dry Line Position from Slice (m) | Couch Roll Solids Content (%) |
|---|---|---|---|---|---|
| Untreated (Negative 24 mV) | 46.2 | 8.5 | 38.0 | 14.8 | 17.4 |
| Under-Coagulated (Negative 12 mV) | 52.8 | 7.2 | 32.5 | 12.4 | 19.1 |
| Neutralized (Negative 2 mV) | 61.5 | 5.4 | 24.0 | 9.6 | 22.8 |
| Over-Cationized (Positive 8 mV) | 49.1 | 8.0 | 36.0 | 13.7 | 18.2 |
Stock temperature controls white-water viscosity and fluid flow through the mat. Running between 48 and 54 degrees Celsius drops water viscosity by over twenty percent relative to ambient room conditions, speeding up interstitial water release. Mechanical fibres maintain wet-web stiffness at these higher temperatures, holding their structure under low vacuum.
Foil angles set between one and two degrees generate alternating pressure-suction pulses that fluidize the wet mat, clearing trapped fines and opening drainage channels.
Bentonite and colloidal silica microparticles provide critical structure late in gravity dewatering. Dosed just ahead of the headbox or after the last fan pump, these nanoparticles present surface areas above five hundred square metres per gram. Strongly anionic silica particles lock onto cationic polymer patches across neighboring fibres, pulling sprawling polymer loops tight and releasing bound vicinal water into the bulk stream.
The resulting micro-flocs resist shear, maintaining open drainage paths straight into the high-vacuum zone.
Fast gravity drainage preserves the open structural network required for high bulk in converted packaging board.
Nip
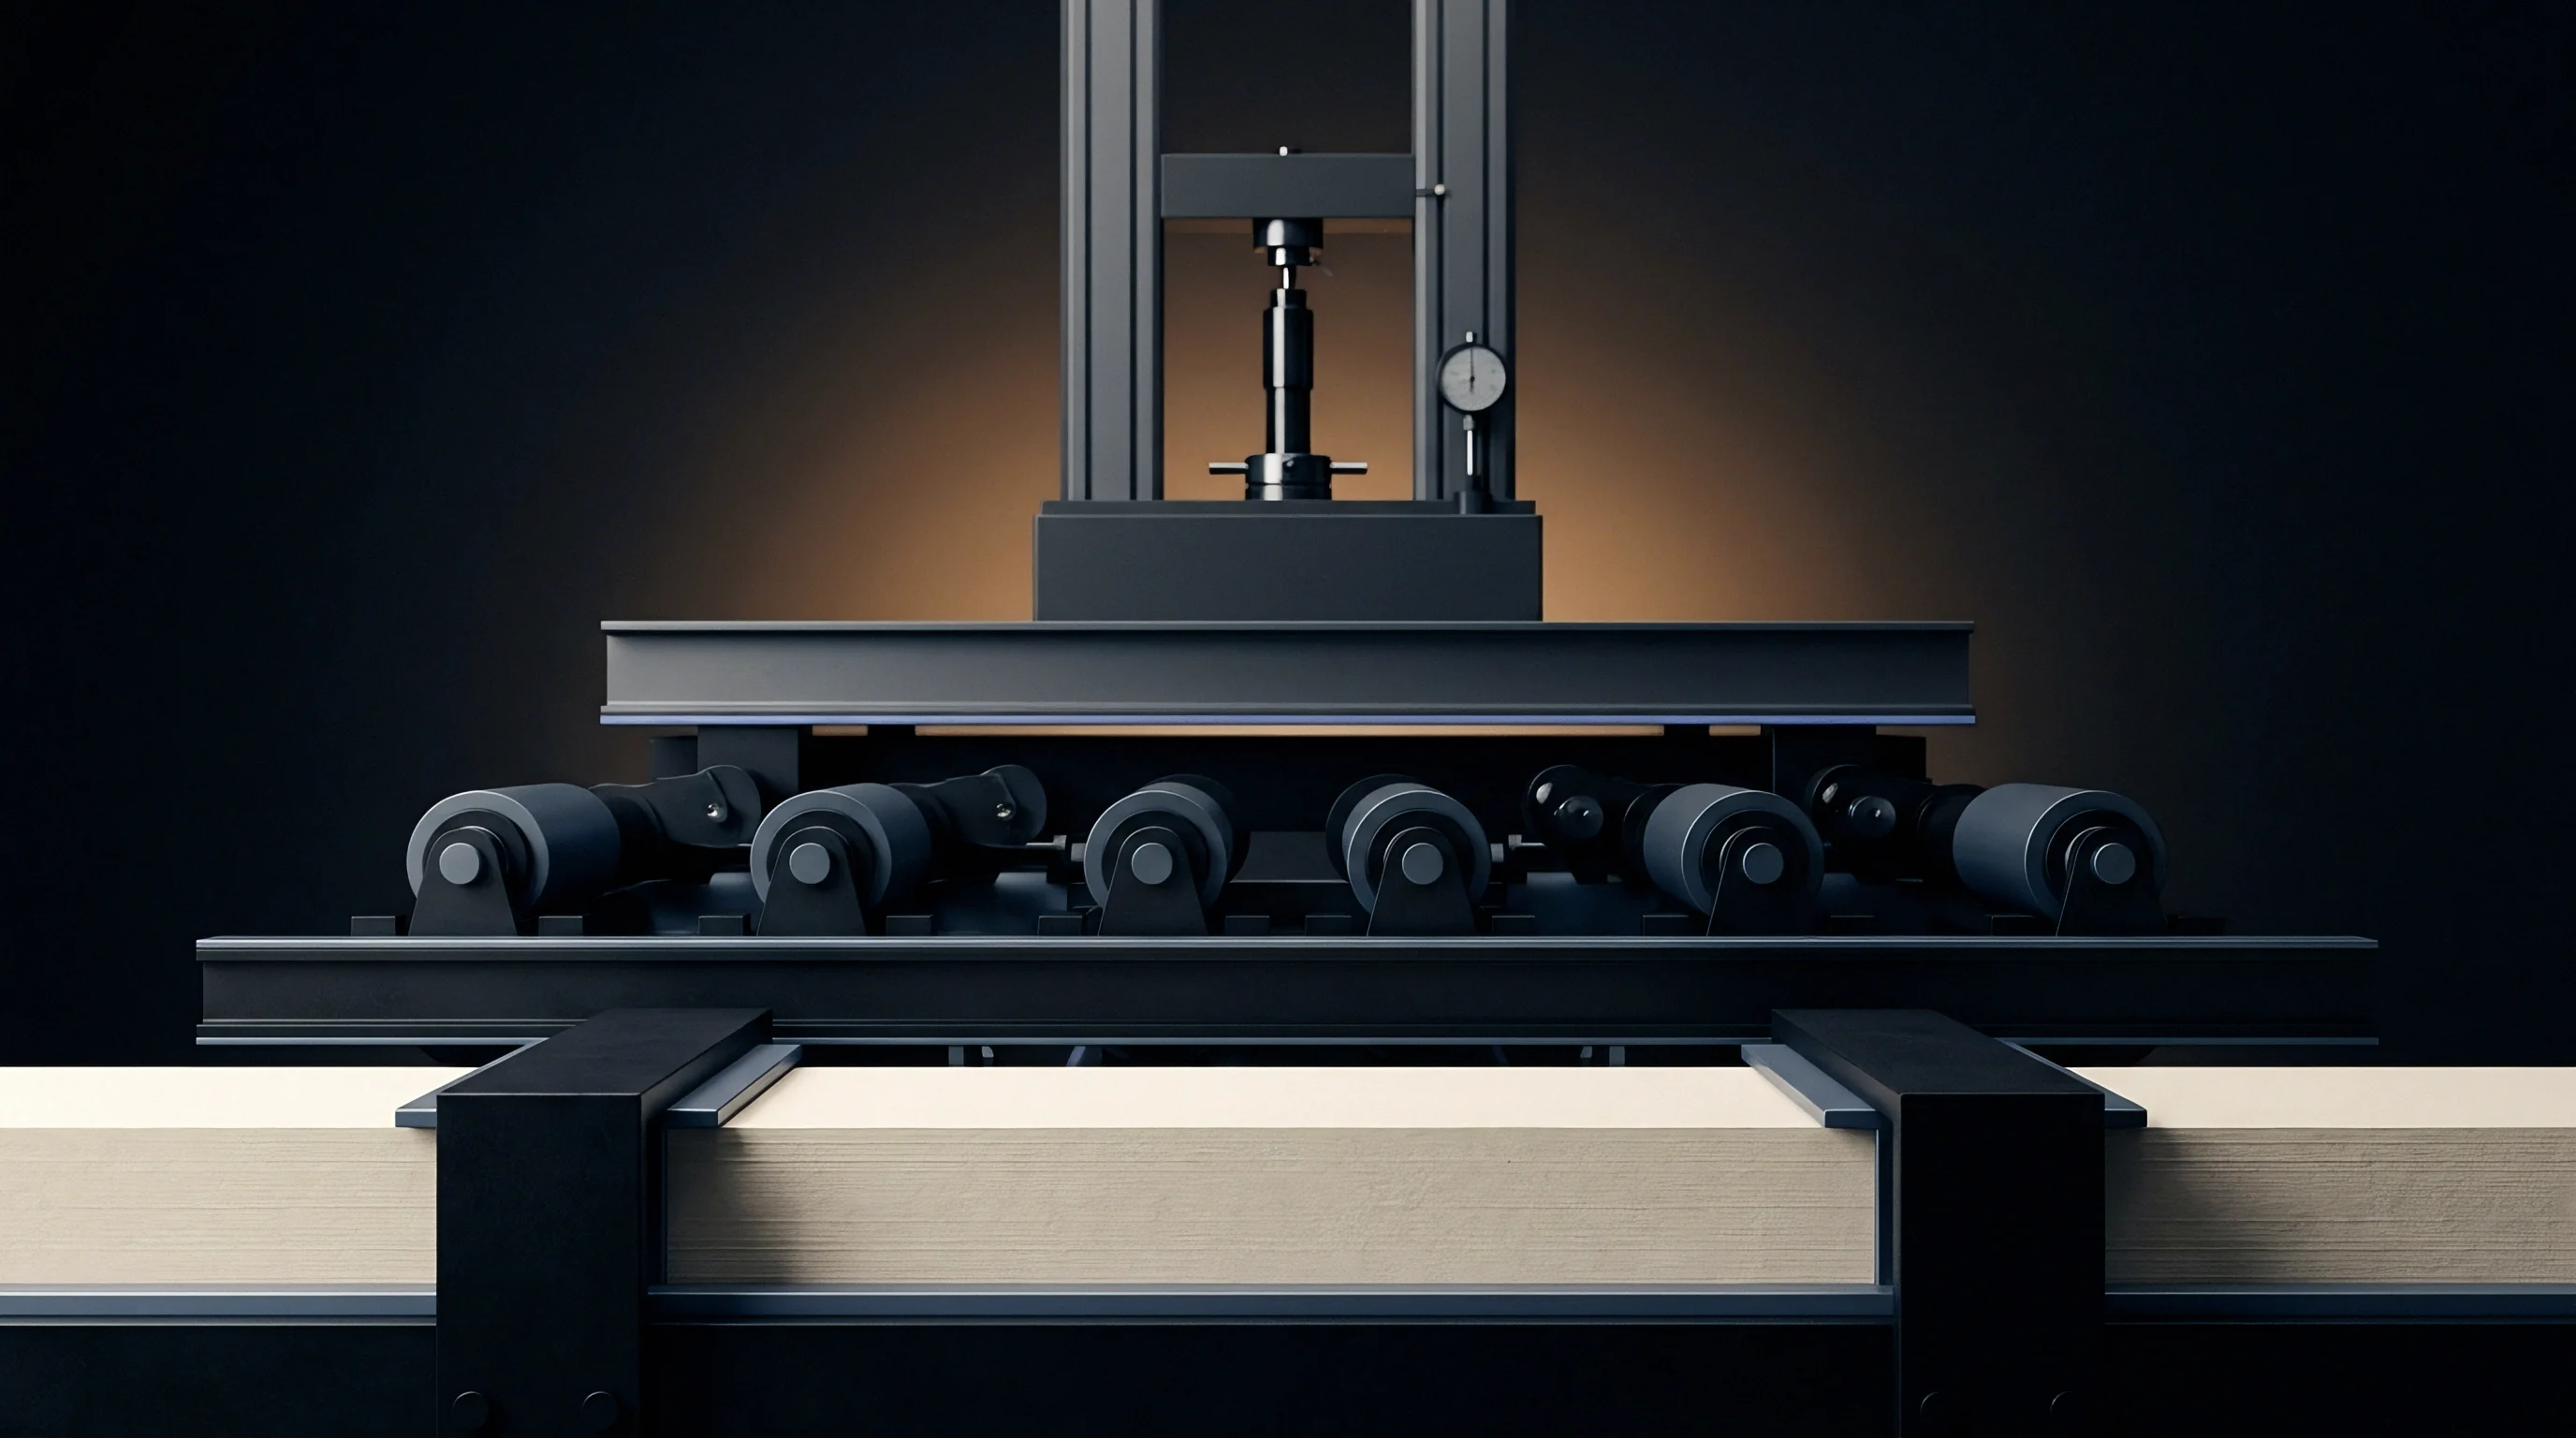
Pressing is the last mechanical chance to remove water before expensive thermal drying. High-yield fibres offer far better bulk and bending stiffness than kraft, but long loading times will deform them. Pressing bleached chemi-thermomechanical stock means balancing maximum water removal against target caliper.
Modern shoe presses use wide 250 to 300 millimetre machine-direction pressure profiles, keeping peak pressure under six megapascals while extending dwell times past thirty milliseconds. This prolonged nip lets internal fibre-wall hydraulic pressure bleed off gradually, preventing structural crush.
Should Chemical Addition Shift before Couch Vacuum?
Couch roll solids dictate whether the wet web survives initial press consolidation without delaminating. Entering the press under twenty percent dryness locks excess free water in the core, where nip compression turns it into explosive hydraulic back-pressure that breaks internal fibre bonds. Correcting upstream charge brings couch roll discharge solids to twenty-two to twenty-four percent.
The resulting wet-web tensile strength lets open draws run between wire and press felts without sheet flutter or edge cracks.
Press section dewatering depends directly on the wet-end charge state built on the wire:
| Wet-End Treatment Condition | Press Inlet Solids (%) | Press Exit Solids (%) | Sheet Caliper (µm) | Apparent Bulk (cm³/g) | Internal Bond Strength (J/m²) |
|---|---|---|---|---|---|
| Unneutralized Raw Pulp | 17.8 | 40.2 | 435 | 1.55 | 142 |
| PolyDADMAC Coagulated | 20.4 | 43.1 | 462 | 1.65 | 178 |
| Coagulant + CPAM + Silica | 22.9 | 45.8 | 488 | 1.74 | 215 |
| Over-Cationized Excess PolyDADMAC | 18.5 | 41.4 | 440 | 1.57 | 155 |
Mechanical fibre stiffness resists compression, maintaining sheet porosity under moderate loads. Bleached chemi-thermomechanical pulp contains over twenty percent residual lignin by weight, a natural cross-linked polymer with a saturated glass transition temperature near 115 degrees Celsius. Keeping press temperatures below 65 degrees Celsius holds lignin in its glassy state.
As the sheet leaves the shoe press nip, mechanical fibres rebound elastically, retaining open lumens and porous networks. That resilience preserves the specific bulk that dictates folding boxboard bending stiffness during die-cutting.
Rigorous operational protocols govern wet-end stability evaluations during full-scale packaging runs:
- Zeta potential tolerance verification monitors headbox furnish between negative four and negative one millivolts through continuous streaming current measurements. Variations outside this band degrade dewatering consistency.
- Press fabric permeability logging tracks felt void volume across operating cycles using portable high-pressure air permeameters. Deposited extractives blind felts rapidly.
- Caliper drift audit correlates reel thickness against drying cylinder steam consumption to verify that dewatering gains avoid sheet compaction.
- Couch vacuum sensitivity profiling establishes minimum operating suction levels required to prevent wet-web edge curling before press pick-up.
Target bulk specifications dictate pressing limits regardless of available machine hydraulic capacity.
How surface-active pitch components alter felt compaction rates over long production runs remains an open question in mill operations.
Throughput
Dryer section evaporation is the most expensive thermal operation in the mill. Vaporizing each kilogram of water entering the dryer cans consumes 1.2 to 1.5 kilograms of low-pressure steam. Raising press exit dryness from 41 percent to 45 percent through charge neutralization strips 0.28 kilograms of water per kilogram of dry fiber before thermal drying even begins.
That cuts specific steam use by fourteen percent, unbottlenecking steam-limited machines while supplying converting plants with board that shows flatter moisture profiles, uniform stiffness, and less curl.
The financial impact of charge neutralization shows clearly on a machine producing 150,000 tonnes per year of 300 g/m² folding boxboard:
An unneutralized baseline run yields 41.5 percent press exit dryness at 480 metres per minute. Evaporation consumes 1.35 tonnes of steam per tonne of removed water, with steam priced at 32 dollars per tonne. At 41.5 percent dryness, the dryers must remove 1.41 tonnes of water per tonne of dry board, bringing thermal drying costs to 60.91 dollars per dry tonne.
Dosing 1.2 kilograms of polyDADMAC and 0.25 kilograms of colloidal silica per tonne adds 4.80 dollars per dry tonne in chemical cost. In return, the dual-polymer treatment accelerates drainage and raises press exit solids to 45.2 percent. Water entering the dryers drops to 1.21 tonnes per tonne of dry board, cutting steam demand to 1.63 tonnes per tonne of board and driving thermal drying costs down to 52.27 dollars per tonne.
After accounting for chemical costs, net savings equal 3.84 dollars per tonne ~ adding 576,000 dollars directly to operating margin on a 150,000-tonne annual run.
Machine speed often responds immediately to wet-end charge control. Reducing the evaporative water load on drying-limited lines lets operators increase speed without raising steam header pressure. When press solids exceed forty-four percent, speed gains of six to nine percent are routine.
Higher output lowers fixed conversion costs per packaging tonne while preserving caliper per grammage unit, as shorter cylinder residence times reduce evaporative shrinkage.
Middle plies for folding boxboard face strict physical and chemical specs, including certified sheet stability under standard conditions. Under ISO 187 guidelines (23 degrees Celsius and 50 percent relative humidity), delivered mechanical board lots must hold cross-web thickness variation below three percent. Delivering that level of dimensional stability requires balanced colloidal charges, uniform dewatering, and caliper control from the forming wire through to the winder.
Contracts specifying reel moisture variations tighter than plus or minus 0.5 percent leave mills no choice but to run automated wet-end streaming current controls.