Selecting Crease Rule Geometry for Recycled Board Grades
Recycled board demands matrix channels widened to rule thickness plus 1.7 to 1.9 times caliper to induce core delamination and prevent liner splitting.
Furnish
Fibre Morphology across Recycled Paperboard Grades
A digital micrometer applying 50 kPa of static pressure per ISO 534 registers 450 micrometres on a sheet of folding boxboard and returns an identical caliper on a sheet of coated recycled board. The two sheets behave differently under the impact of a steel rule. Virgin furnish retains long cellulose chains with intact fibrils that slip, delaminate internally, and stretch across the outer crease bead.
Recycled furnish contains shortened fibres with low hornified swelling capability, high ash fractions, and reduced inter-fibre hydrogen bonding. The mechanical response shifts from elastic plastic redistribution toward brittle shear failure under identical strain.
Recycled containerboard and cartonboard grades such as white lined chipboard, coated recycled board, and testliner grades carry significant portions of mechanical pulp, deinked pulp, and mineral fillers. Recycled fibres display reduced water retention values, lower tensile energy absorption according to ISO 1924-2, and diminished out-of-plane z-directional tensile strength per ISO 15754. Virgin kraft pulps allow broad creasing windows because individual fibres can yield without severing.
Recycled fibres snap when tensile strains across the score exceed three percent.
The manufacturing architecture of multi-ply recycled board introduces further complications for the converting floor. The outer plies usually consist of bleached chemical pulp or sorted deinked office waste, whereas the bulky middle plies consist of mixed waste paper, mechanical screen rejects, and calcium carbonate or clay fillers. Mineral fillers lower the raw material expenditure while stabilizing surface flatness, yet they offer zero fibrous consolidation.
Stresses concentrated by a blunt creasing tool cause the core to crumble instead of delaminating into uniform, controlled hinge sheets.
A recycled furnish conditioned under ISO 187 at 23 degrees Celsius and 50 percent relative humidity exhibits 25 to 40 percent lower tensile energy absorption than virgin bleached board of matching basis weight.
The ratio of machine direction to cross direction tensile stiffness introduces another structural constraint. Cross direction scores bend across predominantly aligned fibres, forcing the rule to fracture fibre walls rather than roll them into the channel. Machine direction scores run parallel to the primary fibre alignment, causing the sheet to split down the grain if channel clearance pinches the stock.
The converter manages these anisotropic differences through dedicated adjustments to the tooling layout rather than running uniform virgin rules across every carton panel.
The visual distinction between virgin cartonboard and recycled chipboard becomes obvious once the sheet splits along the crease channel during 180-degree pre-breaking. Virgin plies separate into clean, paper-thin laminations that maintain liner integrity across the outer profile. Recycled plies break apart into dry granular fragments, dropping fine debris directly into the die-cutting chase and generating jagged cracks along printed ink films.
Tooling parameters designed for virgin substrates fail when transferred to recycled lots without modification.
The converting manager discovers the furnish mismatch when scores split on the gluer belt, leaving high-speed packaging lines jammed with ruptured cartons.
Matrix
Channel Clearance Formulation
Counter dies and creasing matrix systems determine the female channel into which the steel creasing rule forces the cartonboard. Standard converting formulas for solid bleached sulphate calculate channel width as the rule thickness plus 1.5 times the board caliper. Applying that virgin equation to multi-ply coated recycled board produces crushed linerboards, fractured score lines, and catastrophic ink flaking.
Recycled board requires wider female channels to clear the bulkier, stiffer internal plies that refuse to compress cleanly into the matrix.
The engineering formula for calculating matrix channel width on recycled paperboard grades relies on an increased expansion factor:
Matrix Width = Rule Thickness + (Board Caliper Crease Factor)
For standard solid bleached board, the crease factor sits at 1.50. For white lined chipboard and coated recycled board grades spanning 350 to 600 micrometres, the crease factor increases to a band between 1.70 and 1.90. Heavy testliner plies and recycled boards containing ash contents exceeding 15 percent by weight demand factors as high as 2.00.
Omitting this additional clearance forces the substrate against the sharp steel edges of the counter channel, cutting the outer linerboard before folding occurs.
Matrix channel depth governs the penetration distance of the rule and the resulting hinge profile. Standard practice sets channel depth equal to the measured board caliper under 50 kPa platen pressure. On heavily recycled boards, matching depth strictly to caliper frequently results in inadequate bead formation and high folding resistance.
Setting the matrix depth five to ten percent shallower than caliper forces greater out-of-plane shear into the middle plies, inducing the internal delamination necessary to produce a flexible score line.
| Board Caliper (micrometres) | Basis Weight (grams per square metre) | Rule Thickness (Point Size) | Rule Thickness (millimetres) | Matrix Channel Depth (millimetres) | Matrix Channel Width (millimetres) |
|---|---|---|---|---|---|
| 350 | 280 | 2 Pt | 0.71 | 0.35 | 1.30 |
| 400 | 320 | 2 Pt | 0.71 | 0.40 | 1.40 |
| 450 | 360 | 2 Pt | 0.71 | 0.45 | 1.50 |
| 500 | 400 | 3 Pt | 1.05 | 0.50 | 1.90 |
| 550 | 440 | 3 Pt | 1.05 | 0.50 | 2.00 |
| 600 | 480 | 3 Pt | 1.05 | 0.60 | 2.20 |
| 700 | 550 | 4 Pt | 1.42 | 0.70 | 2.70 |
Perturbations across Caliper Drift
Basis weight variations across recycled production runs create substantial converting hazards. A recycled mill running mixed waste furnish operates with basis-weight tolerances of plus or minus five percent, alongside caliper spreads running plus or minus seven percent across the parent reel web. When a die is prepared using a fixed steel matrix milled for nominal 450 micrometre board, delivered stock drifting to 485 micrometres experiences extreme pinching.
The sheet pinches between the rule flanks and channel walls, increasing the required tonnage and severing the coated face.
Converters processing wide-tolerance recycled stock choose between standard phenolic matrix strips and milled steel counter plates. Phenolic systems offer rapid installation and localized adjustment, allowing die-makers to swap matrix strips if a delivered batch runs heavy. Milled steel plates ensure dimensional stability over runs of several hundred thousand impressions, but they eliminate on-press width adjustments.
A delivery of out-of-spec board on a dedicated steel counter run forces press operators to raise impression tonnage, accelerating tool wear without curing the split scores.
A supplier can always point to nominal grammage on the certificate when delivered caliper drifts outside the converting window.
Profile
Steel Rule Edge Geometries
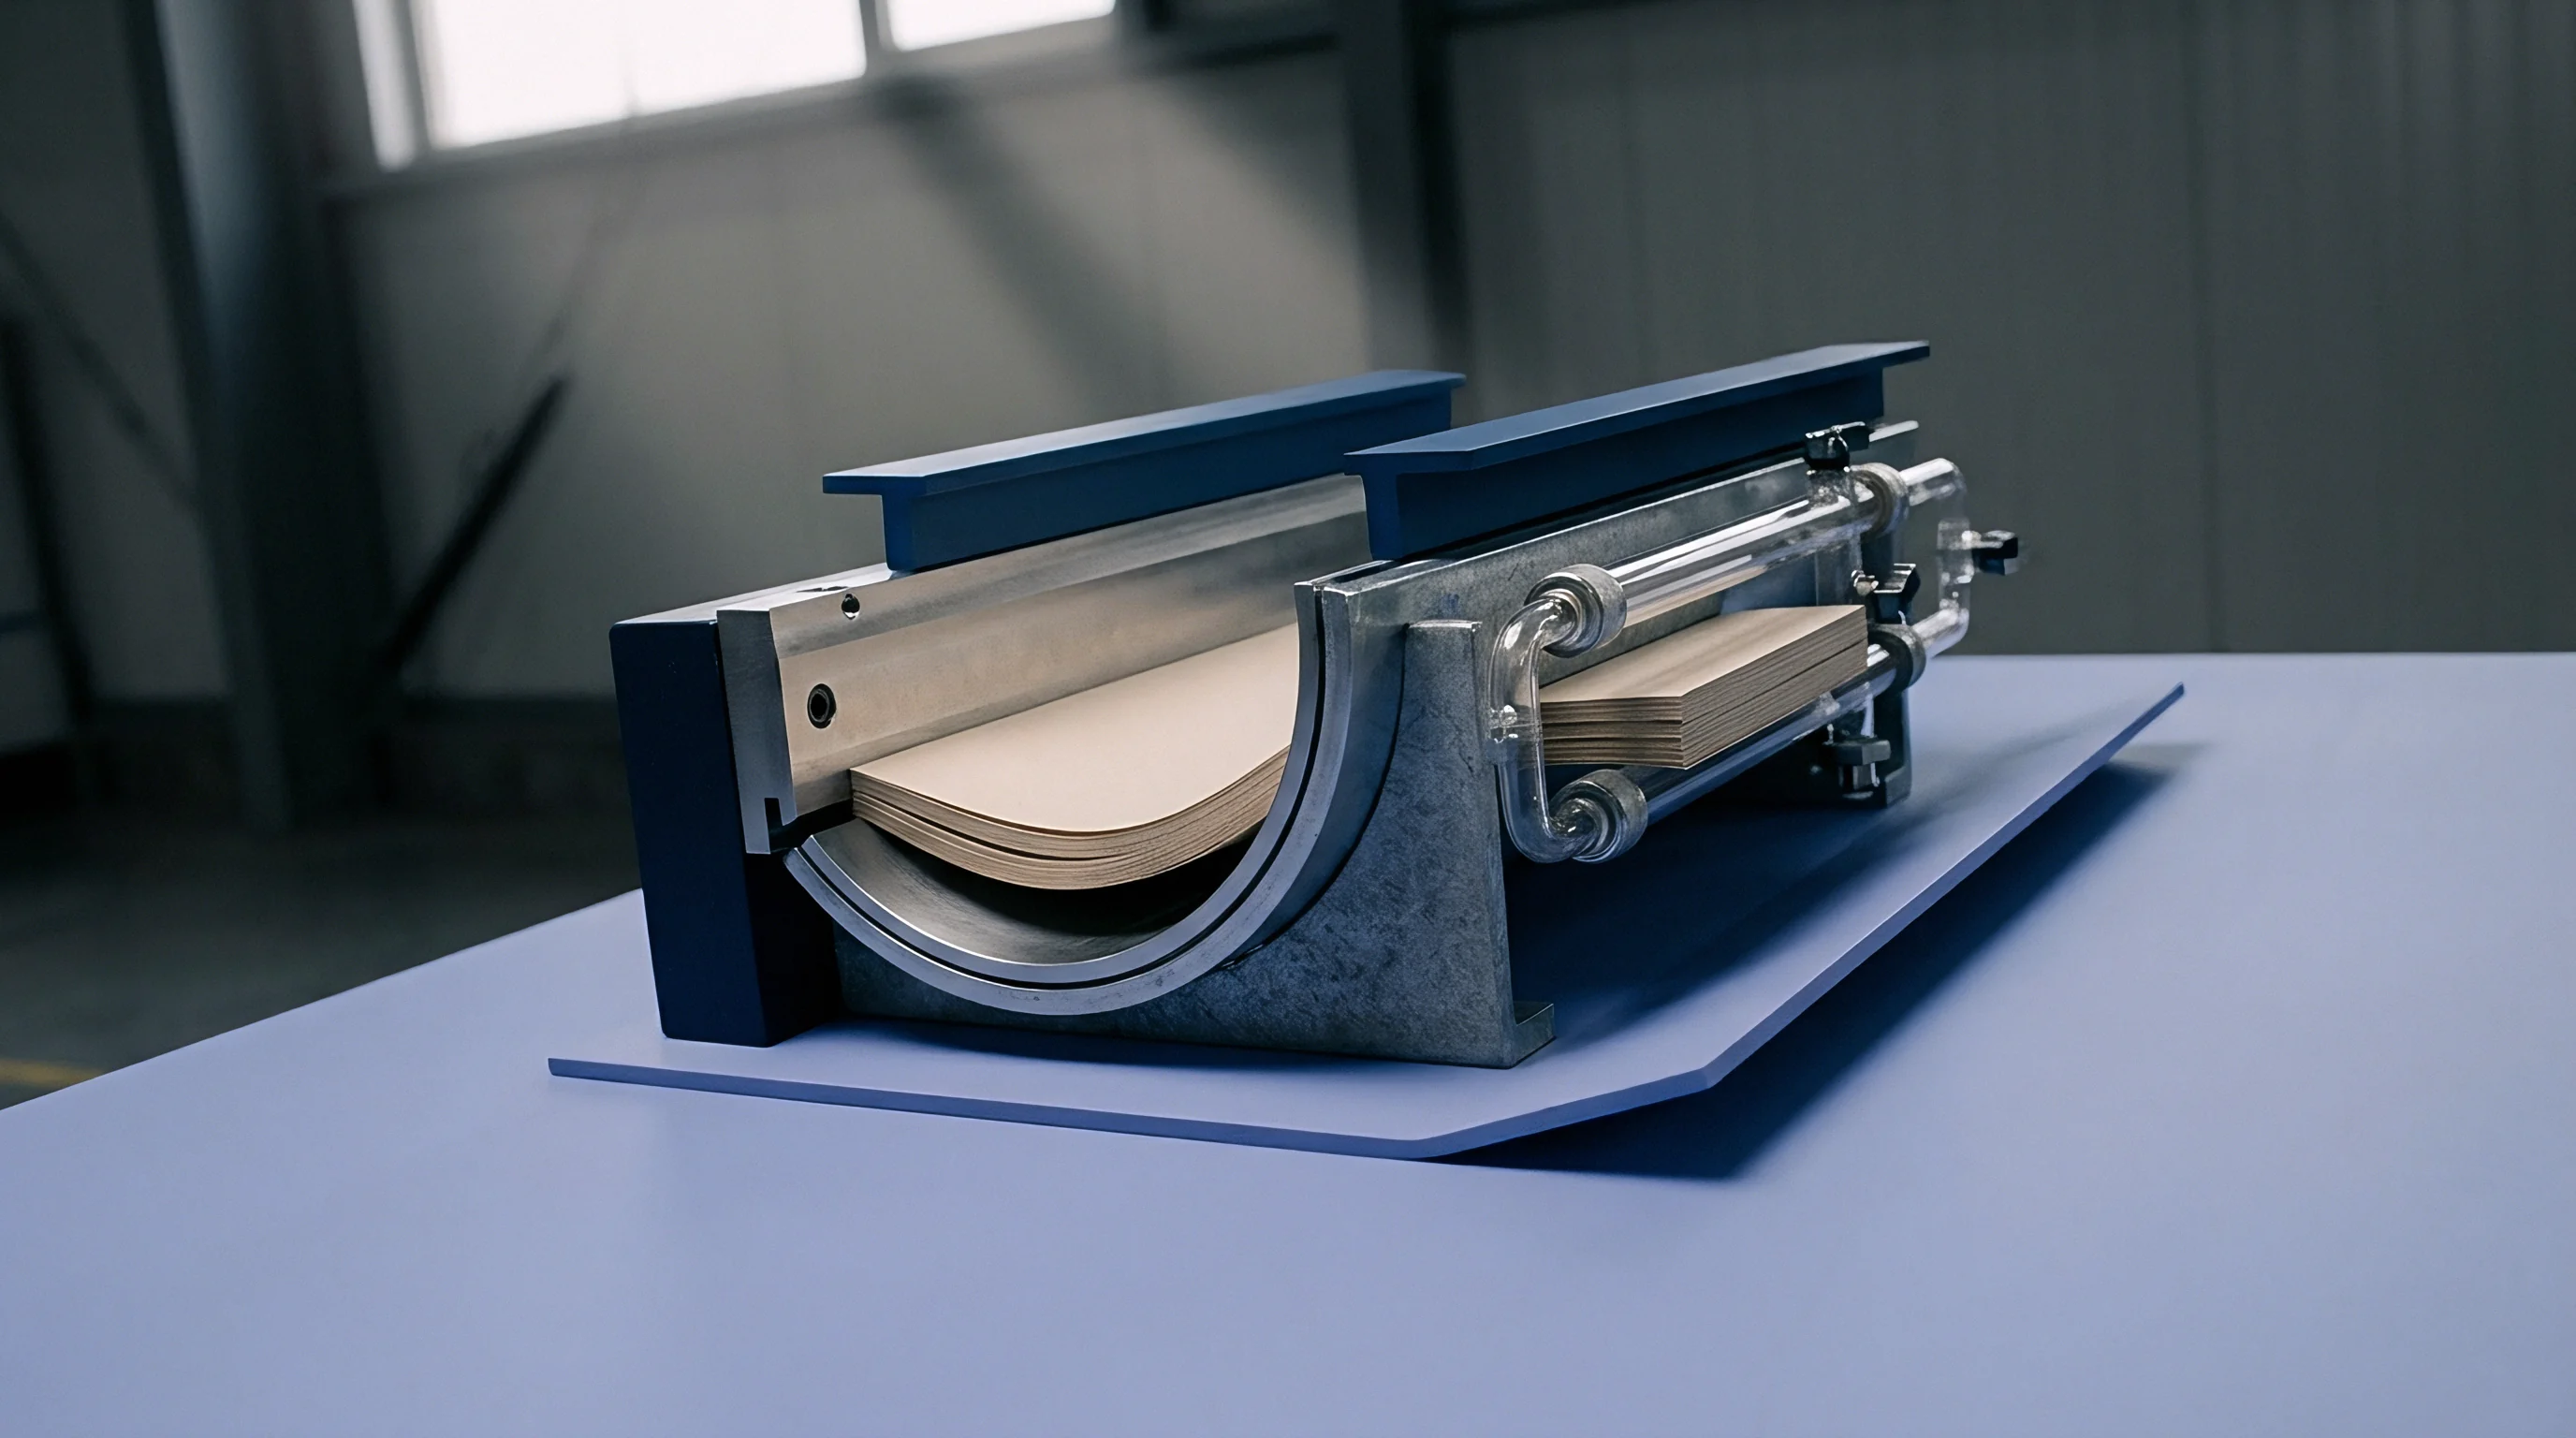
Standard cutting and creasing dies employ steel creasing rules with radiused profiles. The most common geometry is the round edge rule, which carries a continuous half-round profile across its working tip. While round rules perform reliably on long-fibred virgin substrates, their deep profile acts as a wedge against short-fibred recycled sheets.
The wedge drives concentrated tensile stress into the outer liner before the core plies break down into shear planes, splitting ink films along the fold edge.
Flat creasing rules incorporate a flat contact surface bounded by micro-radiused shoulders. Distributing the die platen impression across a flat face increases vertical compression while moderating lateral tension on the exterior linerboard. The flat profile compresses a wider strip of the middle ply, generating a broader delamination pocket that accommodates the bulky recycled furnish when folded 90 or 180 degrees.
Converters migrating from bleached chemical pulp to white lined chipboard routinely switch machine-direction scores from round rules to flat configurations to prevent face cracking.
Specialty geometries address specific furnish limitations across coated recycled boards:
- Flat face rules distribute the primary platen tonnage across a broad plane to prevent localized surface piercing on brittle clay coatings.
- Double creasing rules install two thin rules spaced slightly apart to generate a stepped dual-hinge profile for rigid, heavy-caliper recycled boards.
- Trapezoidal rules narrow slightly toward the tip to reduce flank friction during matrix entry while forcing maximum out-of-plane delamination.
- Laser creasing profiles apply micro-machined texturing to the rule tip, gripping the sheet surface to stop slip during fast platen cycles.
Shoulder Relief and Matrix Wear
The transition angle from the working tip of the rule to its vertical body dictates how cleanly the tool clears the matrix opening during ejection. Rules lacking shoulder relief scrape the inner matrix edges when platen balance drifts. Recycled boards carry abrasive minerals, including titanium dioxide and calcium carbonate, that dull cutting knives and polish rule profiles within fifty thousand impressions.
As rules wear smooth and flat, effective penetration decreases, demanding increased press tonnage that eventually crushes the flute or sheet structure.
Plate wear accelerates dramatically when running recycled furnishes at production speeds exceeding 7,000 sheets per hour. The abrasive dust liberated from unwashed recycled middles settles into the matrix channels, changing the effective depth over a twelve-hour shift. Cleaning cycles and visual checks of rule profiles prevent gradual drift into splitting territory, preserving clean hinge structures across production runs.
Creasing tools operating on high-ash recycled board lose ten to fifteen percent of their edge height within one hundred thousand cycles due to inorganic filler abrasion.
A converter cannot run virgin rule profiles on recycled chipboard without paying for the choice in broken carton flaps.

Hinge

Delamination Mechanics during Penetration
The formation of an acceptable crease hinges on inducing controlled internal shear within the paperboard sheet. When the creasing rule drives the sheet into the matrix channel, the material undergoes intense localized three-point bending combined with through-thickness compression. For a clean fold to occur without exterior cracking, the internal layers must shear apart horizontally, forming multiple thin, flexible delamination lamellae.
These internal delaminations relieve tension on the outer surface when the panel folds around the crease axis.
Recycled paperboard grades possess low internal bond strength, typically measured between 100 and 175 Joules per square metre via the Scott Bond test method TAPPI T 569. High-performance virgin boards register values exceeding 250 to 350 Joules per square metre. While low internal bond strength sounds beneficial for easy ply separation, recycled middles frequently crumble into discontinuous fractures rather than clean horizontal shear planes.
The lack of long fibre reinforcement causes the internal plies to collapse into localized voids, creating an erratic hinge line with variable folding resistance.
Scoreline bend resistance, evaluated according to ISO 2493-1 or TAPPI T 577, quantifies the force necessary to bend a creased carton flap through a 90-degree angle. Virgin boards display predictable folding resistance curves where the bending force drops sharply once internal delamination takes place. Recycled boards display erratic curves: insufficient matrix clearance leaves the middle plies uncompressed, leading to excessively high bending resistance that trips high-speed packaging machinery during carton erection.
| Substrate Classification | Pulp Composition | Scott Internal Bond (Joules per square metre) | Tensile Energy Absorption (Joules per square metre) | Recommended Crease Width Ratio |
|---|---|---|---|---|
| Solid Bleached Sulphate (SBS) | 100% Virgin Chemical | 280 to 380 | 180 to 240 | Rule + 1.50 x Caliper |
| Folding Boxboard (FBB) | Virgin Chemical and Mechanical | 180 to 260 | 130 to 180 | Rule + 1.60 x Caliper |
| Coated Recycled Board (CRB) | 100% Recycled Fibres | 110 to 170 | 80 to 120 | Rule + 1.80 x Caliper |
| White Lined Chipboard (WLC) | Recycled News and Mixed Waste | 95 to 150 | 70 to 110 | Rule + 1.85 x Caliper |
Should Tooling Geometry Compensate for Low Bond Strength?
Packaging buyers ask die-makers whether widening the channel is sufficient to manage low-grade recycled boards. Tooling adjustments manage surface crack initiation, but they cannot replace missing tensile strength across the backliner. If the unprinted reverse liner contains unsorted mixed waste with high lignin content, stretching that liner around a 90-degree corner tears the surface regardless of the matrix profile.
The die-maker balances rule width, penetration depth, and ejector rubber hardness to preserve the integrity of both outer plies.
Ejection rubber placement controls how the sheet releases from the cutting die and prevents premature tension tearing. High-density microcellular urethane rubbers placed close to the creasing rules hold the board flat against the counter plate during tool entry. If the rubber is too soft or positioned too far from the rule, the sheet pulls upward prematurely, generating irregular tensile spikes that tear the partially formed hinge bead.
Rigid recycled boards require stiff rubbers (around 50 to 60 Shore A hardness) placed within 1.5 millimetres of the crease rule to prevent delamination pull-out.
Packaging line reject rates remain directly coupled to the consistency of this internal shear delamination profile.
Moisture
Equilibrium Moisture and Creasability Windows
Paperboard is a hygroscopic material whose mechanical response changes across ambient relative humidity gradients. Recycled fibres, having undergone drying cycles during previous lifecycles, exhibit reduced hornified pores and diminished total moisture absorption capacity compared to virgin cellulose. Under standard converting conditions (23 degrees Celsius and 50 percent relative humidity per ISO 187), recycled cartonboard balances at an equilibrium moisture content between 6.0 and 7.5 percent by weight.
If ambient plant humidity falls below 40 percent, moisture drops below 5.5 percent, narrowing the converting window.
Dry recycled fibres become brittle, elevating stiffness while reducing tensile elongation at break. When a creasing rule impacts a desiccated recycled sheet, the outer liner cracks before shear delamination spreads through the core. If relative humidity climbs above 65 percent, equilibrium moisture surpasses 8.5 percent.
Under high moisture, the internal plies turn spongy, absorbing platen energy through plastic deformation rather than crisp delamination, yielding weak creases that offer poor line stability on automated carton erectors.
The relationship between equilibrium moisture, rule width, and cracking severity appears across production logs:
- Below five percent moisture triggers immediate linerboard rupture along cross-direction scores unless channel widths expand by 0.20 millimetres beyond standard formulas.
- Between six and seven percent moisture provides the ideal window where internal delamination occurs with minimal surface stress under standard matrix calculations.
- Above eight percent moisture reduces carton compression resistance (BCT) by up to 25 percent and causes wide, mushy creases that fail to track straight.
- Moisture gradients through the stack cause outer sheets on an unconditioned pallet to split while core sheets run cleanly through identical tooling.
Drop the equilibrium moisture of a coated recycled sheet below 5.5 percent and the cross-direction creasing window contracts to zero.
A winter shipment stored in an unheated staging warehouse arrives at the press cold and dry. Running that stock immediately without 48 hours of thermal and moisture acclimation causes widespread carton failure across the die-cutter. The press operator often blames the steel counter plate or increases cutting tonnage, when the actual failure mode traces directly to substrate equilibrium dynamics.
The standard supply agreement clause specifying delivery at six to eight percent moisture means little when pallets sit unwrapped on damp loading bays or dry pressroom floors.
Yield
Landed Costs and Machine Line Spoilage
Carton procurement decisions frequently treat recycled board grades as an immediate route to material cost reduction. White lined chipboard or coated recycled board typically trades at a discount of 15 to 25 percent per metric tonne compared to virgin solid bleached sulphate or folding boxboard. A packaging buyer calculating unit economics on raw tonnage price alone overlooks the commercial penalties introduced by reduced yield, lower machine speeds, and converting spoilage.
The physical limitations of recycled furnish extract financial returns across every processing phase.
Recycled board carries a higher bulk density than virgin mechanical grades like folding boxboard. Achieving the required package rigidity on recycled stock demands an increase in board caliper or basis weight, eroding the initial price-per-tonne advantage through lower sheet yield per delivered tonne. A job running on 350-gram virgin folding boxboard might require a 400-gram white lined chipboard to match panel stiffness.
That basis-weight increase eliminates approximately twelve percent of the raw sheet count per purchased tonne before considering converting spoilage.
Pressroom production speeds drop when running recycled grades through complex cutting dies. Die-cutters running virgin board at 8,500 sheets per hour often decelerate to 6,000 or 6,500 sheets per hour when handling recycled boards to prevent dynamic sheet bounce and score cracking. Slower cycle times elevate machine-hour allocations.
Spoilage rates on gluing lines and automated end-of-line packaging machines climb when erratic scorelines produce cartons with variable folding resistance or misaligned flaps.
| Cost Component | Solid Bleached Sulphate (350 micrometres) | Coated Recycled Board (400 micrometres) | Variance Impact |
|---|---|---|---|
| Basis Weight (grams per square metre) | 280 | 335 | +19.6% Tonnage Requirement |
| Substrate Price (per metric tonne) | $1,450 | $1,180 | -18.6% Nominal Tonnage Price |
| Substrate Cost per 1,000 Blanks | $142.10 | $138.25 | $3.85 Savings per 1,000 Blanks |
| Die-Cutting Make-Ready Waste (Sheets) | 350 | 850 | Additional Material Loss |
| Die-Cutter Run Speed (Sheets per Hour) | 8,000 | 6,200 | +29% Extended Press Time |
| Gluer and Packaging Line Spoilage | 0.4% | 2.1% | 1,700 Additional Defective Cartons |
| Net Landed Cost per 1,000 Units | $198.40 | $209.70 | +$11.30 Net Penalty for Recycled |
Die-cutting tooling expenditures increase when running abrasive recycled stocks. Steel counter plates wear out faster, rules require frequent re-knifing, and matrix channels choke with dust, necessitating shorter intervals between tool replacements. A procurement desk that captures an apparent four-dollar saving per thousand blanks on material costs frequently absorbs an eleven-dollar net penalty per thousand delivered cartons once converting downtime, spoilage, and tooling maintenance hit the ledger.
The buyer decides whether the brand owner’s recycled-content claim justifies carrying slower converting speeds and narrow processing windows onto the packaging line.
Dossier
Procurement Specifications for Recycled Stock Creasability
Specifying recycled cartonboard requires strict performance-based parameters rather than simple weight and caliper targets. A procurement specification protecting against scoring defects establishes defined mechanical thresholds for ply bond, moisture ranges, and surface elongation before orders are confirmed. Without explicit boundaries covering these variables, converters bear the entire economic liability when brittle recycled fibres fail on high-speed gluer folders.
A rigorous mill order specification contains explicit test criteria:
- Caliper variation held within plus or minus four percent across the parent reel width according to ISO 534 protocols.
- Absolute moisture delivery verified within 6.0 to 7.5 percent based on ISO 287 oven drying methods upon arrival.
- Scott internal bond strength maintaining a floor of 120 Joules per square metre per TAPPI T 569 to secure interlaminar shear.
- Minimum Cross Direction Tensile Energy Absorption exceeding 85 Joules per square metre via ISO 1924-2 to eliminate score-line bursting.
- Maximum ash content capped below 16 percent under ISO 1762 testing to mitigate premature tooling abrasion and core crumbling.
Incoming inspection procedures at the converting plant should test moisture and caliper before unwrapping pallets for the die-cutting floor. Handheld moisture meters provide fast preliminary data, while benchtop micrometer surveys identify localized sheet thickness variations that exceed matrix clearance allowances. If an incoming shipment exhibits low moisture coupled with high caliper, the die shop receives immediate instruction to widen the female creasing matrix by 0.10 to 0.20 millimetres before tooling strikes the sheet.
A complete technical dossier links furnish metrics directly to tool design. The converter documents every combination of board grade, measured caliper, selected rule geometry, and matrix dimensions on a job card. This recorded history eliminates guesswork when running the same board on repeat packaging contracts.
Clear definitions across the supply chain ensure that recycled board runs smoothly through automated lines, delivering sustainable packaging that meets functional requirements without inflating manufacturing scrap.
The question of how far ash fractions can climb before no tool geometry can prevent score bursting remains an open dispute between recycled mills and carton converters.