Structural Mechanics
High speed converting lines transform flat printed blanks into three dimensional packaging through dedicated folding and gluing stations that apply precise adhesive patterns under regulated pressure. Mechanical accuracy during these operations determines whether a carton passes automated filling line tolerances without jamming or failing at the manufacturer joint. Modern carton plants deploy a folder gluer to execute continuous creasing, prebreaking, side gluing, and final compression stages at speeds exceeding four hundred meters per minute.
Feeders separate individual blanks from the stack using vacuum belts, transferring each substrate into alignment modules that square the trailing edges before folding commences. Plow folders and helical folding belts then rotate panel scores up to one hundred eighty degrees, bringing the final glue flap into direct contact with the opposing edge. Electronic cold glue application systems or hot melt nozzles dispense microdots or continuous beads along the precise path defined by the packaging design.
Compression sections immediately following the glue application apply uniform dwell pressure across the joint to guarantee fiber tear upon subsequent destructive testing.
Adhesive Dynamics
Bond formation relies on precise rheological properties within the selected emulsion or hot melt formulation, balancing open time against setting speed to match line velocity. Water based polyvinyl acetate dispersions penetrate porous clay coated paperboard surfaces rapidly, whereas synthetic polymers handle non porous UV varnishes or laminated foil stocks by establishing mechanical anchorage. Viscosity control systems monitor fluid temperature and pump pressure continuously, preventing nozzle clogging or starvation during long production runs.
Shear stress resistance dictates structural integrity once the carton cures, ensuring the manufacturer joint withstands outward springback forces exerted by heavy weight solid bleached sulfate boards or corrugated microflutes. Operators adjust bead width and compression dwell time according to the grammage of the substrate, preventing adhesive squeeze out that fouls downstream conveyor belts or ruins adjacent printed panels.
Dimensional Tolerances
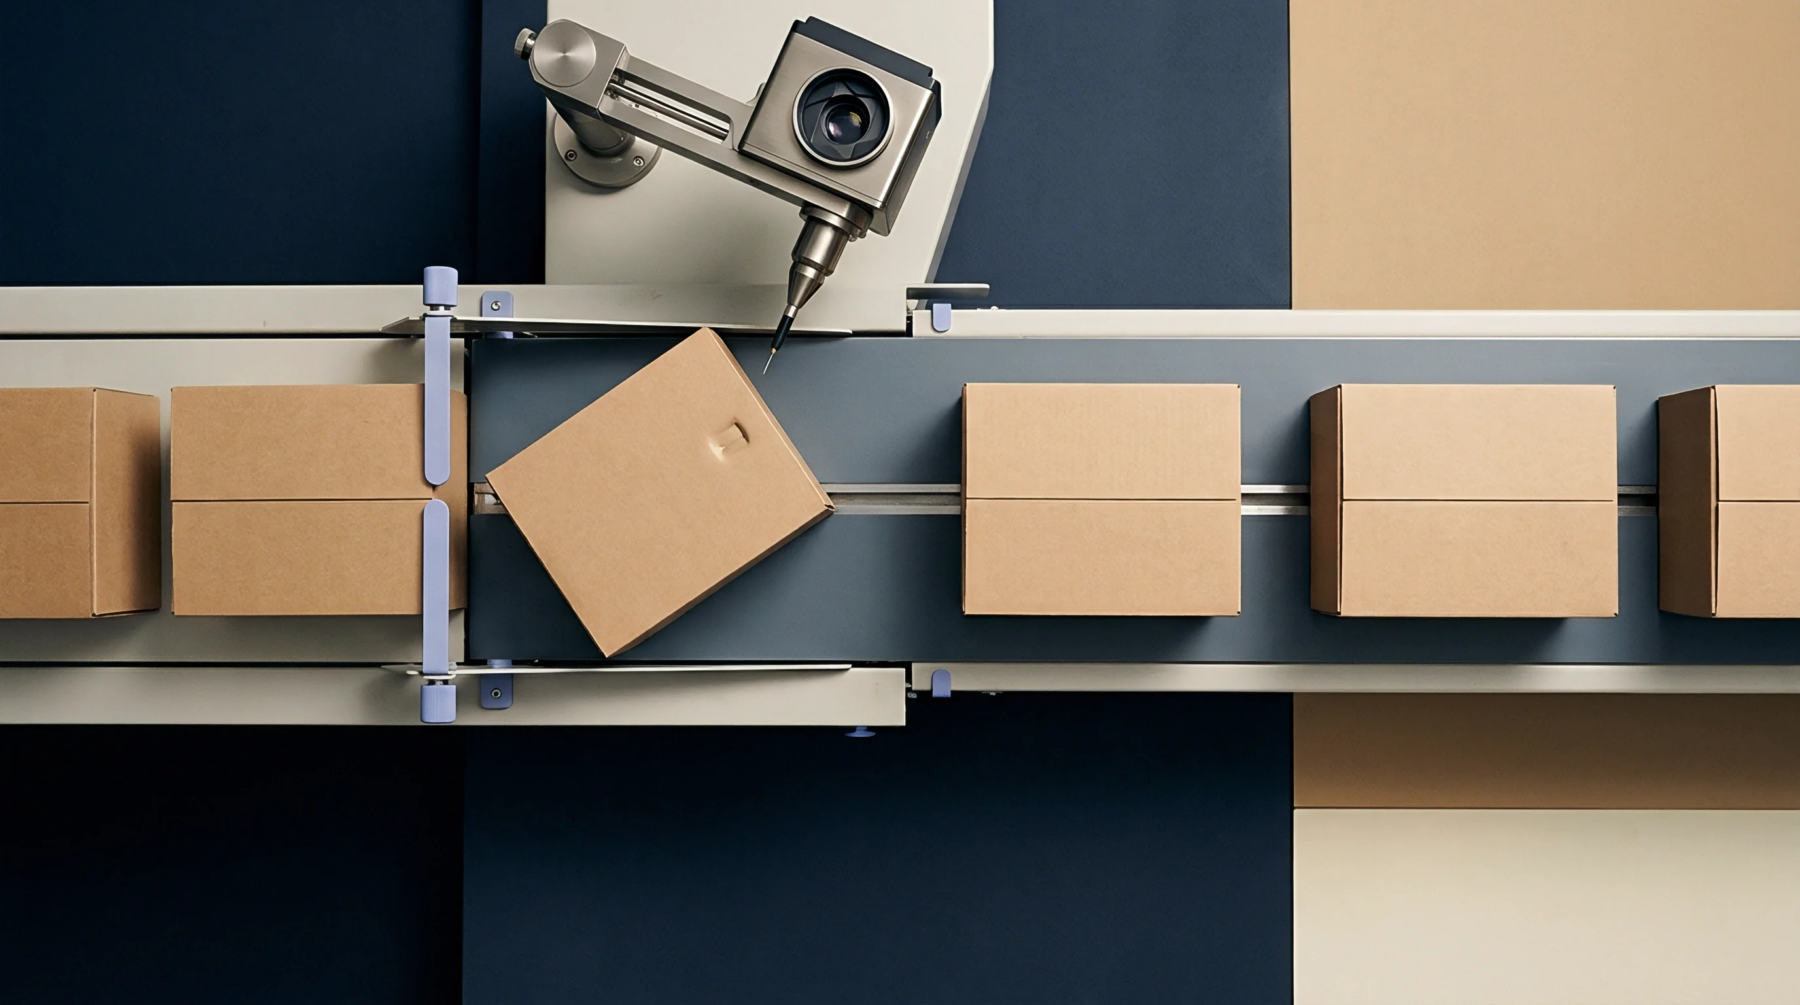
Quality assurance protocols verify squareness and glue placement accuracy by pulling random samples from the delivery apron at regular intervals during production shifts. Skewed blanks or misaligned glue lines alter the final geometry of the erected carton, causing jams inside high speed pharmaceutical or food packaging machinery. Optical inspection systems mounted on the delivery end detect missing adhesive beads or out of spec dimensions instantly, ejecting defective units before packaging into master shipping cases occurs.
Register control adjustments allow operators to shift entire folding cassettes by fractions of a millimeter while the machine runs at full capacity, maintaining strict alignment across millions of printed folding cartons. Mechanical wear on drive belts or folding hooks introduces subtle variations over time, requiring routine calibration against baseline master samples to preserve container performance standards.