Folding Boxboard Calendering Gradient Dynamics and Mechanical Bulk Preservation
Temperature gradient calendering preserves FBB mechanical bulk by softening surface fibres while keeping core BCTMP below glass transition to protect stiffness.
Temperature gradient calendering preserves FBB mechanical bulk by softening surface fibres while keeping core BCTMP below glass transition to protect stiffness.
Water sorption depresses latex film glass transition temperatures, slashing barrier composite stiffness by up to 45% and requiring controlled crosslinking.
Nesting carton blanks across web deckles saves converting trim but rotates crease lines against machine grain, escalating carton erection failures at speed.
Aligning paperboard machine direction perpendicular to the pull axis maintains panel flatness under suction, preventing extraction jams at high machine speeds.
BCTMP cores lower basis weight for target stiffness, but elevated humidity plasticizes lignin, accelerating score memory loss and risking carton wall bulge.
Maintain crease depth ratios between 0.55 and 0.65 to induce internal ply shear, reducing panel springback torque for clean high-speed package ejection.
Optical penetration depth correction in continuous board web profilometry mathematically compensates for subsurface scattering to ensure true mechanical caliper.
Retain board bulk and bending stiffness by applying surface moisture gradients to lower outer ply glass transition temperatures before soft nip compression.
Inline ultrasonic testing verifies internal score delamination and folding resistance in real time, preventing visual surface cracking and high-speed erect jams.
Predictive stiffness loss modeling prevents folder-gluer waste by adjusting crease depth and binder chemistry to compensate for high-speed dynamic strain.
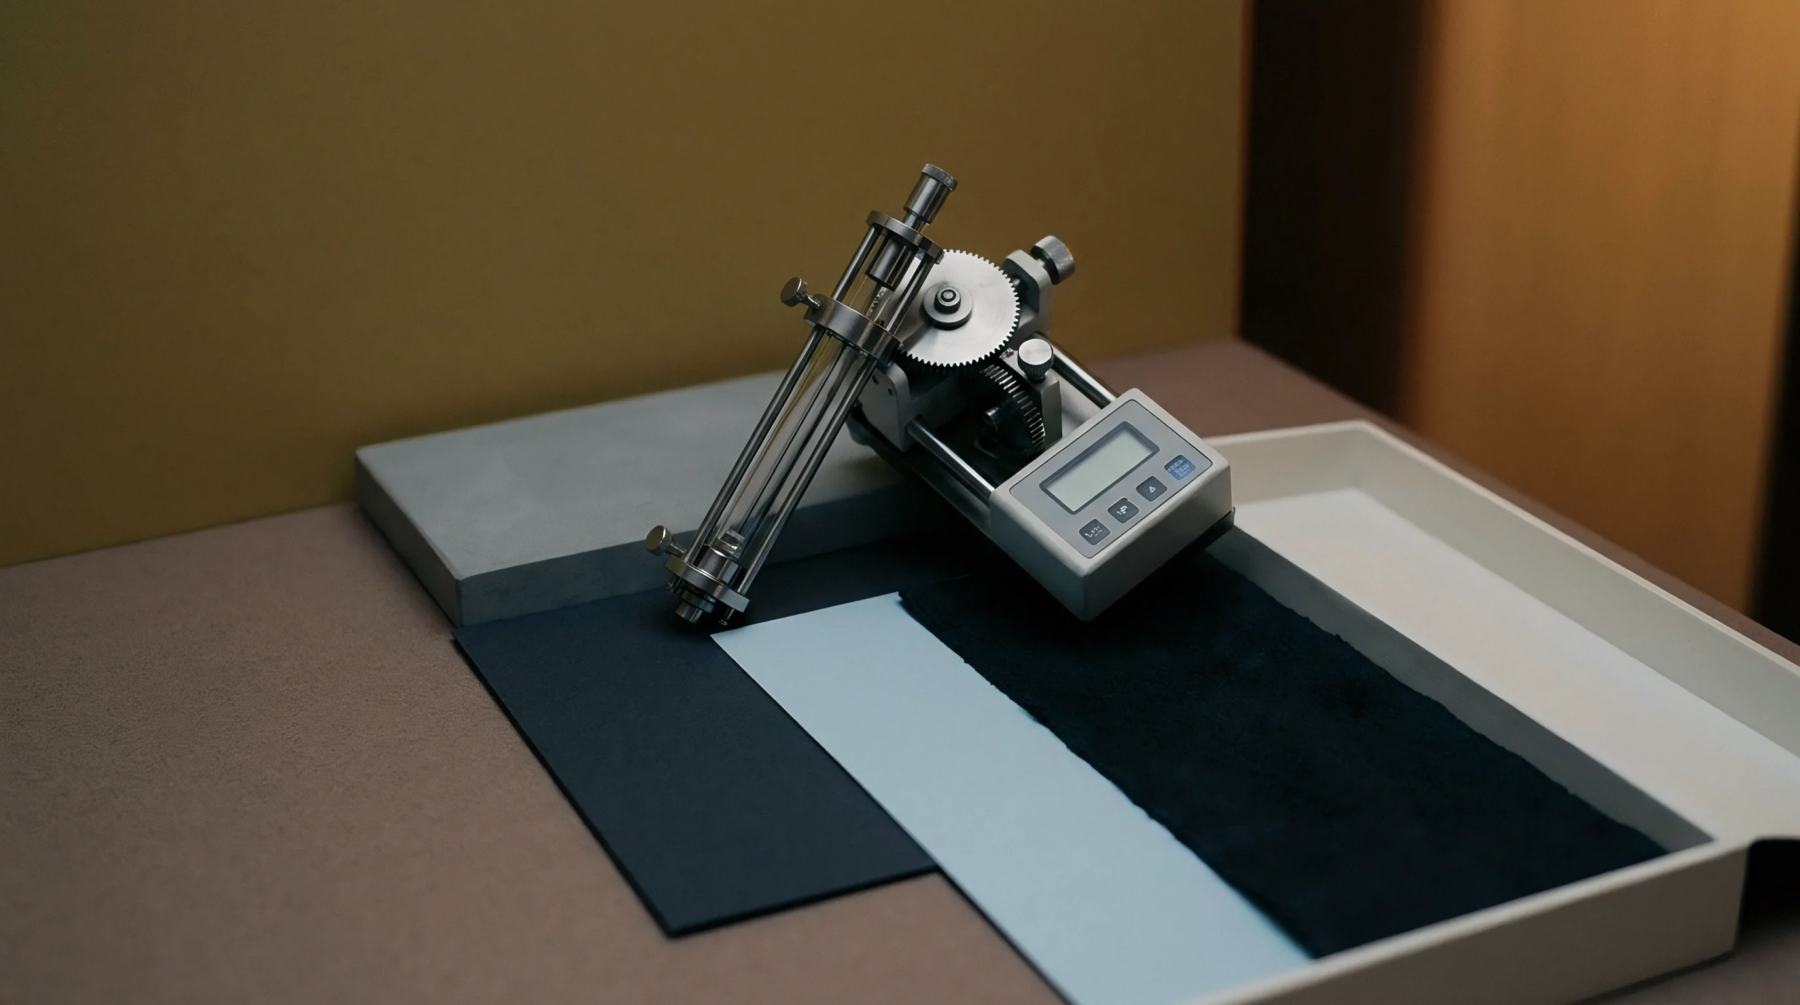
Calculate matrix channel width for co-extruded laminates using an expanded 1.65 to 1.85 board modifier plus rule gauge and double film thickness.
Predicting interfacial delamination thresholds in recycled boxboard requires quantifying Mode II shear fracture toughness and adjusting crease matrix channel dimensions to prevent hinge failure under cyclic loading.
Dynamic pass line vibration cancellation restores laser caliper gauge resolution down to sub-micron accuracy by eliminating phase-lag z-axis position errors.
Valid boxboard physical testing requires ISO 187 conditioning at 23°C and 50% RH to prevent hysteresis errors in stiffness, yield, and creasing metrics.
Jet-to-wire velocity ratios govern machine-direction fiber orientation, setting board anisotropy ratios that dictate box compression and score crack resistance.
High erection speeds induce inter-ply shear strain that causes carton delamination when Z-direction bond strength drops below 180 Joules per square metre.
Folding boxboard machine direction stiffness anisotropy governs carton opening force and high-speed feeder reliability, demanding strict ratio limits on orders.
Core bulk retention during shoe press dewatering requires asymmetric pressure profiles and controlled temperature to prevent mechanical pulp lumen collapse.
Optimizing multi-ply boxboard caliper requires balancing mechanical core thickness against chemical skin elastic modulus to maximize bending stiffness per unit weight.
Rapid shear creasing requires tailored interply delamination toughness to prevent liner fracturing while reducing folding torque on high-speed lines.
Paperboard flexural rigidity depends on the cube of caliper, requiring exact ISO 2493 or TAPPI T 489 instrument alignment and strict 23°C/50% RH conditioning.
Calibrated matrix channel width relies on board caliper, rule thickness, and fiber shear mechanics to prevent liner cracking and gluer jams.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.