High Speed Paperboard Creasing Kinematics and Tooling
Precision matching of creasing rule thickness and counter channel width prevents outer liner cracking and stabilizes folding force on high speed lines.
Precision matching of creasing rule thickness and counter channel width prevents outer liner cracking and stabilizes folding force on high speed lines.
Controlled inter-ply delamination during scoring reduces initial flexural stiffness by 50 percent, preventing outer liner cracking on high-speed lines.
Converting multi-ply secondary furnish board requires expanding matrix channel width by 10 to 12 percent beyond standard virgin formulas to accommodate lower Z-tensile strength and prevent liner cracking.
Online optical triangulation measures paper web thickness non-contact via opposing laser displacement sensors, requiring blue wavelength lasers to suppress fibre scattering.
Cross direction scoreline shear requires precise matrix clearance to split internal plies into sliding lamellae without exceeding outer liner tensile limits.
Controlling shoe press pressure profiles reduces peak nip stress while extending dwell time, preserving middle ply volume to maximize board stiffness and yield.
Structuring multi-ply recycled linerboard into density-optimized layers increases flexural rigidity and prevents score cracking while optimizing yield.
Boxboard claims require exact invoice codes, LC-GC-FID MOSH/MOAH testing under EN 16995, and ISO 2859-1 receiving audits to prevent customs holds.
Cross-direction elongation between 3.2% and 4.8% prevents outer liner cracking on folding boxboard when matrix channel width equals rule size plus 1.5 times caliper.
Zonal induction thermoroll heat combined with segmented spray moisture balances cross-web board caliper while preserving bulk and internal ply bond.
Dynamic creasing impact compresses internal pore air into transient pressure spikes, reducing effective shear strength and causing high-speed ply blowout.
Core bulk retention during shoe press dewatering requires asymmetric pressure profiles and controlled temperature to prevent mechanical pulp lumen collapse.
Low-fibre recycled board requires widening female matrix channels to 1.8 times caliper and reducing penetration depth to prevent top-liner rupture.
Statistical lot verification protects packaging buyers by tying standardized sample testing directly to batch acceptance quality limits and contract settlement terms.
Selective z-directional moisture and thermal calendering plasticizes outer chemical plies to optimize surface smoothness while preserving mechanical core bulk and stiffness.
Counter matrix channel width equals creasing rule thickness plus 1.5 to 1.7 times board caliper under ISO 534 conditioning to optimize delamination.
Selecting steel creasing rules and matrix channels for coated FBB requires matching board caliper and CTMP core shear limits to prevent surface cracking.
Ground paper supply pass-through clauses in verified dry fibre weight, strict index lag rules, and active goods-in batch audits to block supplier overcharges.
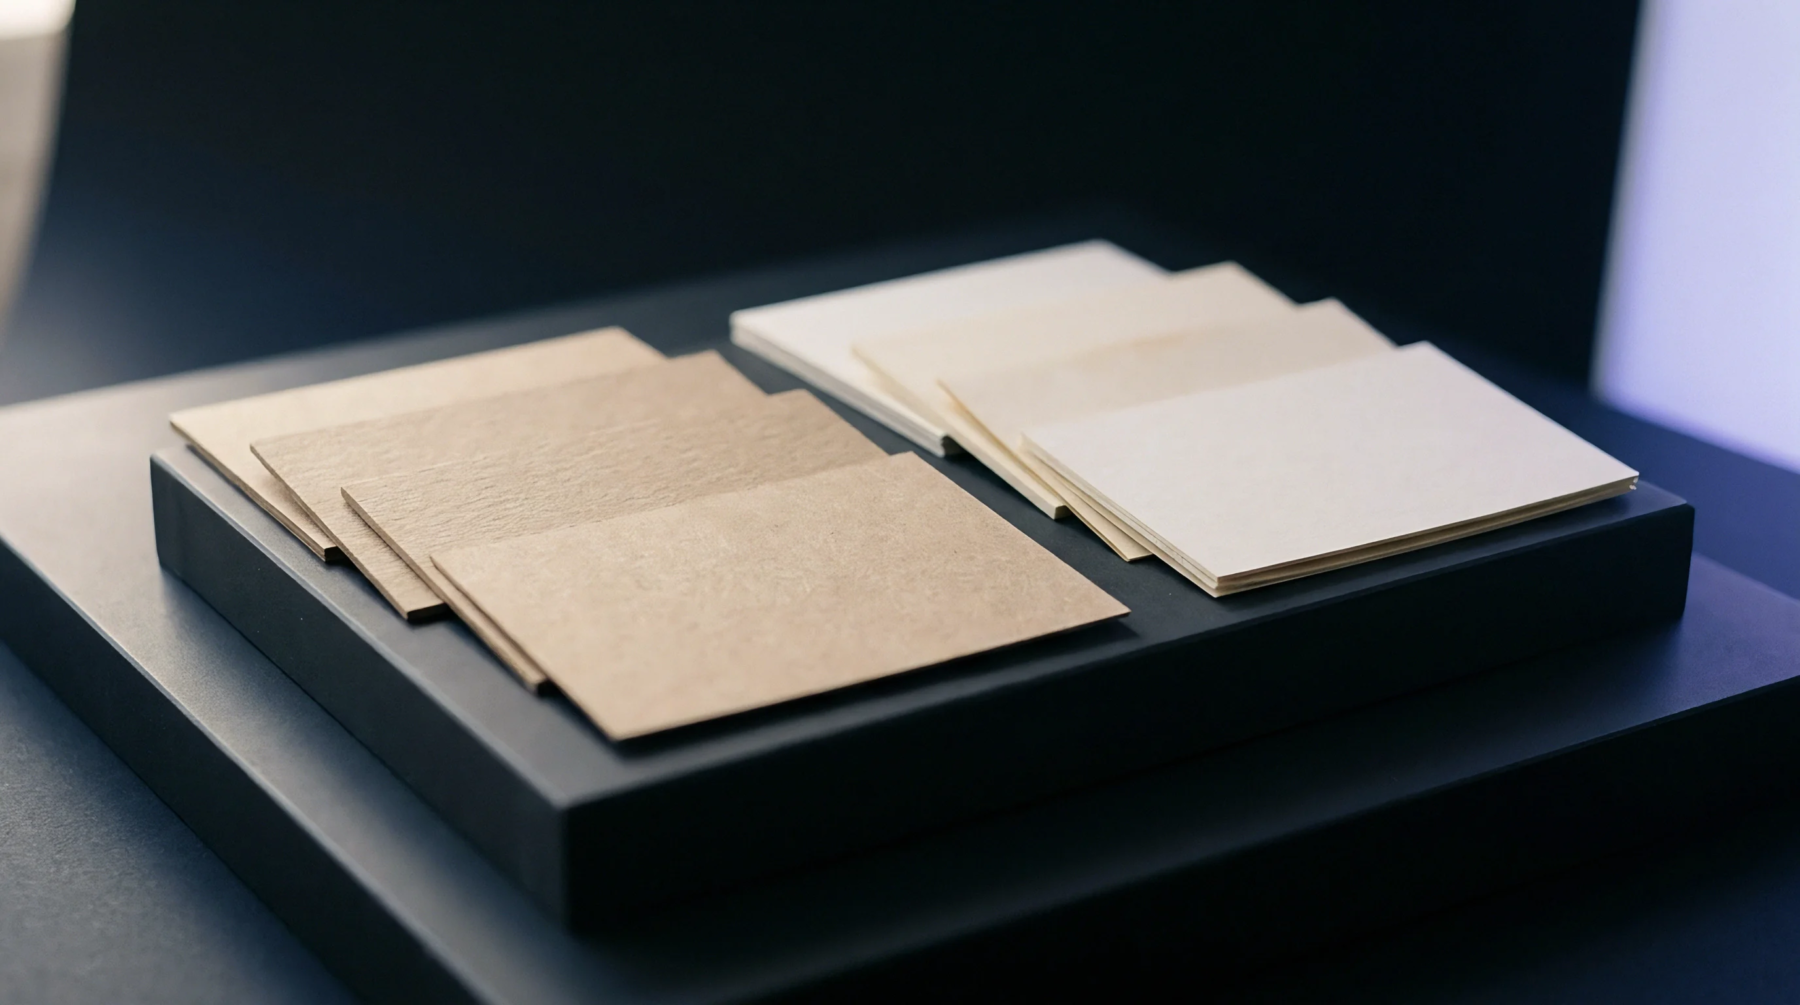
Virgin SBS provides superior print brightness, stiffness consistency, and crack-free scoring, whereas recycled board lowers initial cost but adds waste.
Committing embossing die funds before verifying batch-specific board caliper causes die clearance errors, crushed paperboard profiles, and ruined tooling.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.