Lead Time Each Added Pass Buys between Approval and Pallet
Each added pass adds 24 to 48 hours of lead time through mandatory inter-pass drying, thermal stabilization, tooling lead times, and offline queue staging.
Each added pass adds 24 to 48 hours of lead time through mandatory inter-pass drying, thermal stabilization, tooling lead times, and offline queue staging.
Fibre length degradation in recycled boxboard reduces sheet stiffness and score integrity, requiring chemical bonding additives or higher basis weight to preserve performance.
Optimize matrix channel clearance using board caliper and rule thickness formulas to guarantee internal ply delamination while preventing outer liner score cracking.
Fractionating recycled furnish prior to low-consistency refining preserves boxboard caliper while meeting internal bond targets at reduced energy consumption.
Optimizing multi-ply recycled containerboard requires strategic furnish distribution and precise starch application to maximize stiffness while lowering total fiber cost.
Hornification in secondary fibres reduces internal pore volume and alters optical scattering, requiring dynamic wetting controls to prevent press mottle.
Dynamic delamination thresholds in recycled calipers dictate converted score integrity, requiring minimum inter-ply shear energy dissipation under high strain rates.
Inter-ply bond standards mandate TAPPI T 541 or ISO 16260 testing under strict ISO 187 conditioning to prevent converting delamination on recycled paperboard.
Interfacial shear delamination in dispersion-coated folding boxboards occurs when converting flexure stresses exceed polymer-fiber bond fracture energy.
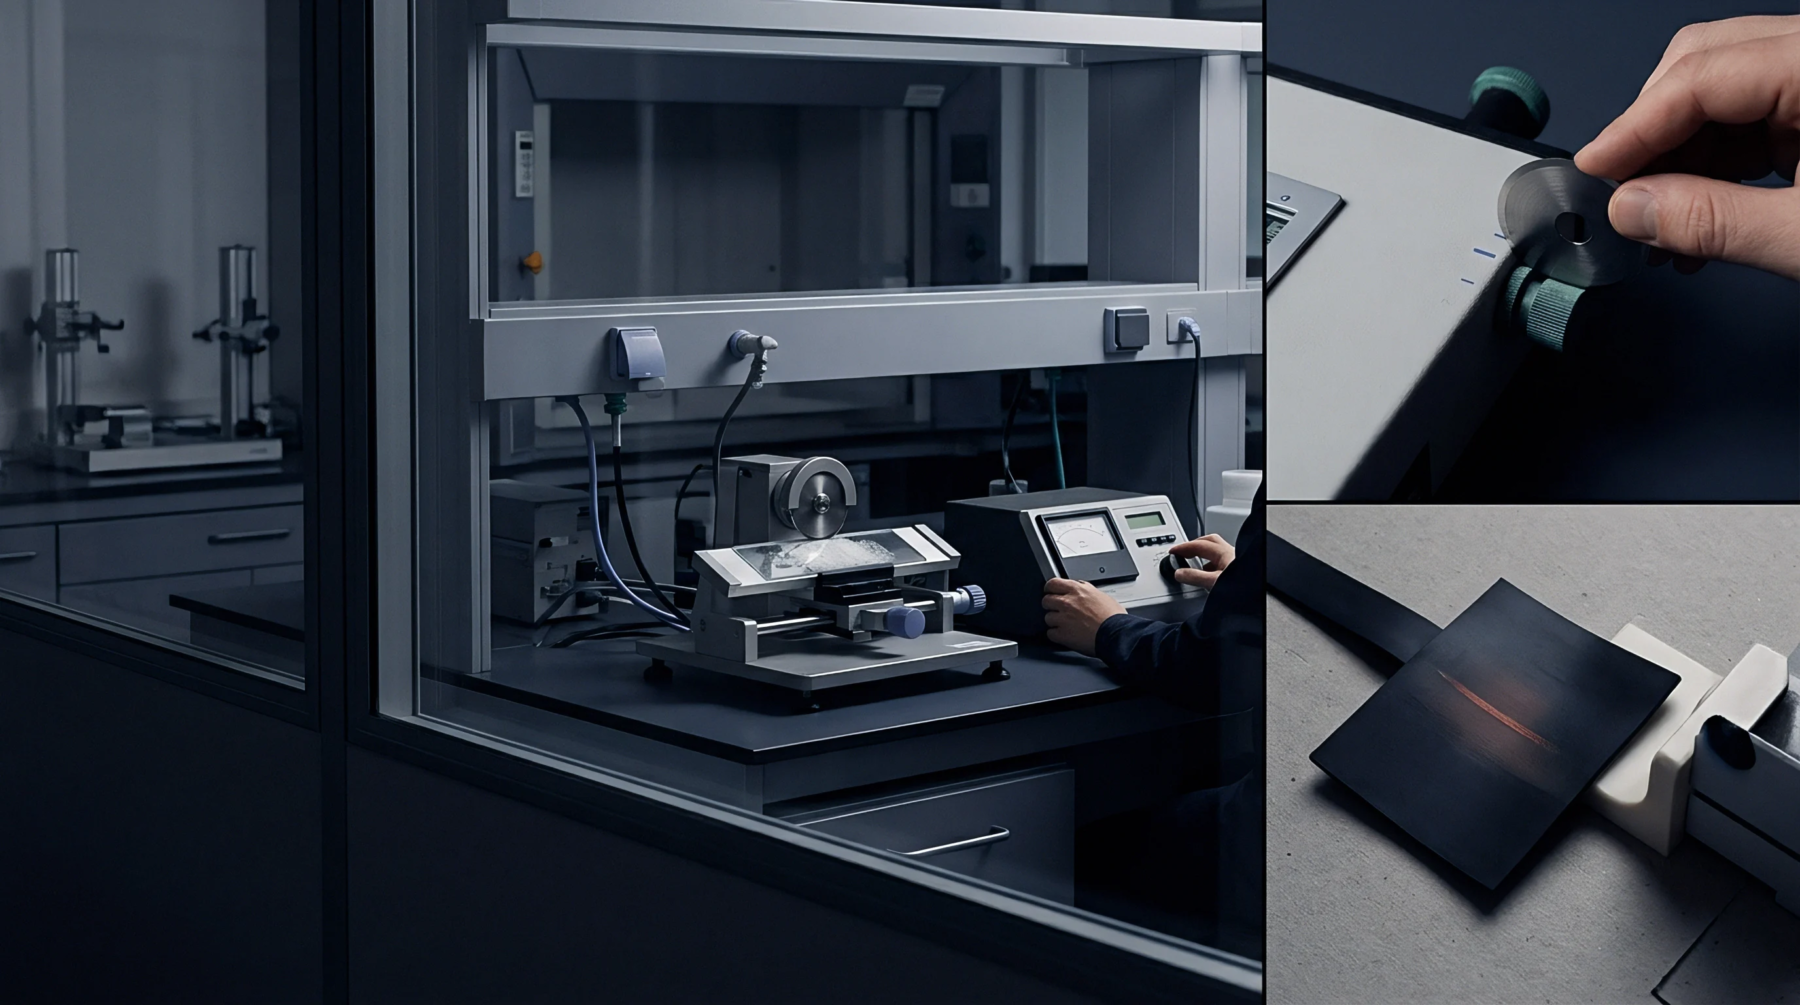
Paperboard physical property verification requires strict ISO 187 conditioning and standardized test methods to ensure compliance and prevent customs holds.
Matching dynamic Scott Bond energy above 120 J/m² prevents high-speed folder-gluer delamination and reduces net carton cost through lower line scrap.
Low-fibre recycled board requires widening female matrix channels to 1.8 times caliper and reducing penetration depth to prevent top-liner rupture.
Eucalyptus fiber collapse and hydrogen bond density dictate sheet tensile strength, bulk retention, and landed sheet cost in commercial packaging grades.
Controlled low energy refining of middle ply mechanical pulp yields superior Z direction tensile development without caliper loss in multi ply boxboard.
Predicting paperboard delamination requires balancing Z-direction shear strength to permit core separation while preventing outer liner tensile fracture.
Dynamic high-speed shear delamination across mechanical board cores occurs when strain rates exceed interfacial starch adhesion, requiring dynamic shear specification over static Scott bond values.
High erection speeds induce inter-ply shear strain that causes carton delamination when Z-direction bond strength drops below 180 Joules per square metre.
Dynamic Scott Bond impact and static Z-tensile testing verify multi-ply recycled board strength to prevent costly delamination during foil stamping and creasing.
Optimize counter-matrix width and rule penetration depth to induce internal core ply delamination while protecting outer extrusion barrier films from shearing.
Maintain crease depth ratios between 0.55 and 0.65 to induce internal ply shear, reducing panel springback torque for clean high-speed package ejection.
Shoe press peak hydraulic pressure must remain below wet web z-tensile limits to prevent core delamination in secondary fiber containerboard manufacturing.
Controlling vacuum hydrofoil pressure gradients and press impulse prevents internal delamination in multi-ply recycled linerboard during converter scoring.
Selecting paperboard caliper and bulk requires balancing furnish density against flexural rigidity to maximize blank yield and carton compression strength.
Low-tortuosity carbonate coatings and minimum 150 J/m² Scott bond prevent heatset web blistering by venting flash steam before internal core delamination occurs.
Zonal induction thermoroll heat combined with segmented spray moisture balances cross-web board caliper while preserving bulk and internal ply bond.
Dynamic high strain rate testing exposes inter-ply strength loss in recycled board that standard static Z-tensile tests miss, preventing carton converting failure.
Dynamic mechanical recovery thresholds set the limit where cyclic shear causes permanent ply delamination, dropping box stacking strength in transit.
Recycled containerboard loses stiffness when hornified fibers slip under shear, which buyers offset with higher grammage or starch addition.
Mechano-sorptive cycling accelerates transverse delamination in recycled multi-ply board, collapsing stacked cartons when interlaminar shear exceeds ZD tensile bond.
Verify Scott Bond above 120 J/m² and ZDT above 220 kPa under ISO 187 conditioning to prevent blanket delamination and score splitting on recycled cartonboard.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.